Foam Extrusion
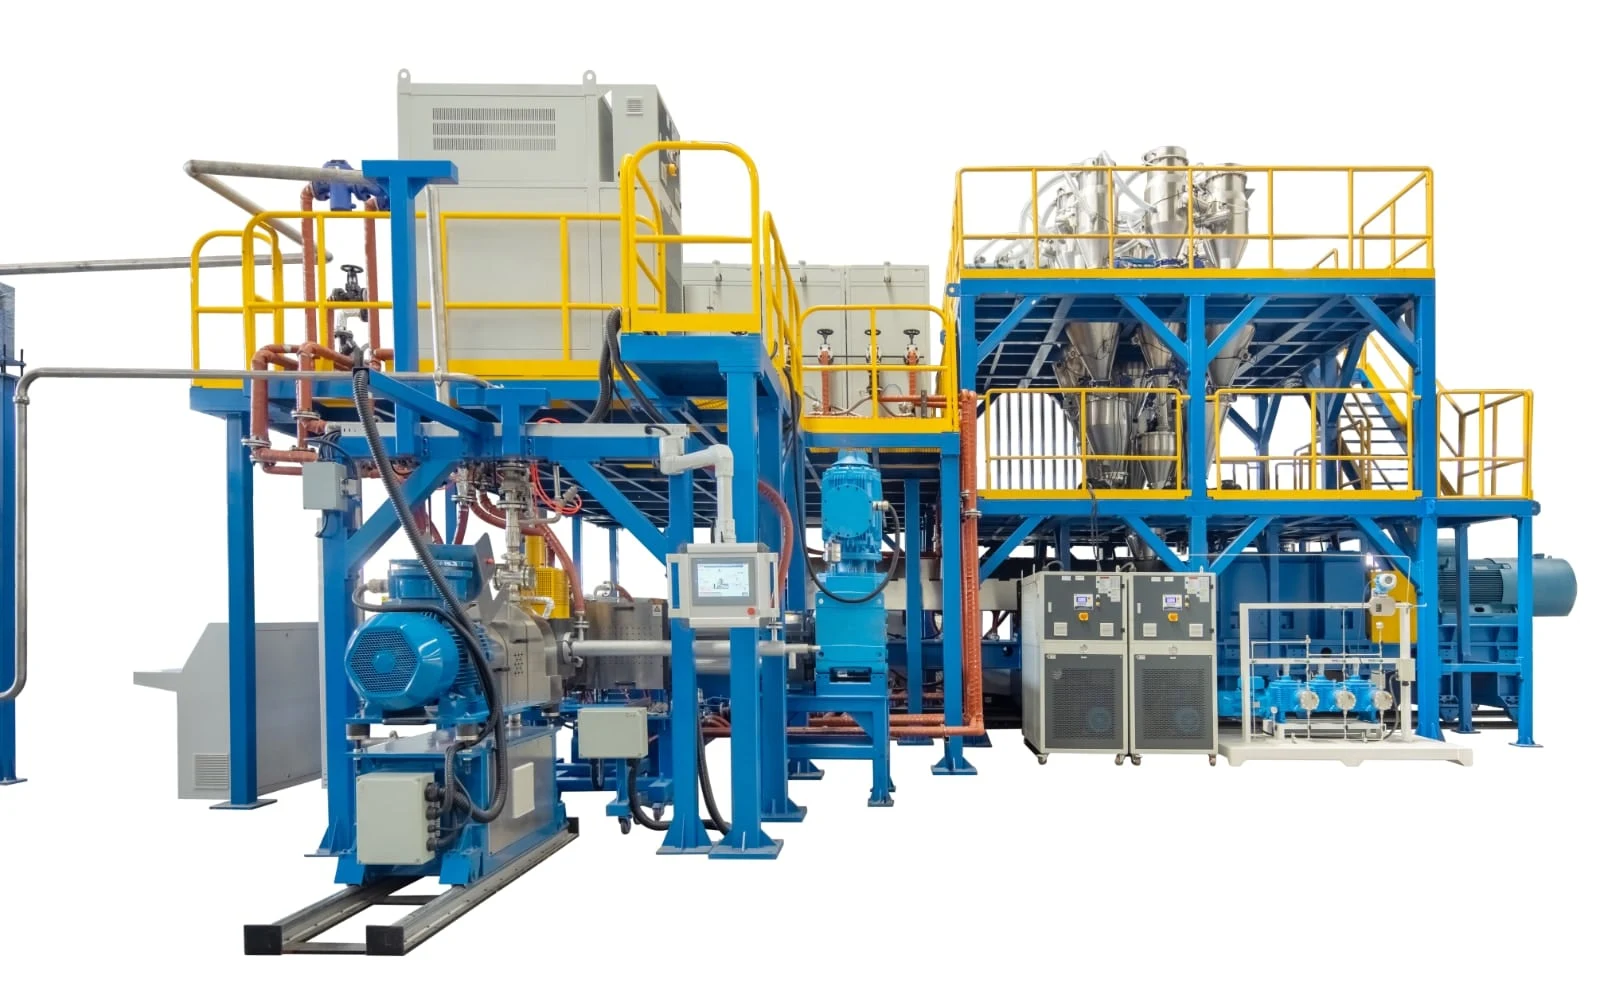
USEON builds complete foam extrusion lines for boards, sheets and beads, as single-stage and two-stage systems. From a 10 kg/h lab line to 3,000 kg/h production lines, each with its blowing agent system and intelligent control.
- Board
- Sheet
- Beads
Find your line by what you make
Seven lines, three product forms. Start from the form of the foam, then the polymer.
Board
Insulation and core material
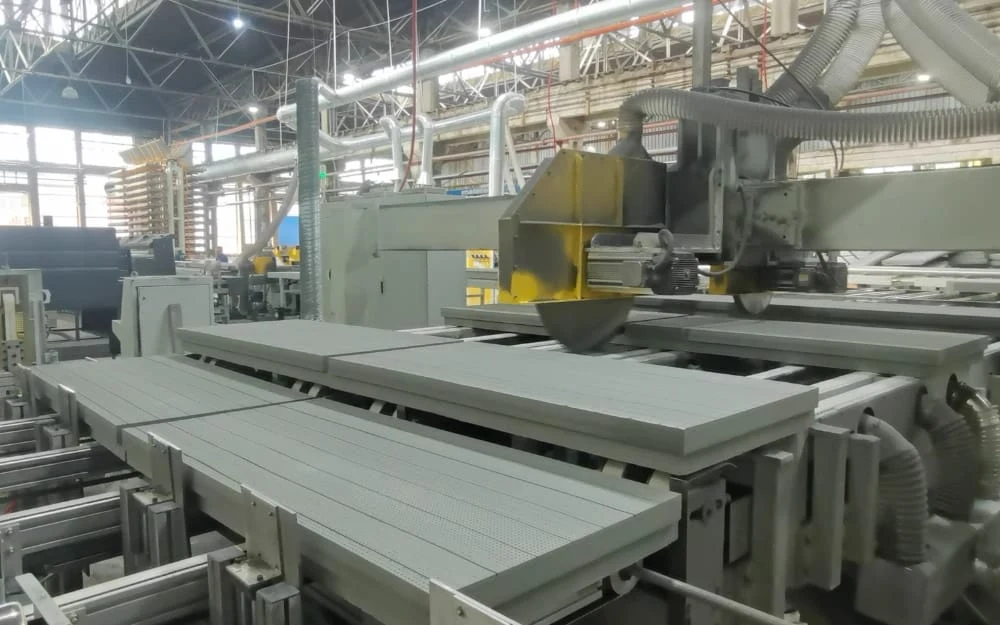
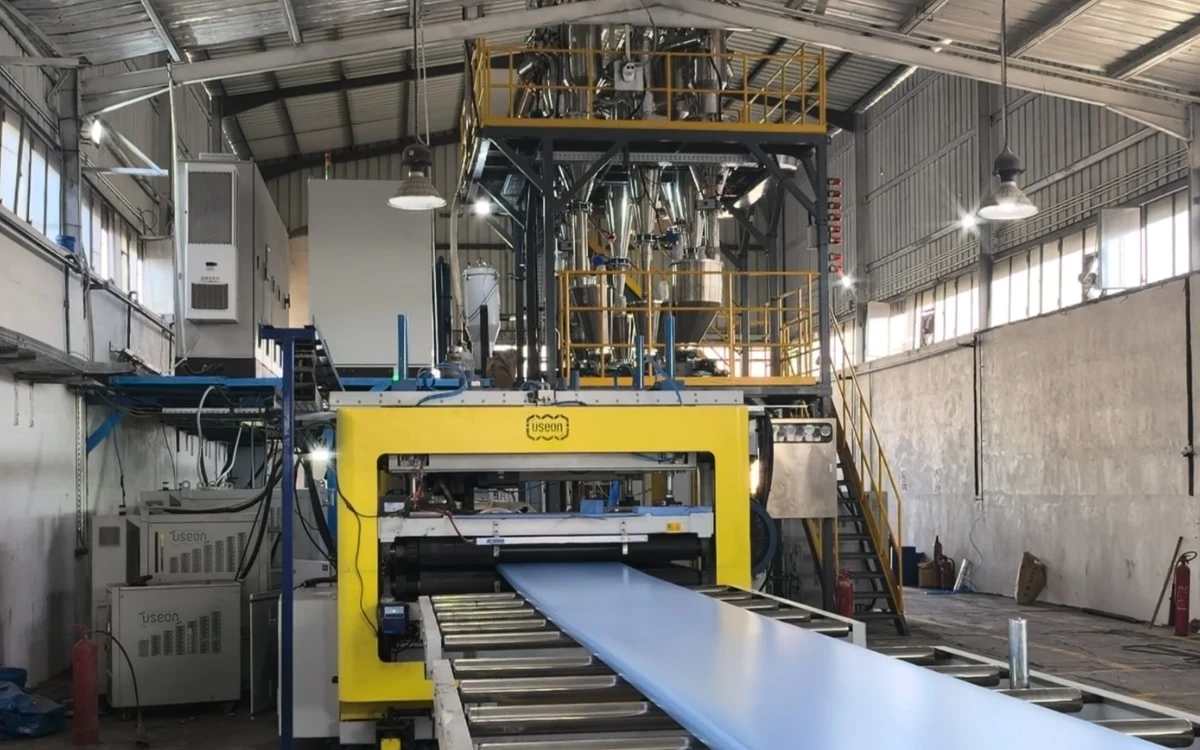 XPS Foam BoardCO₂ Foam XPS Production Line · ECOFEL seriesPSrecycled PSOutput200–3,000 kg/hBoard density25–50 kg/m³XPS production line
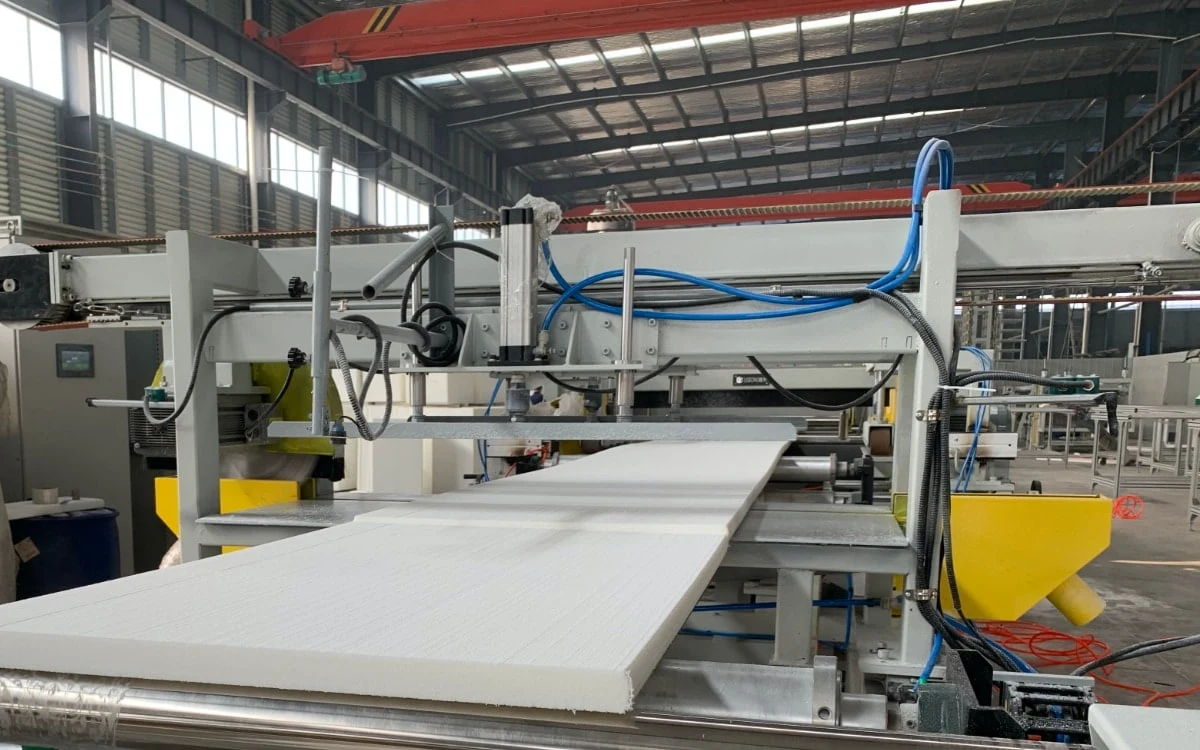 PET Foam CoreFor wind blades and composites, from recycled bottle flakesPETbottle flakesOutput80–800 kg/hCore density80–350 kg/m³PET foam core line
Sheet
Thermoforming and cushioning
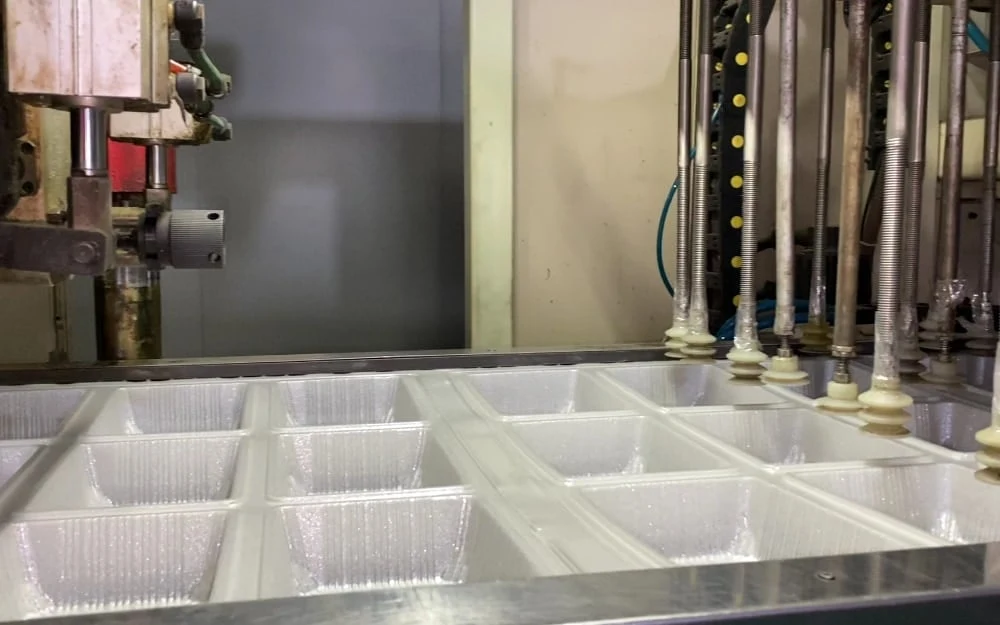
 XPE Foam SheetChemically cross-linked PE foam; XPE and IXPE machinesPESheet thickness3–12 mmSheet density25–135 kg/m³XPE foam sheet line Microfoam SheetA closed-cell foamed core between solid skins, for thermoformingPETPLAPSPCAgainst solid PET sheet30–40 % lighterPLA sheet0.5–1.5 mmMicrofoam sheet lines
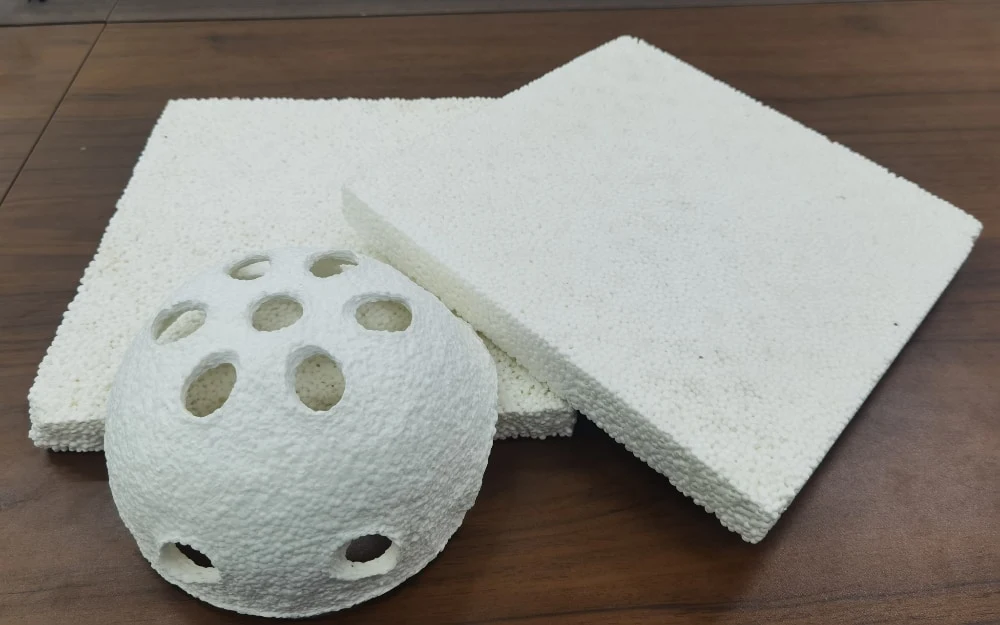
The lines side by side
Foam density tells the lines apart: from 20 kg/m³ bead foam to a microfoam sheet that is only slightly lighter than the solid polymer.
Logarithmic scale. Ranges as stated on each line page; PLA bead density is given there in g/L and the PLA sheet density in g/cm³. Extruded EPS beads leave the line unexpanded, so they have no foam density here.
| Line | Form | Polymer | How it foams | Output |
|---|---|---|---|---|
| XPS foam board | Board | PS, recycled PS | Blowing agent injected into the melt: CO₂, alone or combined. Tandem TDS + TDD. | 200–3,000 kg/h |
| PET foam core | Board | PET, bottle flakes | Reactive extrusion and CO₂ foaming in one line. | 80–800 kg/h |
| XPE foam sheet | Sheet | PE | Chemical: a master sheet is extruded and cross-linked, then expanded in a foaming oven. | up to 200–300 kg/h |
| Microfoam sheet | Sheet | PET, PLA (PS, PC) | Closed-cell core formed in the middle layer; the skins stay solid. | — |
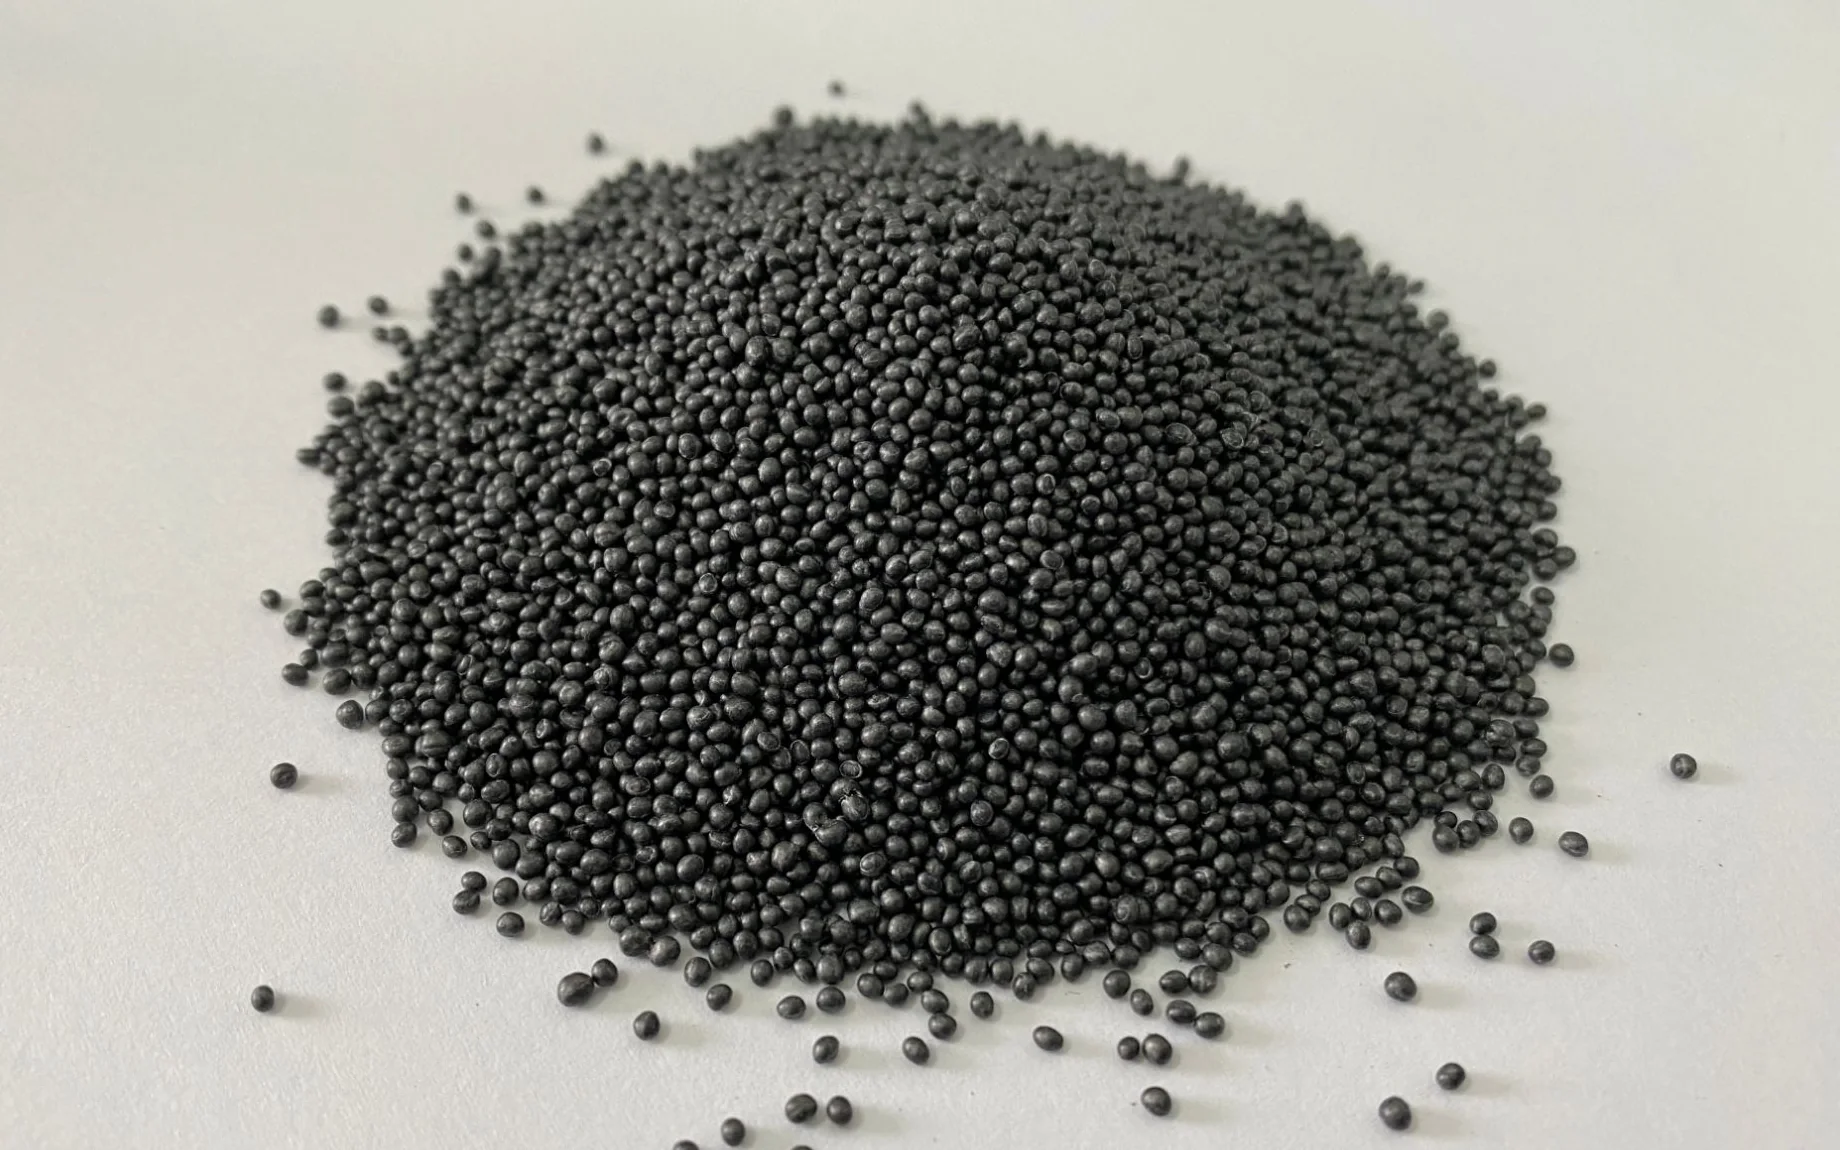
| Extruded EPS beads | Beads | PS + graphite or colour | Blowing agent encapsulated in the bead; expanded later at the moulder. Tandem, underwater pelletizing. | 200–3,000 kg/h |
| PLA foam beads | Beads | PLA | Supercritical CO₂ dissolved in the melt; foams at the die and is cut into beads. | — |
| Lab-scale line | Sheet, board, beads | By project | N₂, CO₂, HFO, HC and their combinations. | 10–100 kg/h |
What the lines share
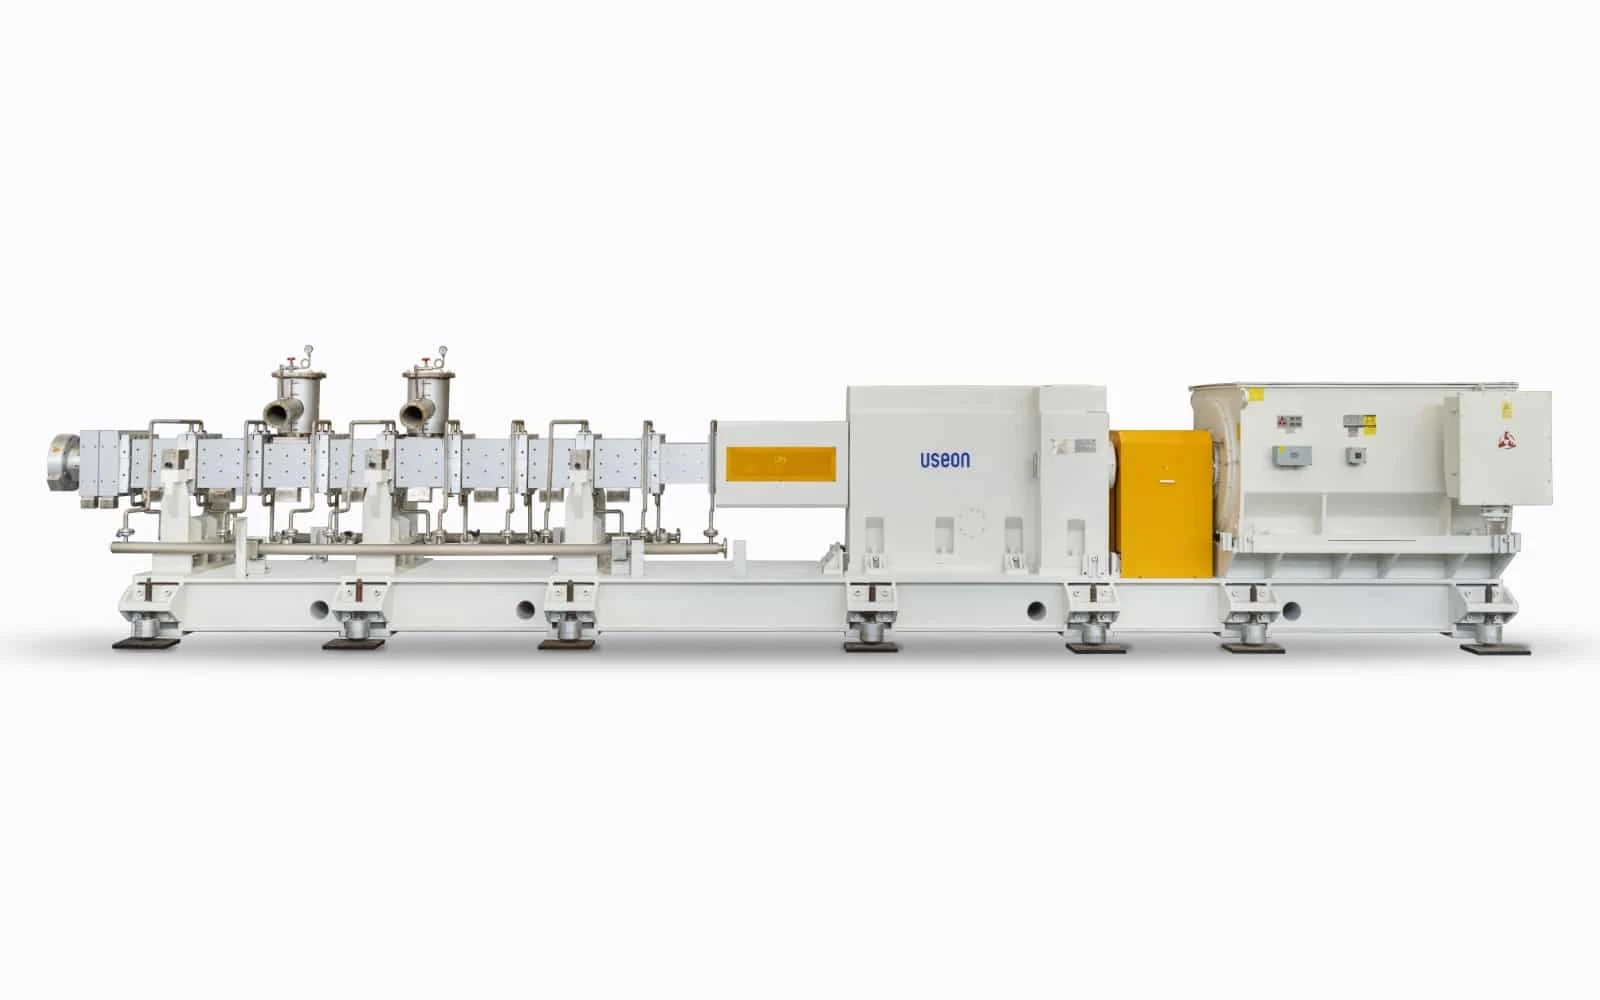
Foam extrusion asks for precision: the melt has to take up the blowing agent, then cool to foaming temperature before the die.
Optimized screw profile
The screw is laid out for the polymer and for taking up the blowing agent.
Highly efficient cooling barrel
The barrel design of our cooling single screw extruder increases cooling capacity by 80% compared with traditional designs.
Blowing agent system
N₂, CO₂, water, ethanol, HFO and HC. Multiple injection lets you shift the product portfolio.
Intelligent control system
One control system for the whole line, with data access for production management.
Foam lines in production
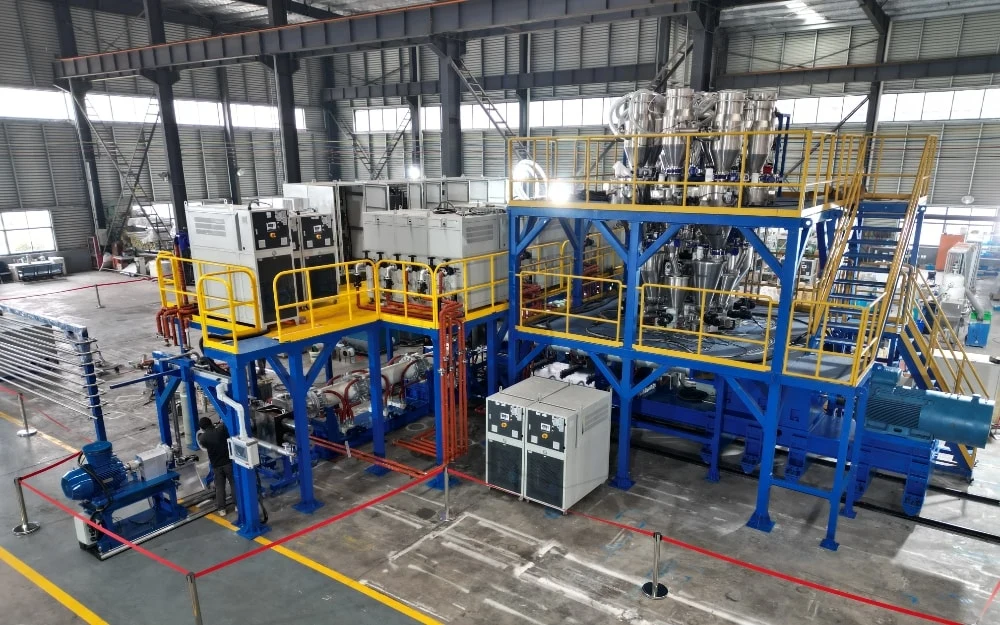
XPS board lines and a graphite EPS bead line, in production.
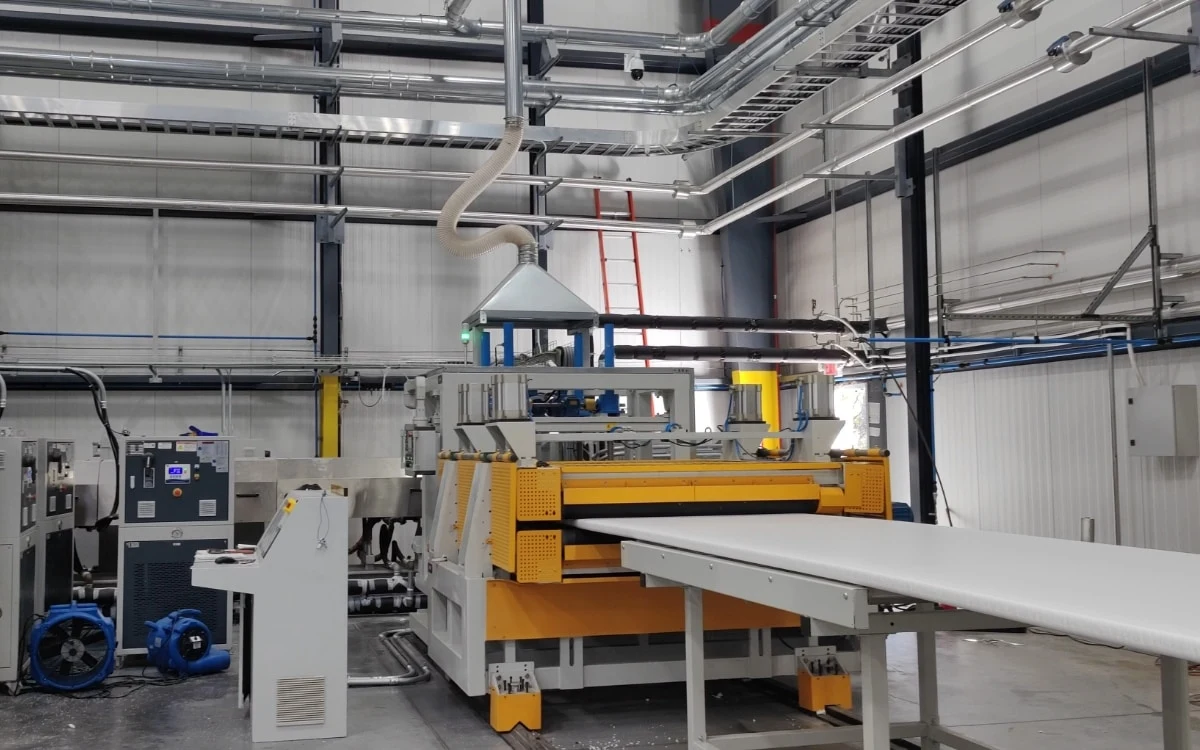 XPS · USA
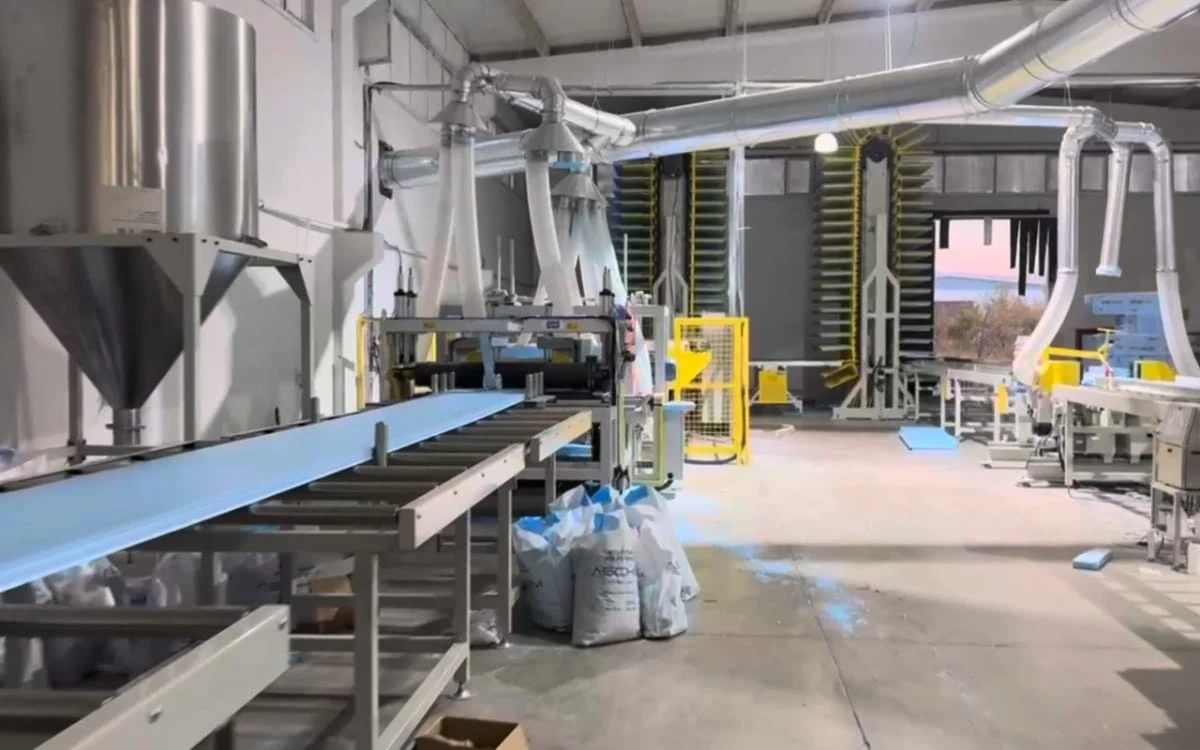 XPS · Turkey
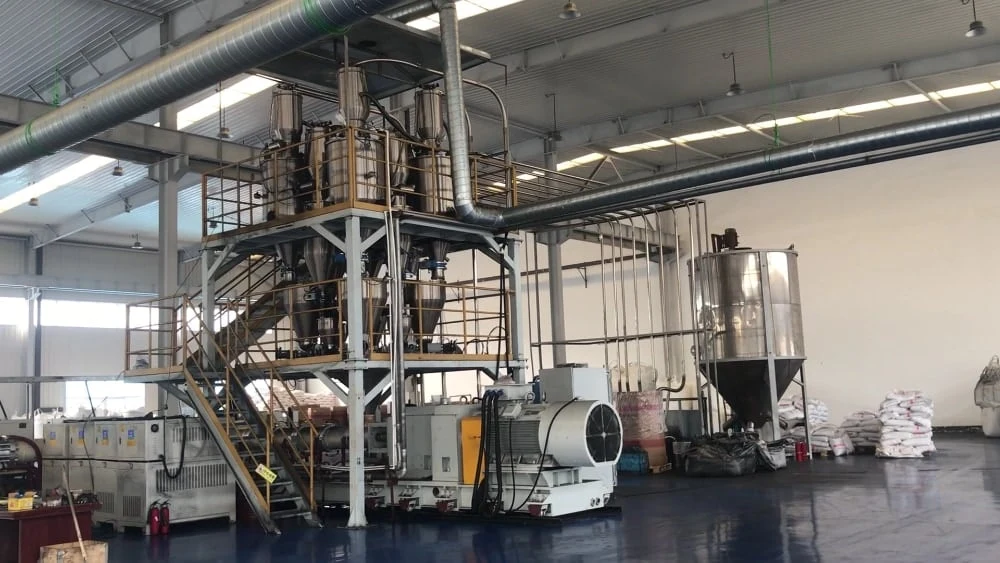 EPS beads · China
Foam know-how
How to choose an XPS production line
Capacity, configuration, budget and factory requirements.
Read the guide Blowing agentsHow to figure out the portfolio of blowing agents for XPS production
Which agents, alone or combined, for which board.
Read the guide MaterialsPET foam core: a better alternative to PVC foam core
PET and PVC foam core compared.
Read the guide- How to rise to the challenge for foam extrusion?
- How to Control Your CO2 in XPS Production Line
- The Ultimate Guide to XPS Foam Board
When the foam comes back
Get a quote
Tell us the product you want to make, the polymer and the output you need. We recommend the line and quote it as a turn-key project.
- 01Board, sheet or beads, and the polymer
- 02Target output, density and dimensions
- 03Line configuration and quotation
Cliff Zhang
Head of Foam Extrusion Division
Polymer foam extrusion, extrusion machinery R&D and international business development.