
Color Masterbatch
USEON has delivered more than 700 high-performance extruders for color masterbatch, which goes into any polymer and all kinds of products. Here is our experience with the special applications: fibre, special-effect and micro pellet masterbatch.
- Mono · SPC
- Tailor-made
- Customized
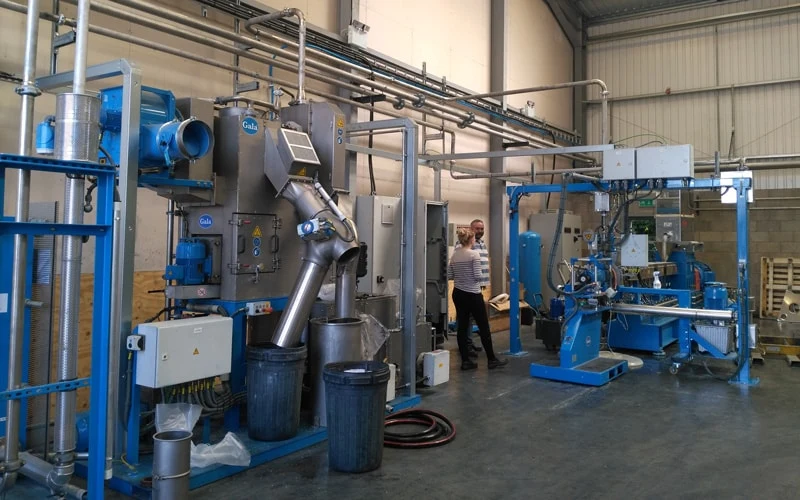
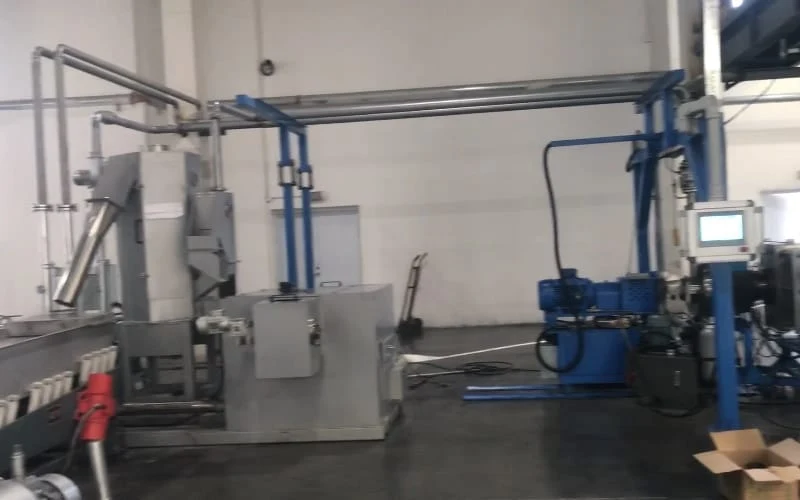
- Extruders delivered for color masterbatch
- 700+sets
- Colours for PP carpet, BCF & CF yarn
- 20,000+
- Strand die plate change between colours
- 2min
- Micro pellets, underwater pelletizing
- ≤ 1mm
Three types of color masterbatch
Color masterbatch compounding is one of the main applications for the twin screw extruder. What you make decides how the line is built.
Mono color masterbatchSPC · single pigment concentrate
Polymer compounded with one single pigment, mostly without wax and additives.
Tailor-made masterbatchCustom colouring
Different mono color masterbatch pellets mixed to reach the colour the customer wants.
Customized masterbatchPolymer + pigments + additives
Polymer mixed with several pigments and additives in one compounding step.
The basic formula
Pigment loading by pigment type, with the base resins and additives we compound.
Base resin
Additives
Pigment loading
Applications
Color masterbatch goes into fibre, film, blow moulding, extrusion and injection moulding. Five of them need a special line.
Carpet, textiles, upholstery
Shopping bags, cast film, multilayer film
Medical & cosmetic containers, lubricant & paint containers
Sheet, pipe, wire & cable
Automotive, electronics, construction, housewares, furniture, toys
Experience for special applications
| Application | Base | Feeding | Extruder | Pelletizing | What decides the line |
|---|---|---|---|---|---|
| PP mono & tailor-made · BCF / CF | PP | Premix, or split feeding | SAT-T triple (mono); SAT twin (tailor-made) | Water-cooling strand | 20,000+ colours: mono first, then tailor-made |
| PBT · POY & FDY | PBT powder | Premix | SAT-T triple, small size | — | Low viscosity, strong vacuum, minimum IV drop |
| PET · PSF | Recycled PET flakes | Split feeding, two LIW feeders | — | Under water strand | 25–40% carbon black, almost no waste |
| Special-effect | — | Side force feeder, 5th barrel | Distributive kneading elements | — | Shear-sensitive pigments up to 170 μm |
| Micro pellets | — | — | — | Underwater pelletizing | Pellets ≤ 1 mm, lower dosage |
Color masterbatch for fibre
Carpet yarn, filament and staple fibre each ask for something different.
Mono first, then tailor-made
There are more than 20,000 colours for PP carpet, BCF and CF yarn. It is better to make mono color masterbatch first, then produce tailor-made masterbatch for the final product.
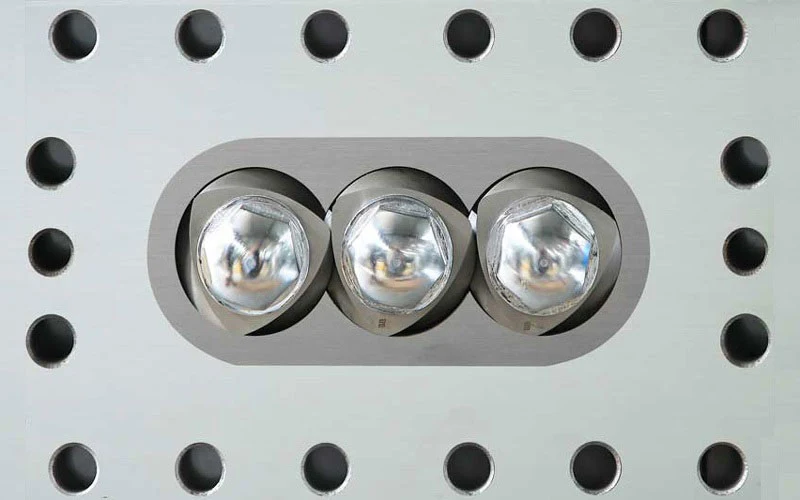
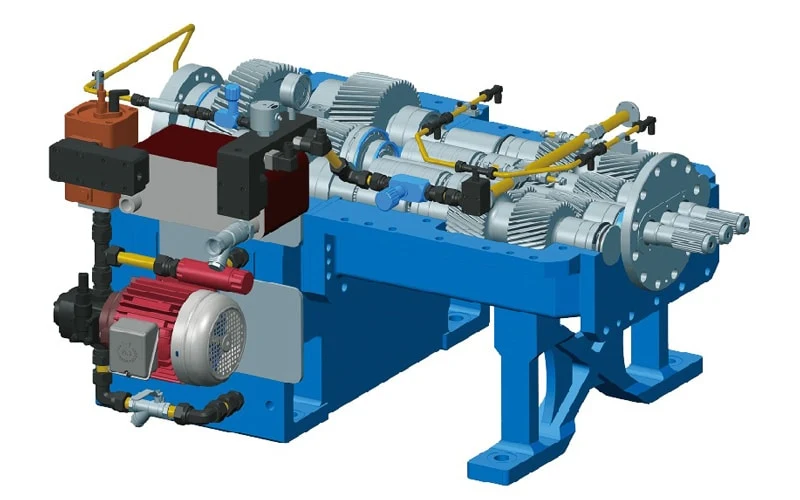
SAT-T triple screw extruder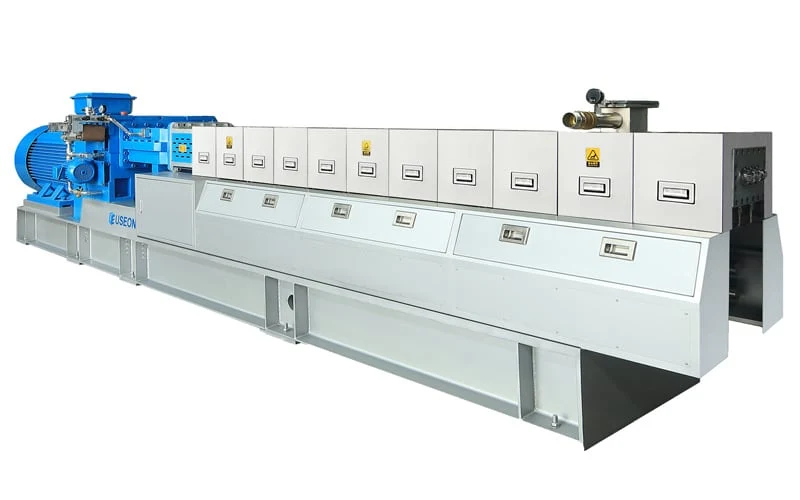
Mono color masterbatch
MachineSAT-T triple screw extruder
- One extruder for one colour family, such as light red to dark red.
- Most pigments need premixing: a separate room with dust collection for the mixer.
- PP powder for one-time compounding; PP pellets if you compound twice with split feeding the first time.
- Triple screw: 40% extra free volume and one more screw for better dispersion and more output.
Tailor-made masterbatch
MachineSAT twin screw extruder
- Clean production with a high degree of automation.
- High torque and high screw speed for more output.
- Fast-cleaning strand die plate without heater: 2 minutes to change colour.
Tailor-made: two types of process
- Mixer
- Twin screw extruder
- Water-cooling strand pelletizing
- Loss-in-weight feeding
- Twin screw extruder
- Water-cooling strand pelletizing
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT-T52 | 51.4 | 600 | 110 | 44–48 | 250–350 |
| SAT-T65 | 62.4 | 600 | 160 | 44–48 | 450–600 |
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT40 | 41 | 800 | 55 | 40 | 150–200 |
| SAT52 | 51.4 | 800 | 110 | 40 | 250–350 |
| SAT65 | 62.4 | 800 | 160 | 40 | 450–600 |
Low viscosity, small clearances
PBT base color masterbatch for filament yarn.
- PBT has a lower viscosity than PP, so it needs a special screw design.
- PBT in powder form is necessary for premixing: a separate room and dust collection for the mixer.
- A strong vacuum system removes moisture and keeps the IV drop to a minimum.
- The triple screw extruder gives better dispersion and more output.
- The clearance between the screws, and between screw and barrel, should be minimal, so a small extruder is better.
Bottle flakes plus carbon black
PSF is always made from recycled PET. The dispersion requirement is lower than for POY masterbatch.
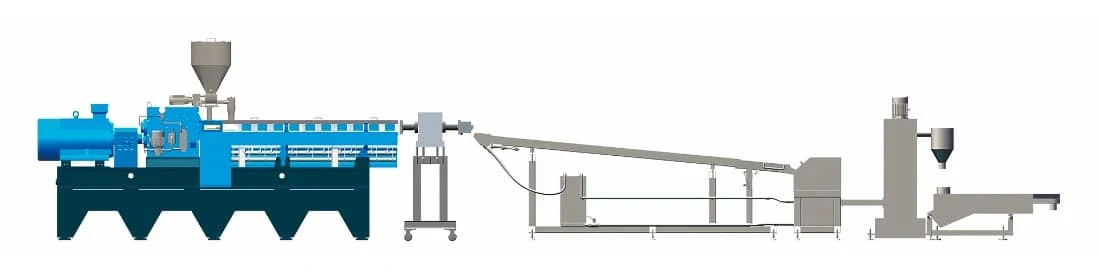
Under water strand pelletizing- The most popular formula: bottle flakes under 10 mm compounded with 25–40% carbon black powder.
- Split feeding by two loss-in-weight feeders, with minimum dust.
- Under water strand pelletizing for more output: the water flow carries the strands into the pelletizer, even when they break during a filter change, so there is almost no waste.
Special-effect and micro pellet masterbatch
Distribute, don’t grind
Effect pigments serve decorative and functional purposes and have become an essential part of modern product design. They refine selected colours and make the end product unique.
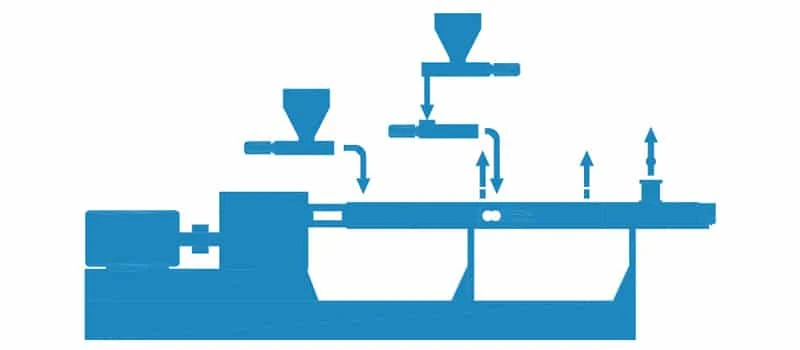
- Effect pigments have a layer structure, with particle size up to 170 μm, and are sensitive to shear.
- Split feeding: the pigment enters the fifth barrel through a side force feeder.
- Special kneading elements with more distributive than dispersive effect: less shear, more mixing.
Pellets of 1 mm or less
Made with the underwater pelletizing system.
Underwater pelletizing system- Their small size lets micro pellets spread more uniformly and distribute finer, like the raw polymer itself.
- Normal-sized masterbatch pellets must be dosed higher for the same effect; micro pellets need less colorant, a significant saving since masterbatch costs far more than the polymer.
- Easier to handle, better to dose, and dust free.
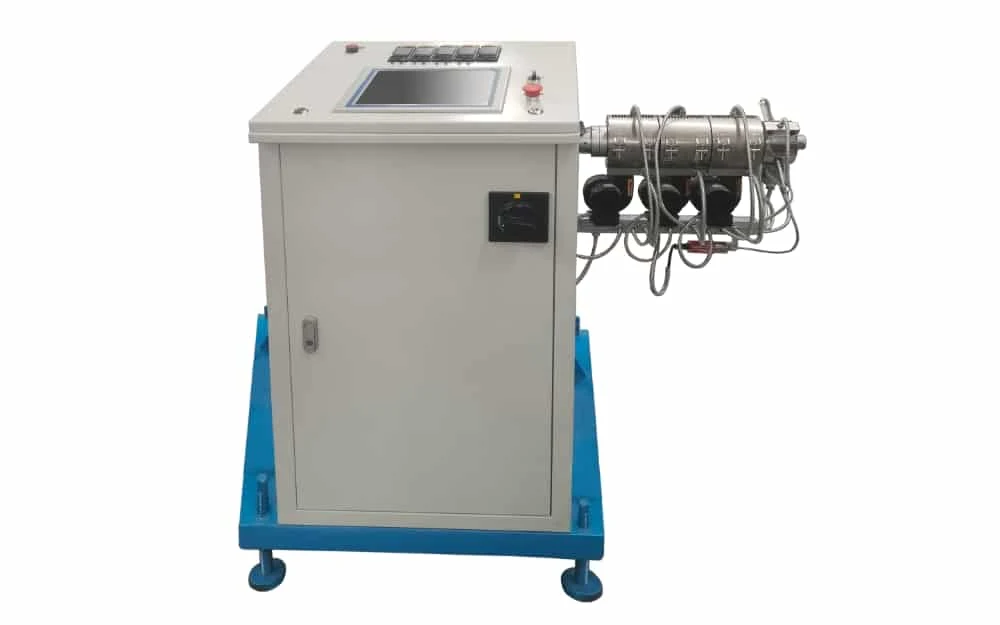
Filter pressure value (FPV) tester
USEON also supplies an FPV tester for masterbatch dispersion. It is a necessary test machine for professional BCF or POY color masterbatch producers.
- 01
Nitrided plate screen changer
Manual, high hardness and wear resistance.
- 02
High-precision melt pressure sensor
An accurate melt pressure reading.
- 03
HMI records the result in bar/g
Recording and calculation directly on the HMI.
Testing process
- 1
Premix 1 kg
950 g polymer and 50 g pigment, premixed for each test.
- 2
10 μm filter
About 1250 mesh.
- 3
Read the rise
Pressure rise after 1 kg, divided by the pigment.
FPV = (70 − 30) bar / 50 g = 0.8 bar/g
The lower the value, the better the dispersion.
Project · Turkey
400 kg/h black masterbatch line in Turkey
A SAT75 twin screw extruder line for black masterbatch, delivered to Turkey with an output of 400 kg/h.
- Extruder
- SAT75 twin screw
- Application
- Black masterbatch
- Output
- 400 kg/h
- Location
- Turkey
More color masterbatch lines
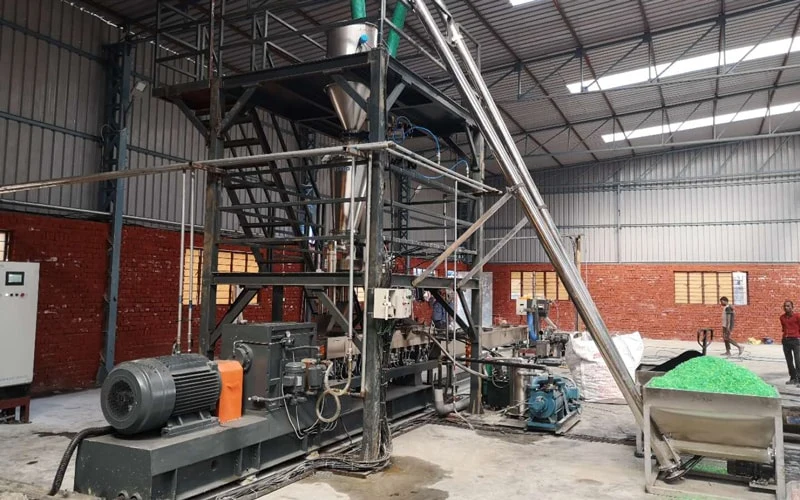 India
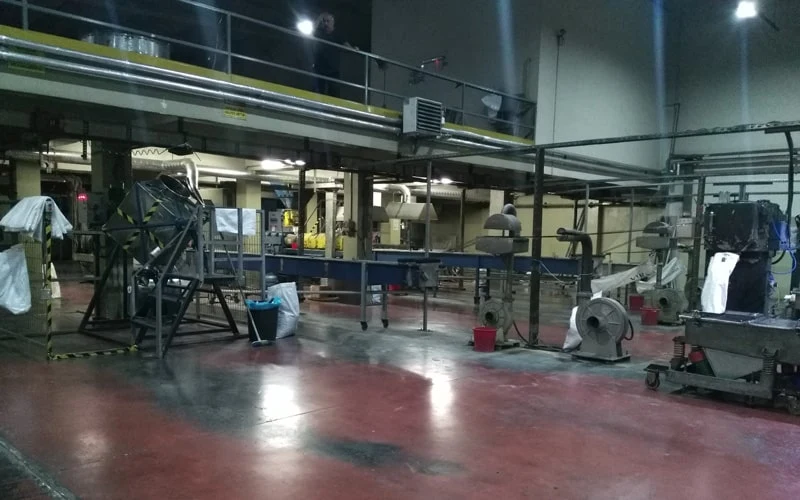 Turkey
Get a quote
Tell us which masterbatch you make (mono, tailor-made or customized), the base resin, the pigments and loading, and the end product. For fibre grades, tell us the yarn and the filter pressure value you need.
- 01Masterbatch type, resin & pigments
- 02Feeding, extruder & pelletizing
- 03Colour change & dispersion targets

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.