
Engineering Plastic
Engineering plastic compounding is a main application of the twin screw extruder. These polymers are sensitive to overheating and hydrolytic degradation, so we build for high torque and high speed: more output with less residence time, better dispersion and accurate temperature control. From short glass fibre to long-fibre thermoplastics.
- Short fibre
- LFT-G
- UD tape
- Direct LFT
- Glass fibre length in short-fibre pellets
- 0.2–0.3mm
- LFT-G pellets, fibre as long as the pellet
- 6–16mm
- Modulus and impact of LFT-G vs. short-fibre compounds
- 2× · 4×
- U6 line in Germany, up to 50% glass fibre and powder
- ~800kg/h
Materials and applications
The basic formula: a general or advanced engineering plastic, reinforced and modified with fibres and additives.
General engineering plastics
Advanced engineering plastics
Additives
Intake manifolds, header tanks, filters, fans and shrouds, engine covers
Terminal blocks, cable ties, connectors, power tools, MCCB, relays, lights
BOPA, BOPET, PET sheet, pipe
PA fibre, PSF, FDY
Construction, housewares, furniture, toys
Processing of engineering plastic
High torque, short residence time
Engineering plastic is sensitive to overheating and hydrolytic degradation. Our SAT-X series extruder, with 13 Nm/cm³ specific torque and 800 rpm screw speed, reaches higher output with less residence time, better dispersion and more accurate temperature control.
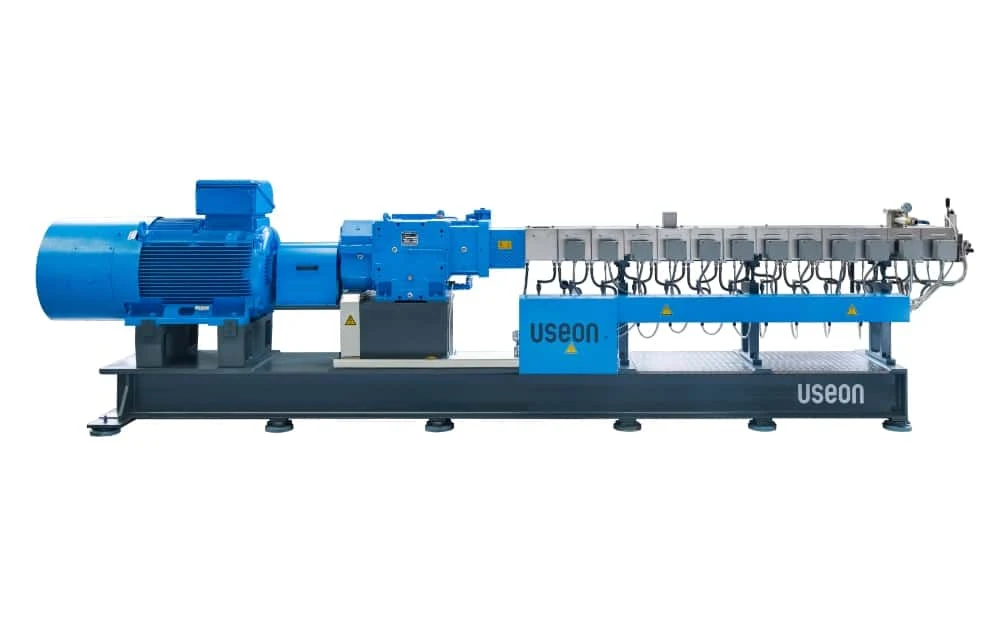 EquipmentU+ Series Twin Screw ExtruderOur high-torque platform for PEEK, PPSU and glass-fibre compounds.
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT-X52 | 51.4 | 800 | 160 | 40–44 | 450–700 |
| SAT-X65 | 62.4 | 800 | 280 | 40–44 | 750–1200 |
| SAT-X75 | 71.4 | 600 | 355 | 40–44 | 850–1500 |
Output depends on polymer, fibre content and pelletizing.
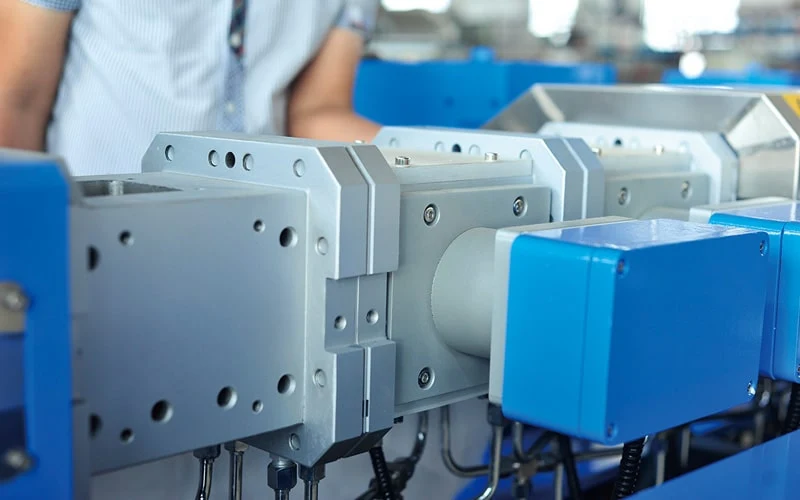
Heating inside the barrel
Cartridge heaters made in Germany sit inside the barrel instead of cast heaters outside. The polymer melts mostly by heat, not by kneading, so screw and barrel last longer and the compound is better.
Saves energy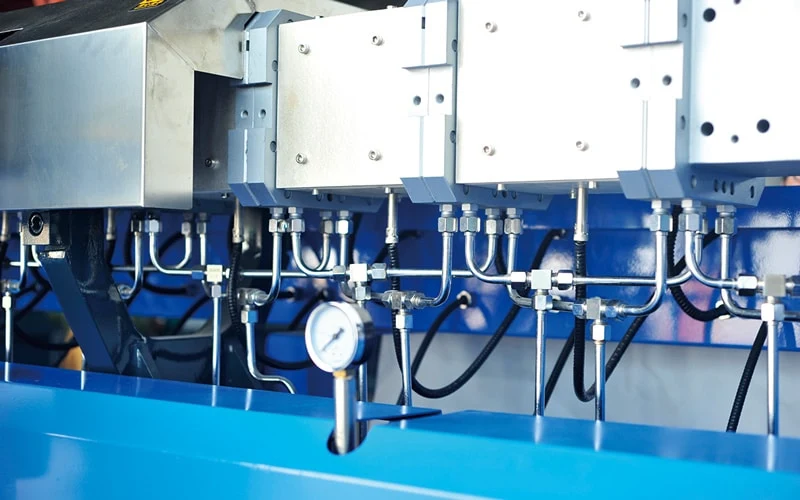
Two-way barrel cooling
Two inlets and outlets on each barrel give more uniform and faster cooling.
Temperature control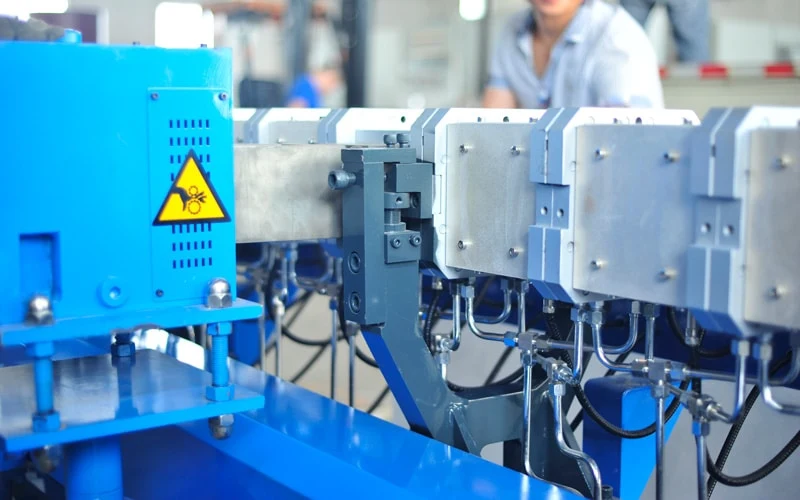
Supported at the centre
A barrel supported underneath expands upward by 0.2–0.5 mm when heated, leaving uneven gaps. Ours is supported in the middle, so it expands evenly up and down and the gaps stay even.
Even screw clearance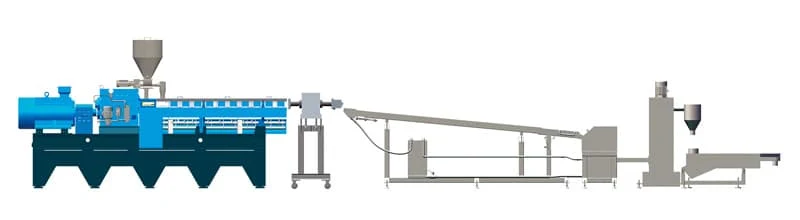
Under water strand pelletizing
Water flow carries the strands into the pelletizer, even when they break during a filter change: almost no waste. Above about 25 strands (around 800 kg/h), hot strands are hard to handle by hand.
> 800 kg/hFour ways to reinforce with fibre
The longer the fibre stays in the part, the higher the mechanical properties. Each route keeps a different fibre length.
- 01 · Compounding
Short fibre reinforced
Roving or chopped glass fibre goes straight into the twin screw extruder and is compounded with the polymer.
- Fibre in
- Roving, or chopped 4–6 mm
- Entry
- 5th barrel
- Product
- 4 mm pellets
- Fibre in pellet
- 0.2–0.3 mm
- 02 · Indirect LFT
LFT-G
Rovings pass through an impregnation die and are coated by PP melt from the twin screw extruder. The pellets go to any injection moulding machine.
- Fibre in
- Glass rovings
- Product
- 6–16 mm pellets
- vs. short fibre
- 2× modulus · 4× impact
- Low temperature
- Keeps function at −30 °C
- 03 · Tape
UD tape
Glass or carbon rovings enter a T-die and are coated by PE / PP / PET / PA melt. For building wall panels and truck and trailer bodies.
- Fibre
- 50–60%
- Width
- 610 or 1,220 mm
- Thickness
- 0.25–0.35 ±0.02 mm
- Line speed
- 6–12 m/min
- 04 · Direct LFT
LFT-D-IMC / LFT-D-ECM
Fibre and matrix are combined right before the moulder, with no intermediate product and a single heat history.
- D-IMC
- Attached to an injection machine
- D-ECM
- Two extruders + hydraulic press
- Additions
- Fillers, flame retardants, additives
Short-fibre and long-fibre lines in detail
Two ways to feed the glass
Roving and chopped fibre both enter at the fifth barrel, after the polymer has melted.
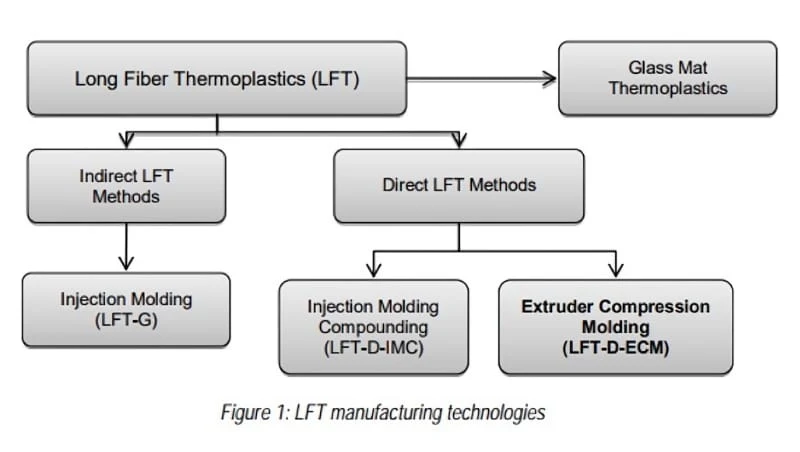
Three processing methods for LFT parts
LFT parts are typically made by one of three methods: indirect (LFT-G pellets for injection moulding), direct injection moulding compounding (LFT-D-IMC), or extruder compression moulding (LFT-D-ECM).
- D-ECM advantage 1Compounding and fibre mixing are separated, so each extruder is optimised for its own job.
- D-ECM advantage 2The material sees less stress than in injection moulding, which keeps the fibre long: critical for automotive parts.
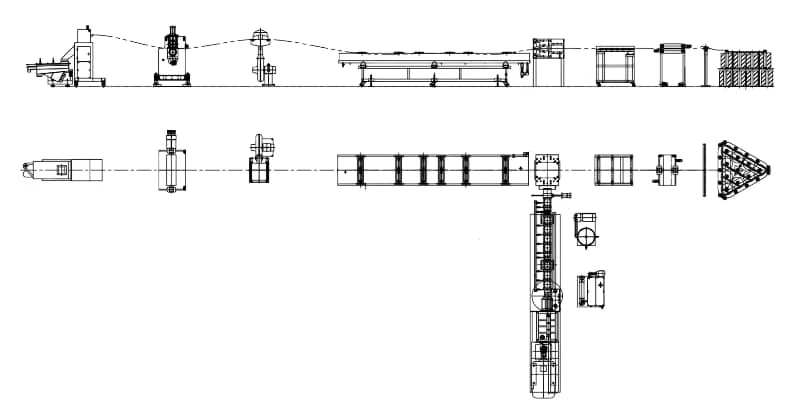
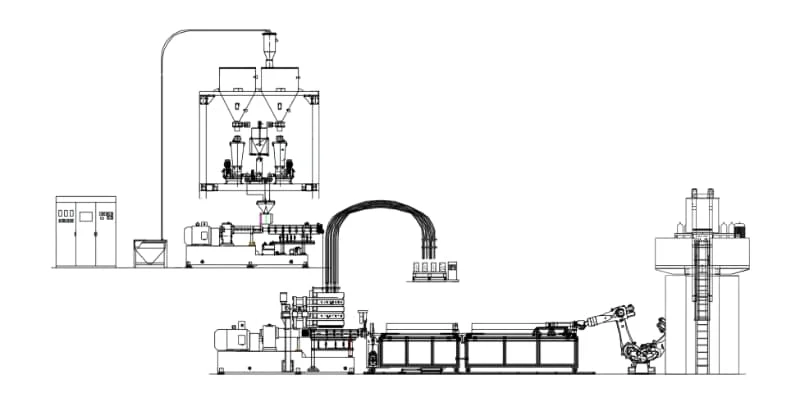
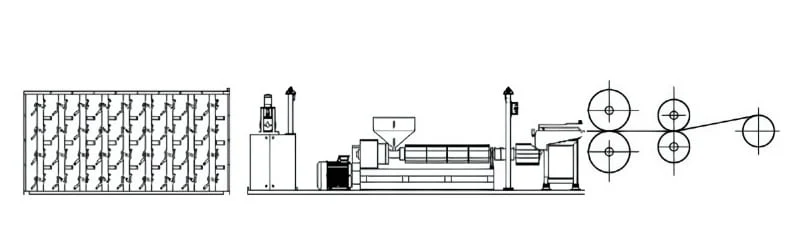
Thermoplastic UD tape extrusion line
SAT40 or SAT52 twin screw extruder. For PP base sheet a single screw extruder is fine; for PA or PET base it should be a twin screw.
- Fibre creel
- Traction unit
- Gravimetric batch mixer
- LIW feeder
- Twin screw extruder
- Melt filter
- Impregnation die
- Pressure calibrating
- Cooling stack & edge cutting
- Winder
See the lines running
Glass-fibre compounding, LFT-G on three extruder sizes, LFT-D-ECM and a continuous-fibre tape line.
Project · Germany
Up to 50% glass fibre and powder at ~800 kg/h
A German compounder of PBT, PA and PP needed a line for high glass-fibre and mineral loadings, CE-compliant and linked to its SAP system.
- Extruder
- U6-48
- Drive
- Siemens 280 kW
- Gearbox
- Zambello · 900 rpm
- Pelletizing
- Under water strand
Base resin 12–90%, inorganic powder 10–50%, glass fibre 10–50%, additives 1–5%.
Wear-resistant alloy barrel liners and screw elements in the working section.
A single-stage side feeder downstream lets the fibre join after the resin has melted.
Stable pelletizing at around 800 kg/h on site.
More engineering plastic lines
From a lab extruder for PA66 with 45% glass fibre to production lines for PPS and PPSU.
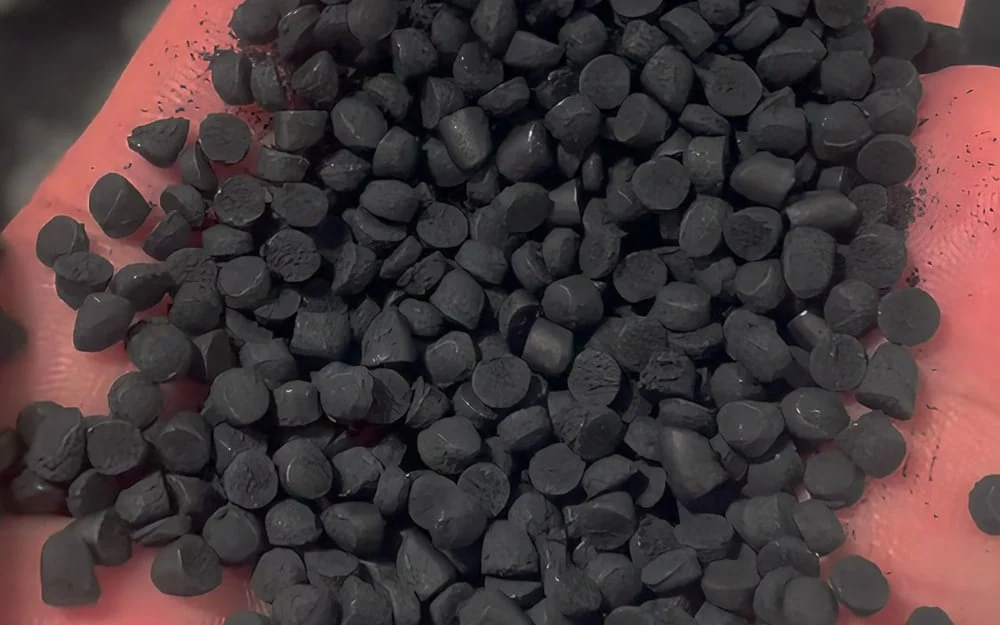 U6
PPS with carbon nanotube masterbatch and glass fibre
Air-cooling die face500–600 kg/h
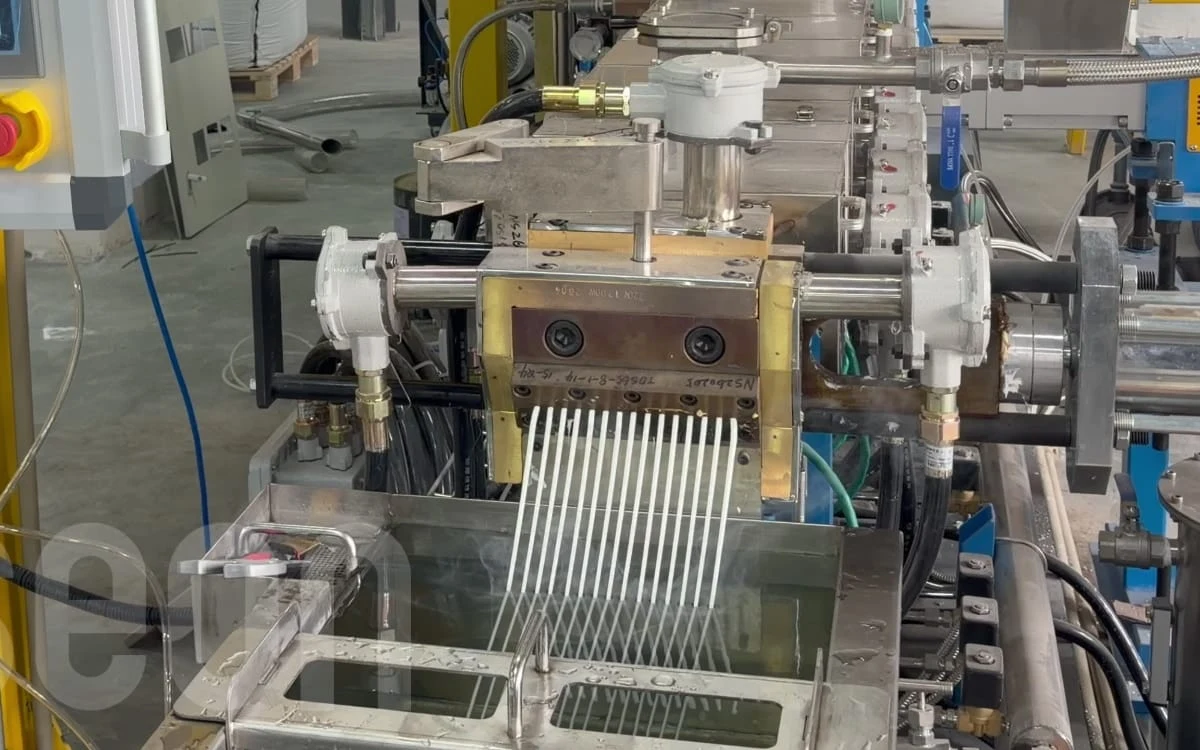 SAT65
Explosion-proof line for PLA, PETG and ABS with carbon fibre
Ex tb IIIC500–700 kg/h
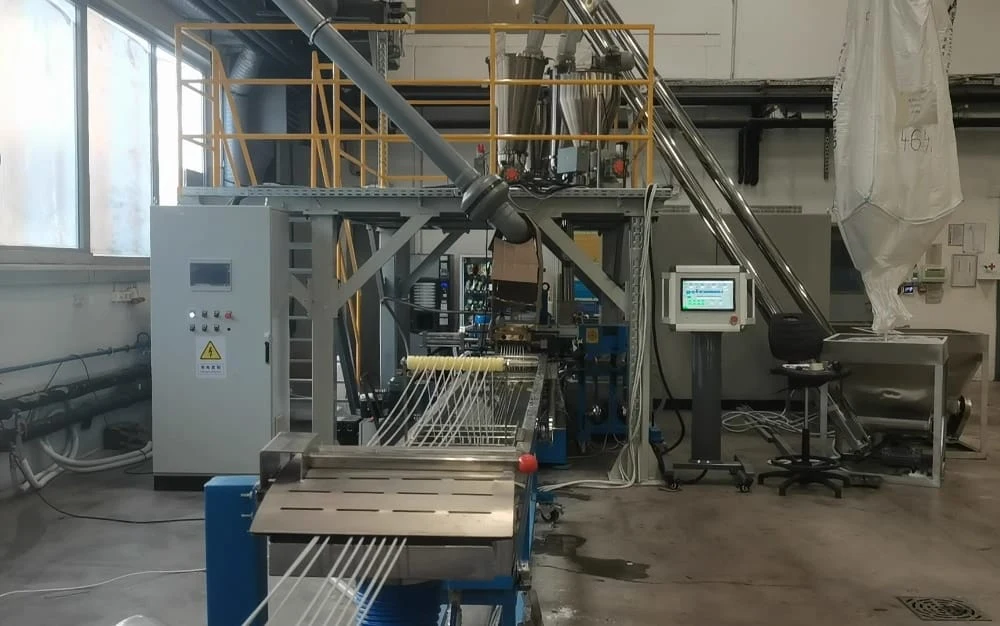 SAT52
PA / ABS / PC with glass fibre
Water-cooling strand200–350 kg/h
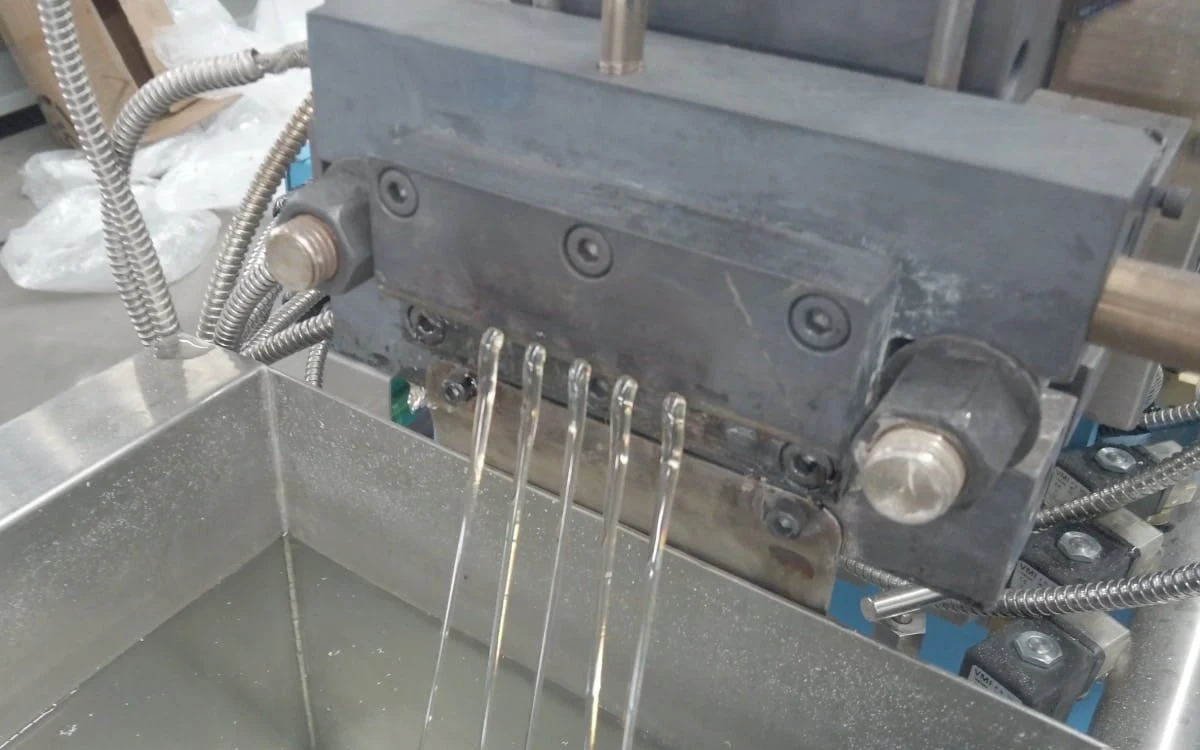
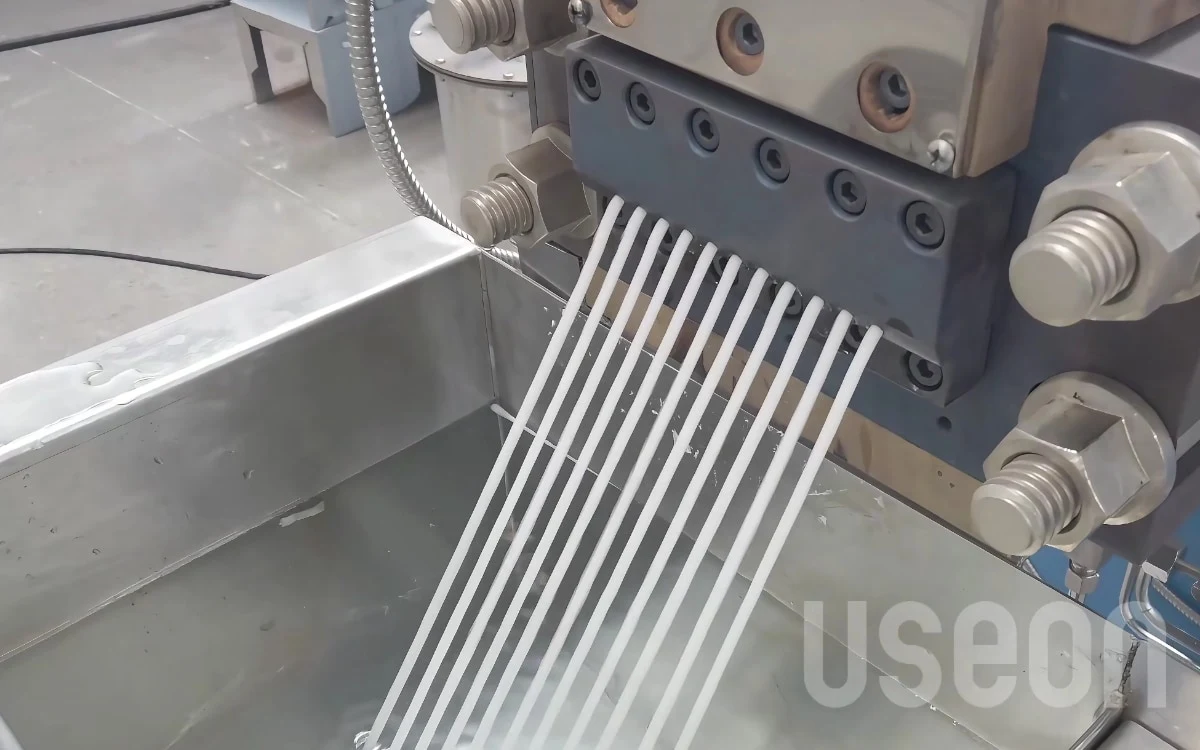 SAT52
PP with 30% short fibre
Water-cooling strand300 kg/h
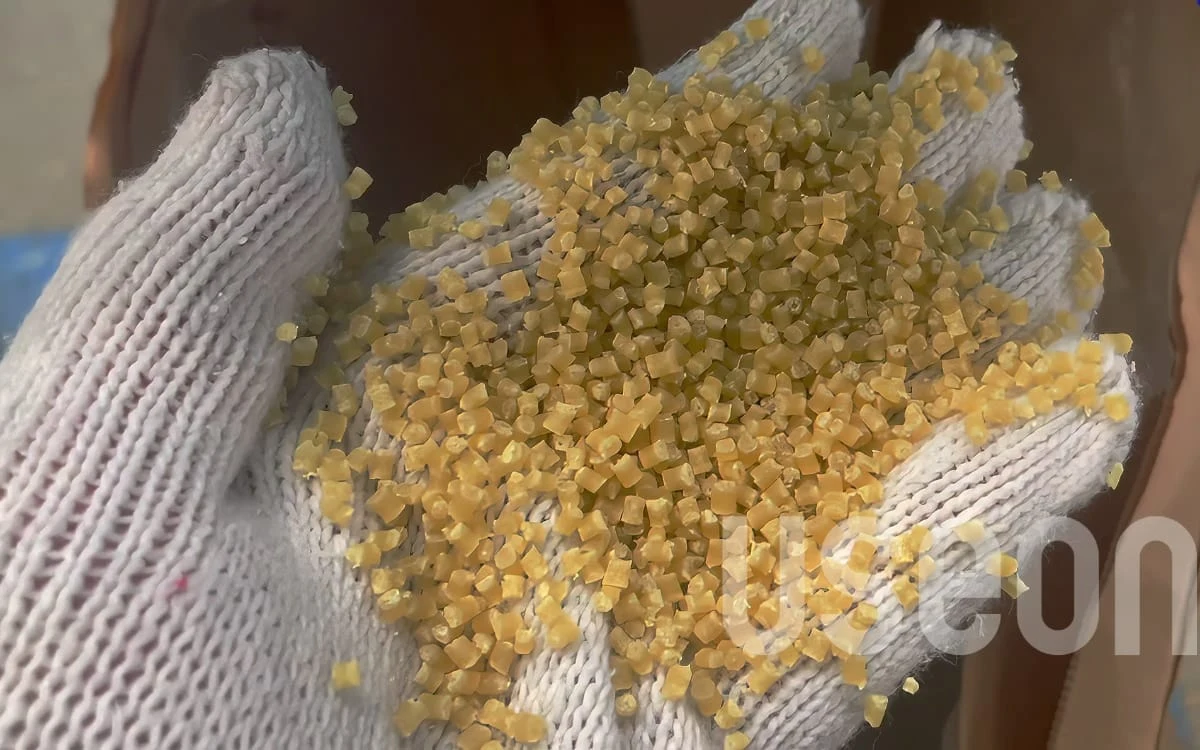
 U3
PPSU pelletizing line
Water-cooling strandU3
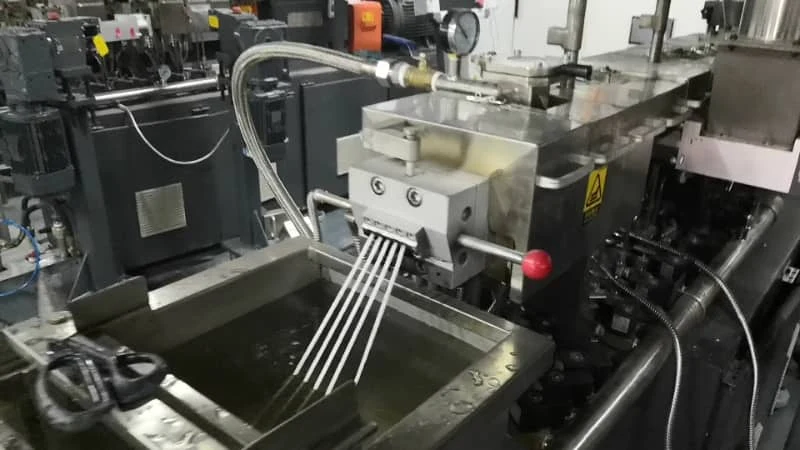
 Lab
PPO with 25% fibre on a SAT35
Water-cooling strandSAT35
 Lab
PA66 with 45% glass fibre on a LAB-30
LAB-3030–50 kg/h
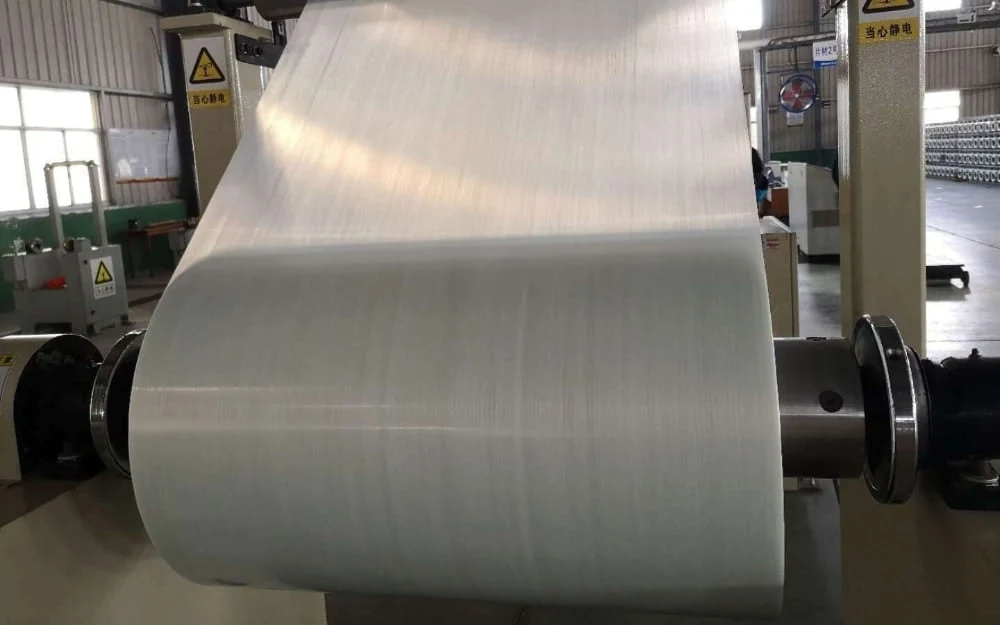 Tape
Continuous fibre reinforced thermoplastic tape line
Up to 70% glass fibre3 t/day
Get a quote
Tell us the polymer, the fibre or filler and its content, and how the compound will be moulded. Short-fibre pellets, LFT-G pellets, UD tape and direct LFT need different lines; we start from the part and the fibre length it needs.
- 01Polymer, fibre & additives
- 02Route: pellets, tape or direct LFT
- 03Extruder, feeding & pelletizing

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.