
Tandem Extrusion System
A twin screw extruder and a single screw extruder in series. The primary twin screw extruder provides mixing and dispersion without over-shear; the lower-speed single screw extruder provides cooling and pressure accumulation. For shear-sensitive or heat-sensitive materials and for pelletizing without water.
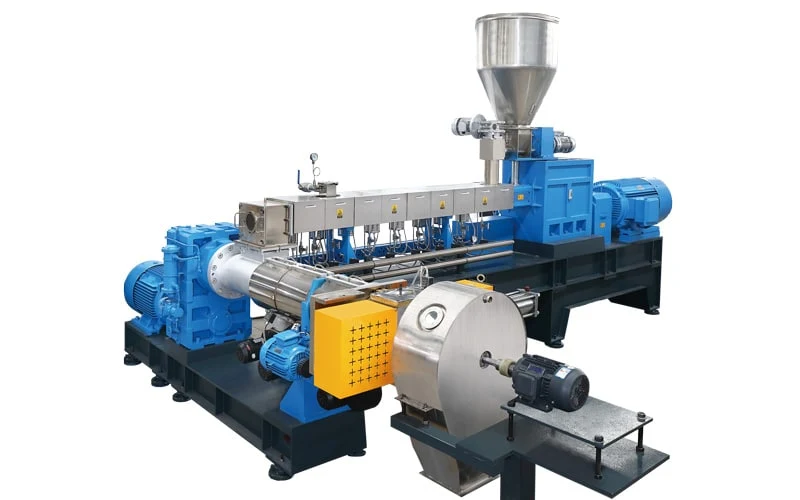
- Output, four sizes
- 200–2,500kg/h
- Maximum speed, twin screw / single screw
- 600 / 90rpm
- Twin screw / single screw
- 32–64 / 8L/D
Two stages, two jobs
What each extruder does, and why they are separated.
- Certain polymers require pelletizing without water and moisture, so the extrusion system needs sufficient cooling capacity of its own.
- Shear-sensitive or heat-sensitive materials: the primary twin screw extruder provides mixing and dispersion without over-shear.
- The lower-speed single screw extruder provides cooling and pressure accumulation.
Twin screw
The standard for compounding. Usually the more economical choice.
- Sizes
- SAT, U+, EC, TDY, Lab
Triple screw
When feeding volume limits the output: light powders, very high filler loading.
- Sizes
- SAT-T35 to SAT-T95
This page
Tandem: twin + single
Mixing in the twin screw, cooling and pressure build-up in a slow single screw.
- Sizes
- SAT52-TDD150 to SAT95-TDD240
Single screw
Melt extrusion with venting, force-fed lumps, or the second stage of a tandem.
- Sizes
- TDD20 to TDD500
Typical application
SolutionPVC Compounding SolutionCable Compounding SolutionWood Plastic Composites
Tandem series specifications
Four sizes. Values are given as twin screw / single screw. The last column shows lines we have delivered.
| Model | Diameter (mm) | Max. Speed (rpm) | L/D | Motor (kW) | Output (kg/h) | Delivered lines |
|---|---|---|---|---|---|---|
| SAT52-TDD150 | 51.4/150 | 600/90 | 32–64/8 | 110/55 | 200–400 | — |
| SAT65-TDD180 | 62.4/180 | 600/90 | 32–64/8 | 160/75 | 400–800 | Rigid PVC compounding500 kg/hRigid PVC two-stage line400–600 kg/h |
| SAT75-TDD200 | 71/200 | 600/90 | 32–64/8 | 250/90 | 600–1200 | Rigid PVC pelletizing, Serbia900 kg/hWood plastic compounding, Latvia700 kg/hPLA with starch, Indonesia500 kg/h |
| SAT95-TDD240 | 93/240 | 600/90 | 32–64/8 | 500/110 | 1500–2500 | Soft PVC for medical use, SAT95-TDD2202,000 kg/hRigid PVC compounding, SAT95-TDD2201,200–1,500 kg/h |
Output depends on the material and the formulation. Delivered lines are listed by the size of their twin screw; the single screw of each line is named on its project page.
Pelletizing behind a tandem line
Dry
Air cooling die face pelletizing
The pellet never meets water. Used on our rigid PVC and HFFR lines.
Air Cooling Die FaceWet
Water ring pelletizing
Used on the 2,000 kg/h soft PVC line for medical compounds.
Water Ring- 01FeedingVolumetric or loss-in-weight
- 02ExtruderTwin, triple, tandem or single screw
- 03Melt filtrationScreen changer, melt pump
- 04PelletizingSix methods
- 05Dewatering and classifyingDryer, vibrating classifier
- 06Conveying and storageBlower, silo
- 07PackingBags or jumbo bags
Control system: one recipe and one start and stop sequence for all stationsControl system
Projects
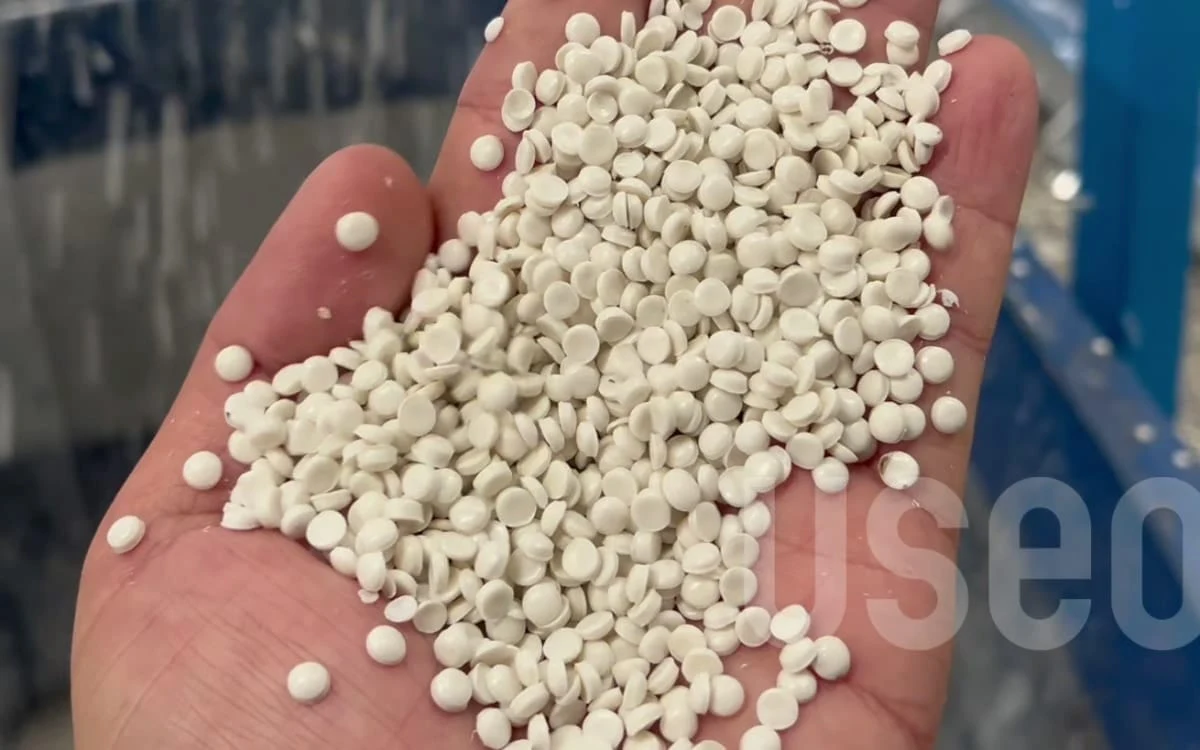 SAT65 + TDD180
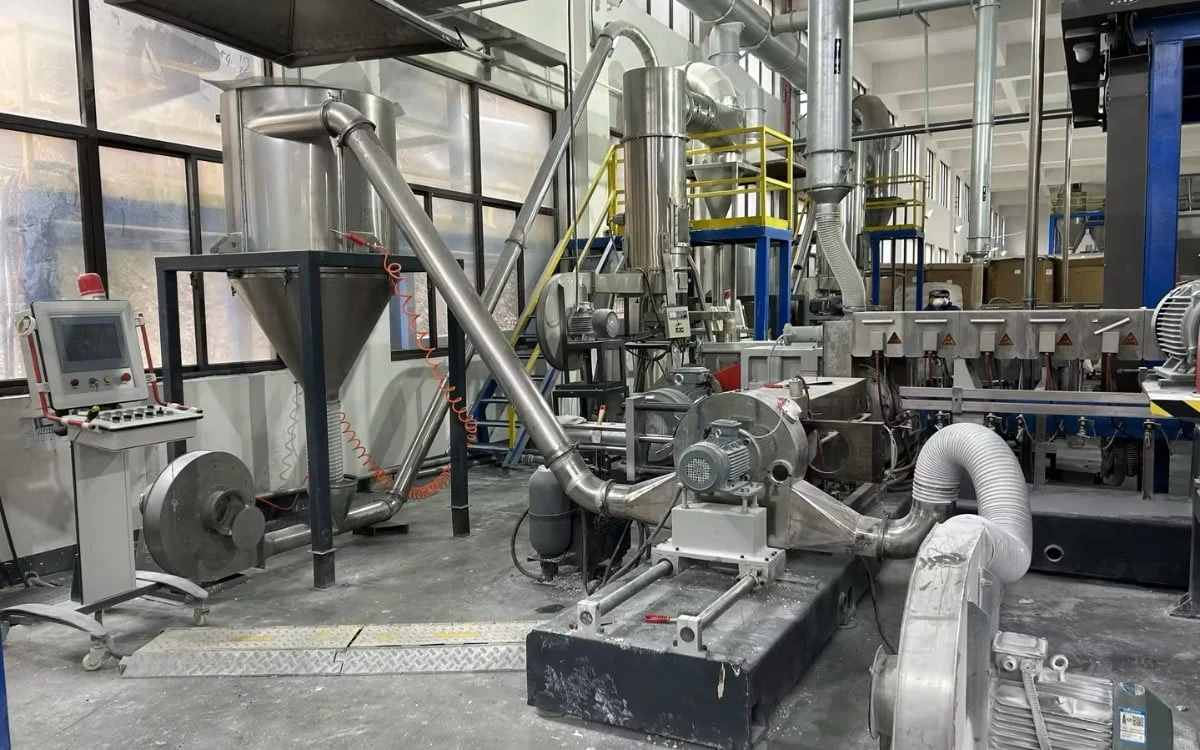 SAT75 + TDD180
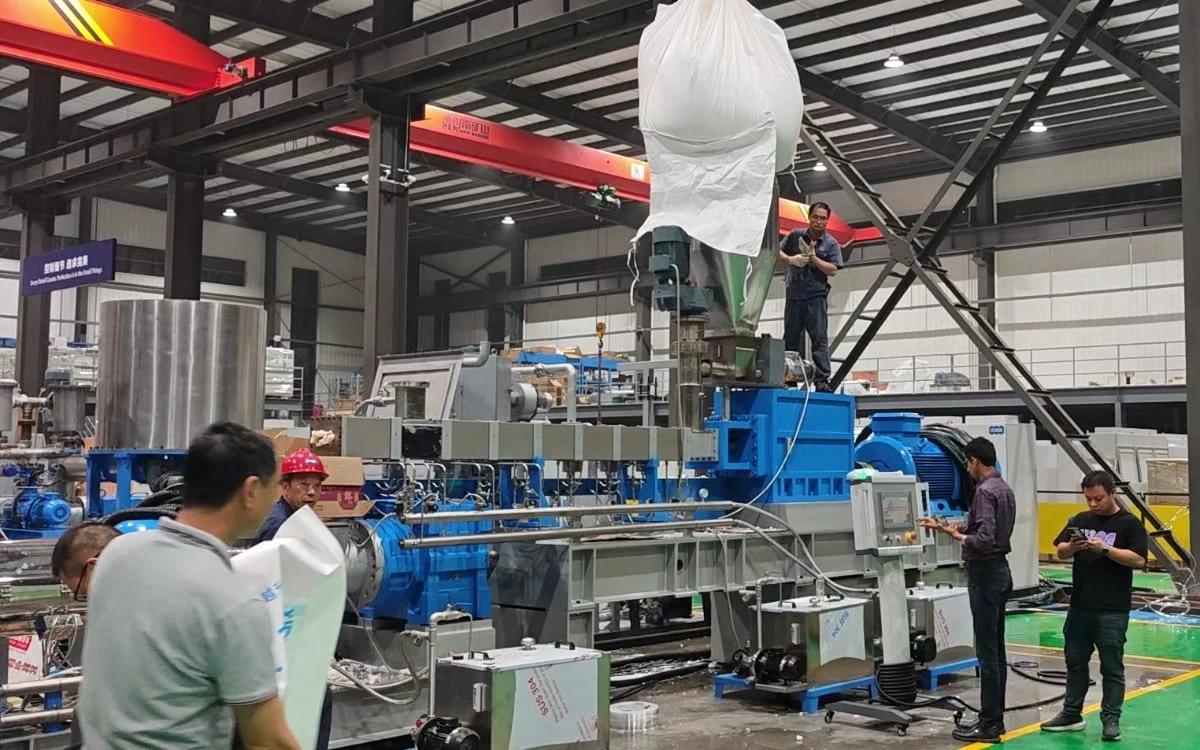 SAT95-TDD220
Get a quote
Tell us the compound and why it is sensitive: shear, temperature or water. We check whether a tandem line is needed and size both stages.
- 01Compound: PVC, HFFR, WPC, EVA, XLPE …
- 02Upstream mixing (mixer or kneader) and target output
- 03Tandem size, pelletizing method, quotation

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.