PP / PS / PLA / PBAT / PHA Sheet Extrusion Line
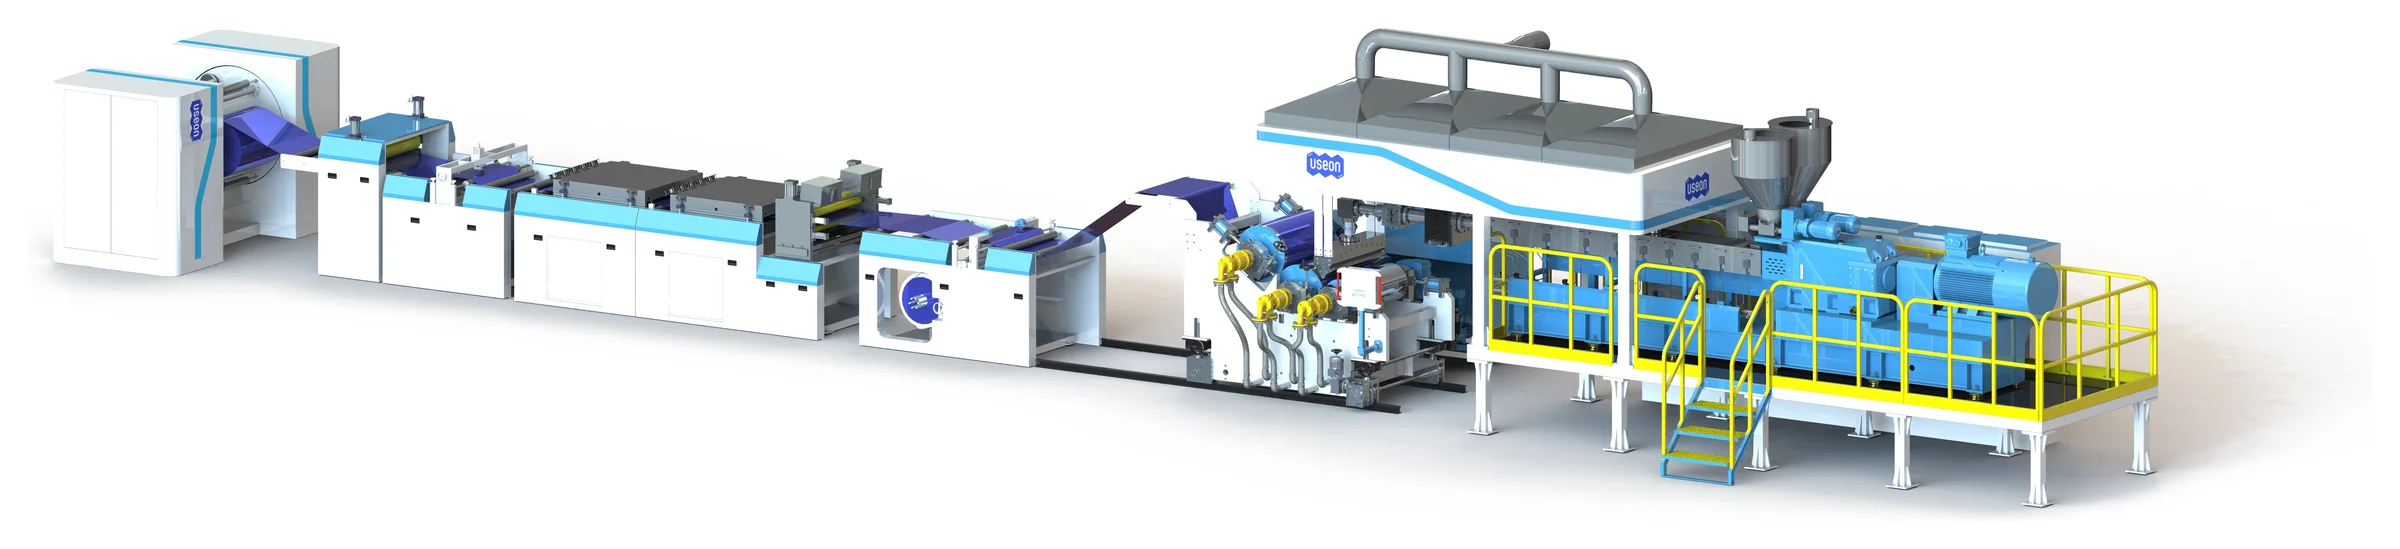
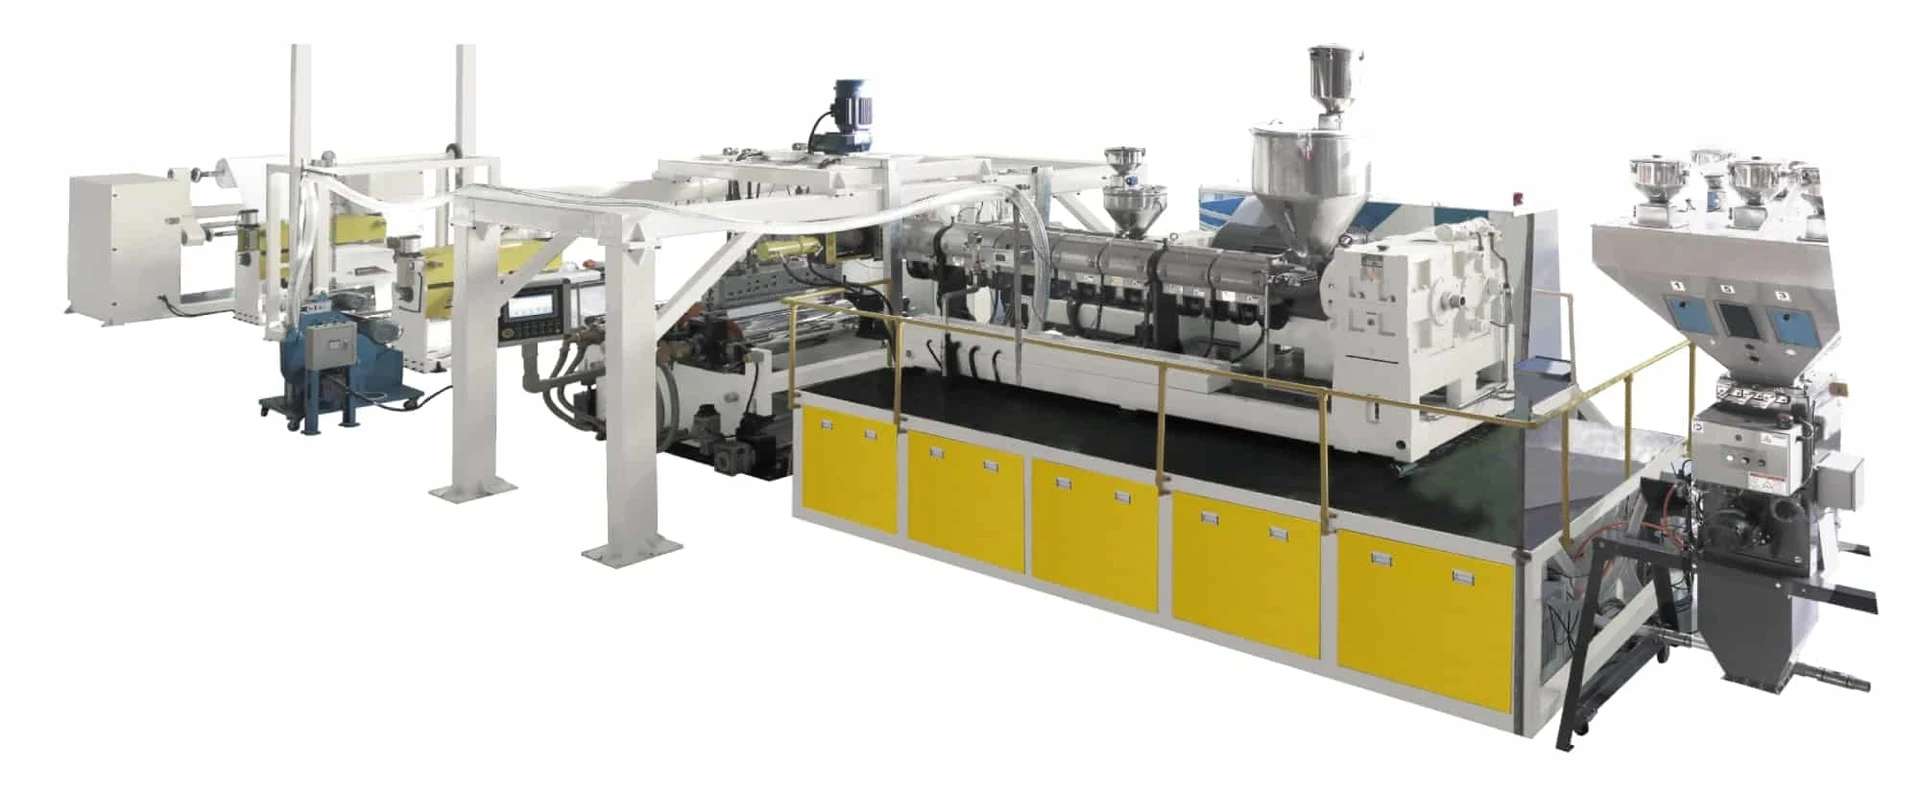
Sheet extrusion lines for PP, PS and HIPS, and for the biodegradable PLA, PBAT and PHA. Standard configurations are single-layer and 3-layer co-extrusion, with fully customizable multi-layer co-extrusion lines to match the application.
- PP
- PS
- HIPS
- PLA
- PBAT
- PHA
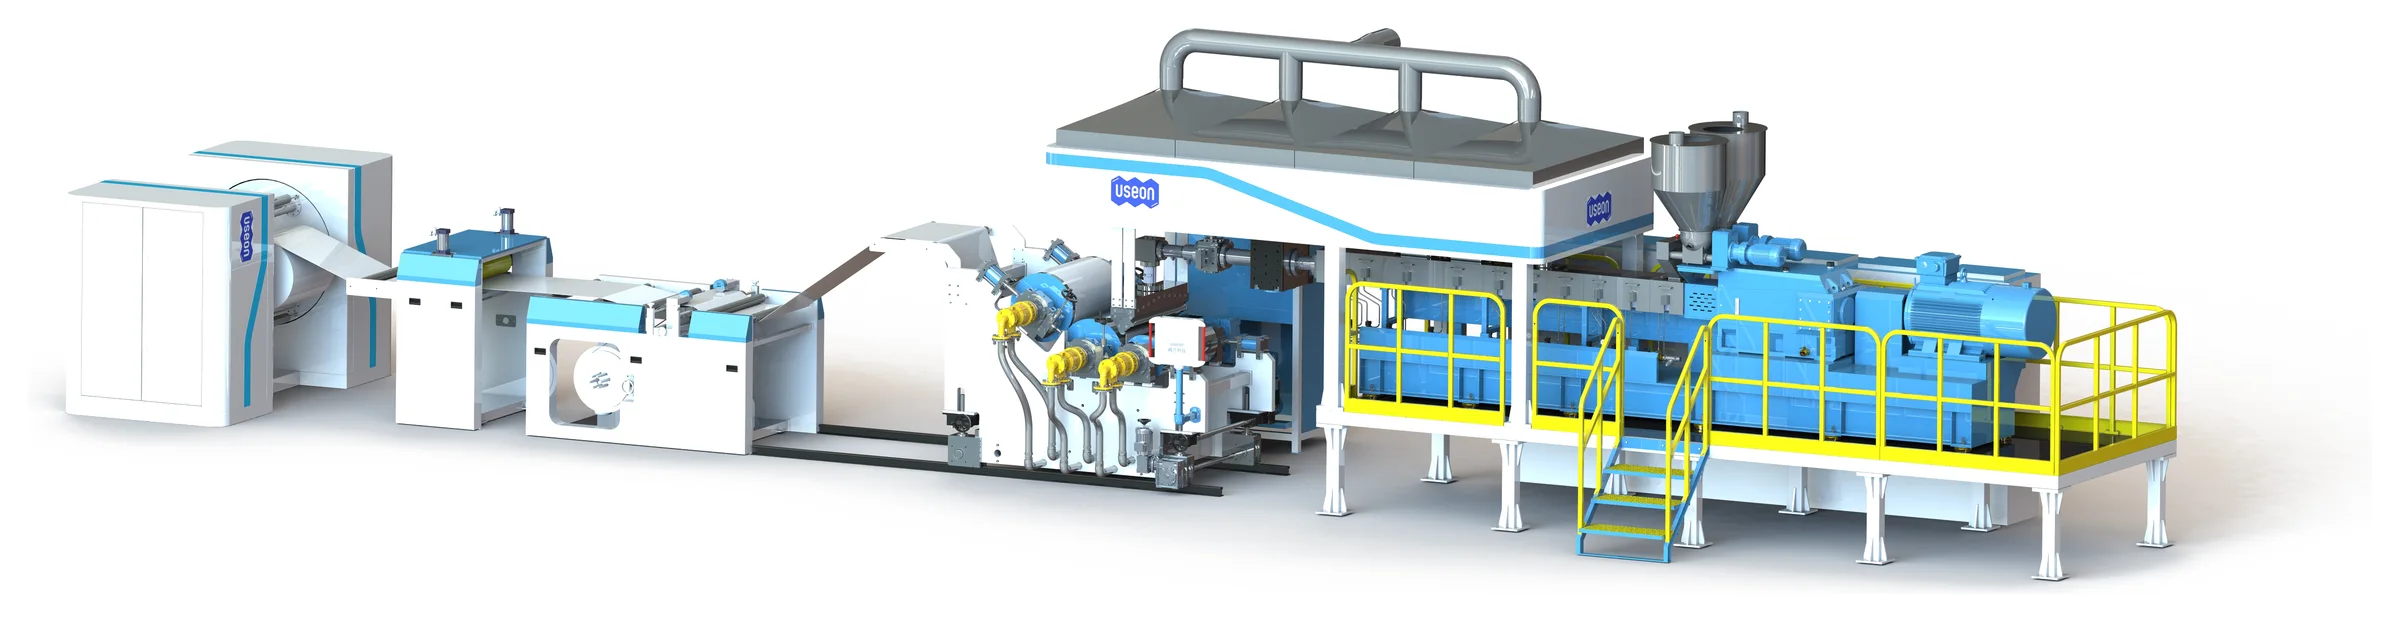
- Sheet thickness
- 0.15–3mm
- Sheet width
- 600–3,000mm
- Throughput, single and twin screw lines
- 350–1,500kg/h
- Sheet thickness tolerance
- ± 0.005mm
Five kinds of sheet from one line design
The lines are highly versatile and designed to meet diverse production needs.
| Sheet | Variants | Used for |
|---|---|---|
| Thermoforming & packaging | Premium thermoforming sheets | Food packaging, thermoformed or vacuum formed; anti-static electronic component trays |
| Blister packaging | Single-layer, bi-color co-extruded, ultra-high-clarity transparent | Thermoforming and blister packaging industries |
| Stationery & office supplies | Highly transparent, frosted / matte with fine or coarse texture, bi-color | PP stationery sheets |
| Highly filled sheet | PP compounded with high percentages of calcium carbonate (CaCO₃) or talcum powder | Rigid food containers and lunch boxes |
| Bio-based eco-sheet | PP compounded with natural fillers such as corn starch or bamboo powder | Eco-friendly applications |
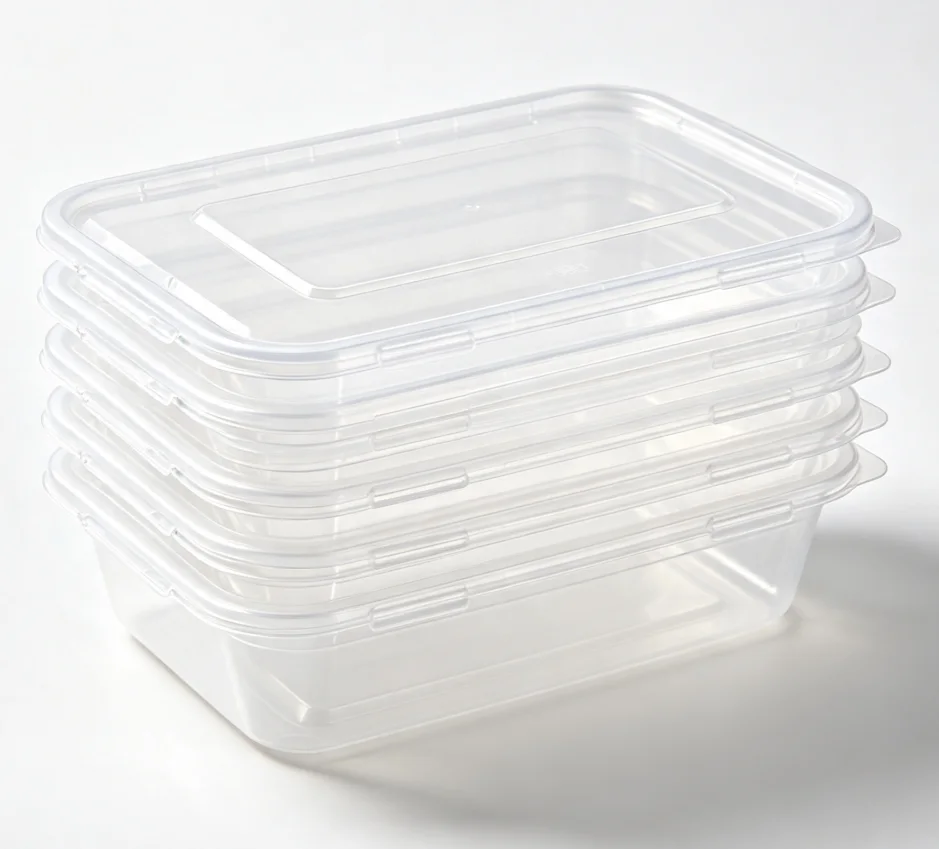
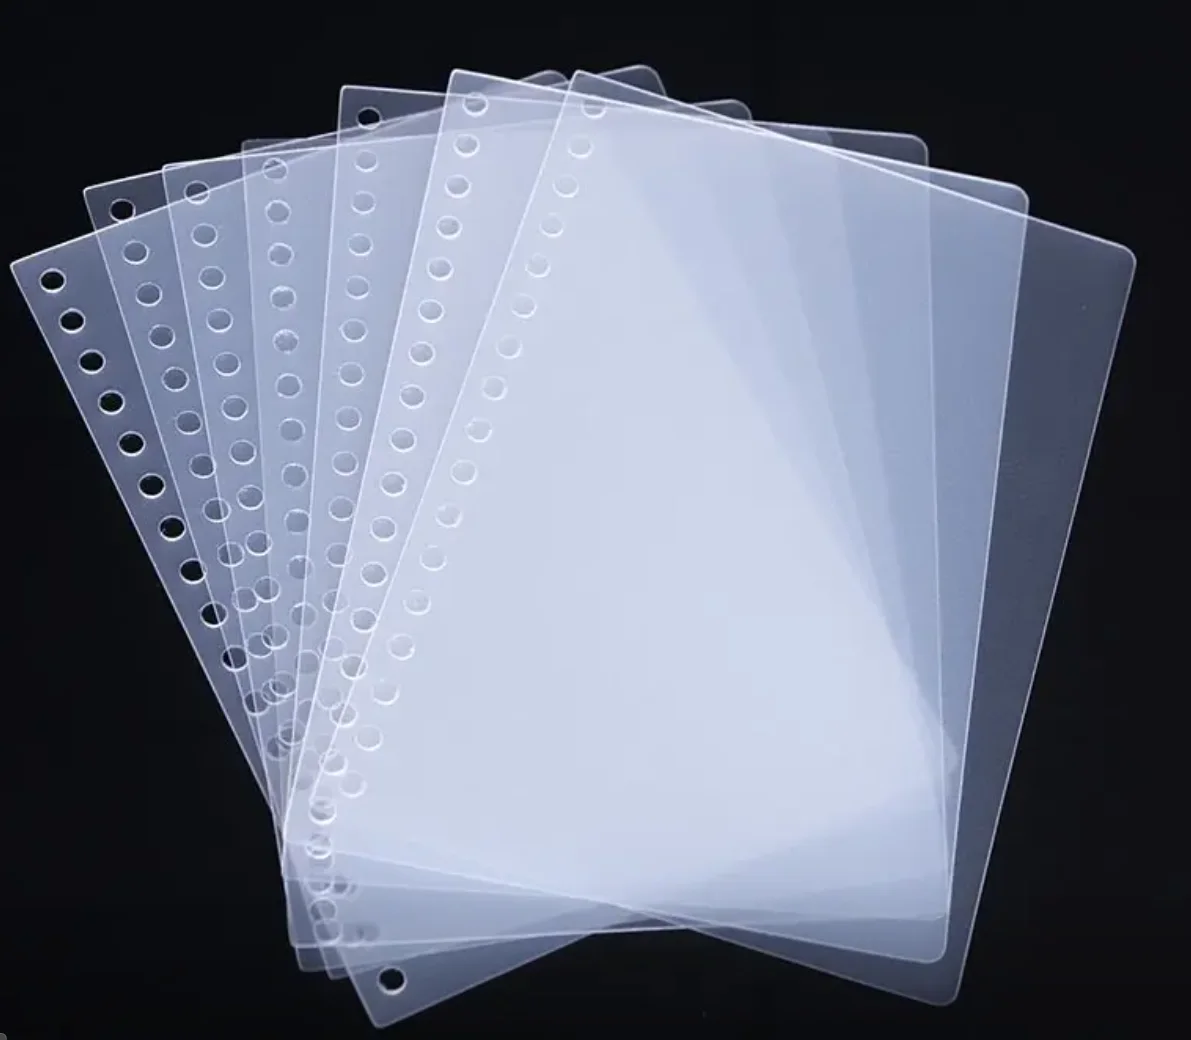
PP sheet
Light weight, good heat resistance, high mechanical strength, excellent chemical stability and electrical insulation. After thermoforming it becomes beverage cups and food boxes.
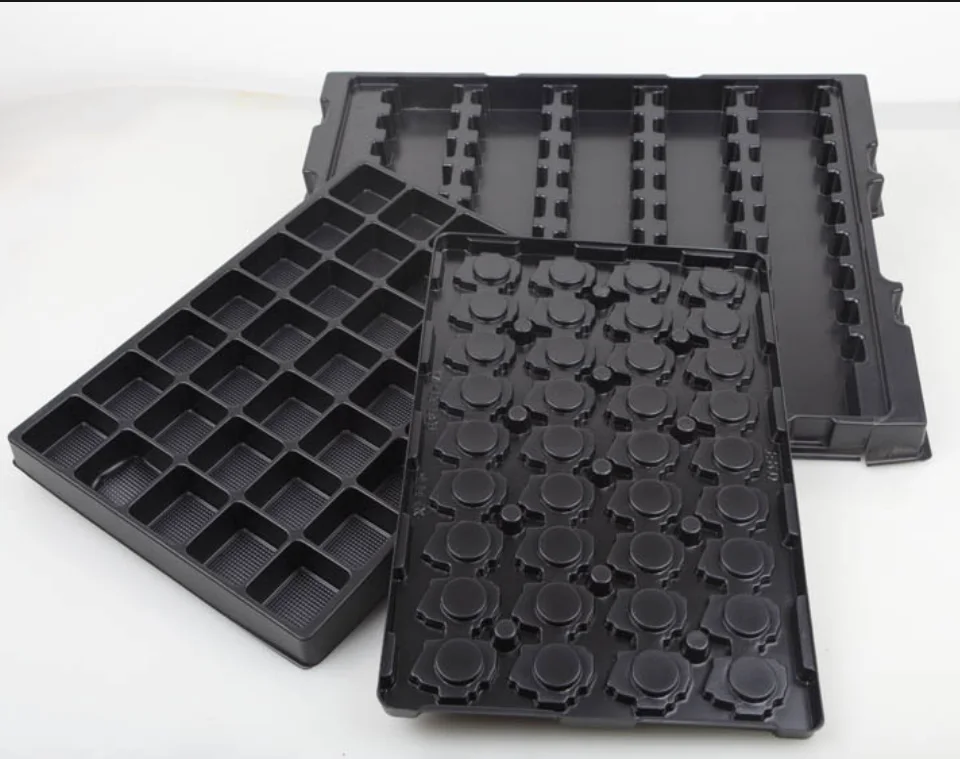
PS sheet
Excellent thermoforming performance and good hardness; easy to colour; low static electricity generation. Widely used in the blister packaging of medicine, food, toys, electronics and clothing.
Twin screw or single screw
Both extruder types feed the same die, calender and winder. All lines: sheet thickness 0.15–3 mm, width 600–3,000 mm.
Twin screw extrusion line
For formulas that are compounded in the line: fillers, talc, starch or bamboo powder are fed and dispersed in the extruder, without a separate pelletizing step. Compounding in line makes a recipe change more flexible and the masterbatch preparation unnecessary.
Single screw extrusion line
For simple formulations: resin with a small added quantity of masterbatch or additives, premixed and fed into the extruder.
Twin screw extrusion line · SAT series
| Extruder | Motor power | Max. output |
|---|---|---|
| Single-layer line | ||
| SAT75 | 160 kW | 500–700 kg/h |
| SAT85 | 220 kW | 600–800 kg/h |
| SAT95 | 355 kW | 800–1,200 kg/h |
| Co-extrusion line | ||
| SAT75 / SAT52 | 160 kW / 45 kW | 500–700 kg/h |
| SAT85 / SAT52 | 220 kW / 45 kW | 700–900 kg/h |
| SAT95 / SAT65 | 355 kW / 75 kW | 900–1,500 kg/h |
Single screw extrusion line · TDD series
| Extruder | Motor power | Max. output |
|---|---|---|
| Single-layer line | ||
| TDD120 | 132 kW | 350–450 kg/h |
| TDD130 | 160 kW | 500–600 kg/h |
| TDD150 | 200 kW | 600–800 kg/h |
| Co-extrusion line | ||
| TDD120 / TDD65 | 132 kW / 45 kW | 350–450 kg/h |
| TDD130 / TDD75 | 160 kW / 55 kW | 500–600 kg/h |
| TDD150 / TDD90 | 200 kW / 75 kW | 600–800 kg/h |
Tailored extrusion solutions
Processing and screw configurations engineered for the raw material format and its processing requirements.
Energy-efficient drive
Permanent magnet synchronous motor, USEON high-torque gearbox and a safety coupling that disengages on torque overload.
Precision co-extrusion
A premium feedblock and extrusion dies: stable melt flow, uniform layer distribution, precise control over individual layer ratios.
Stable extrusion pressure
Servo drive and dual closed-loop control, with simplified operation.
Biodegradable sheet: PLA, PBAT and PHA on the same line
Fully biodegradable sheet for thermoformed products.
Biodegradable materials
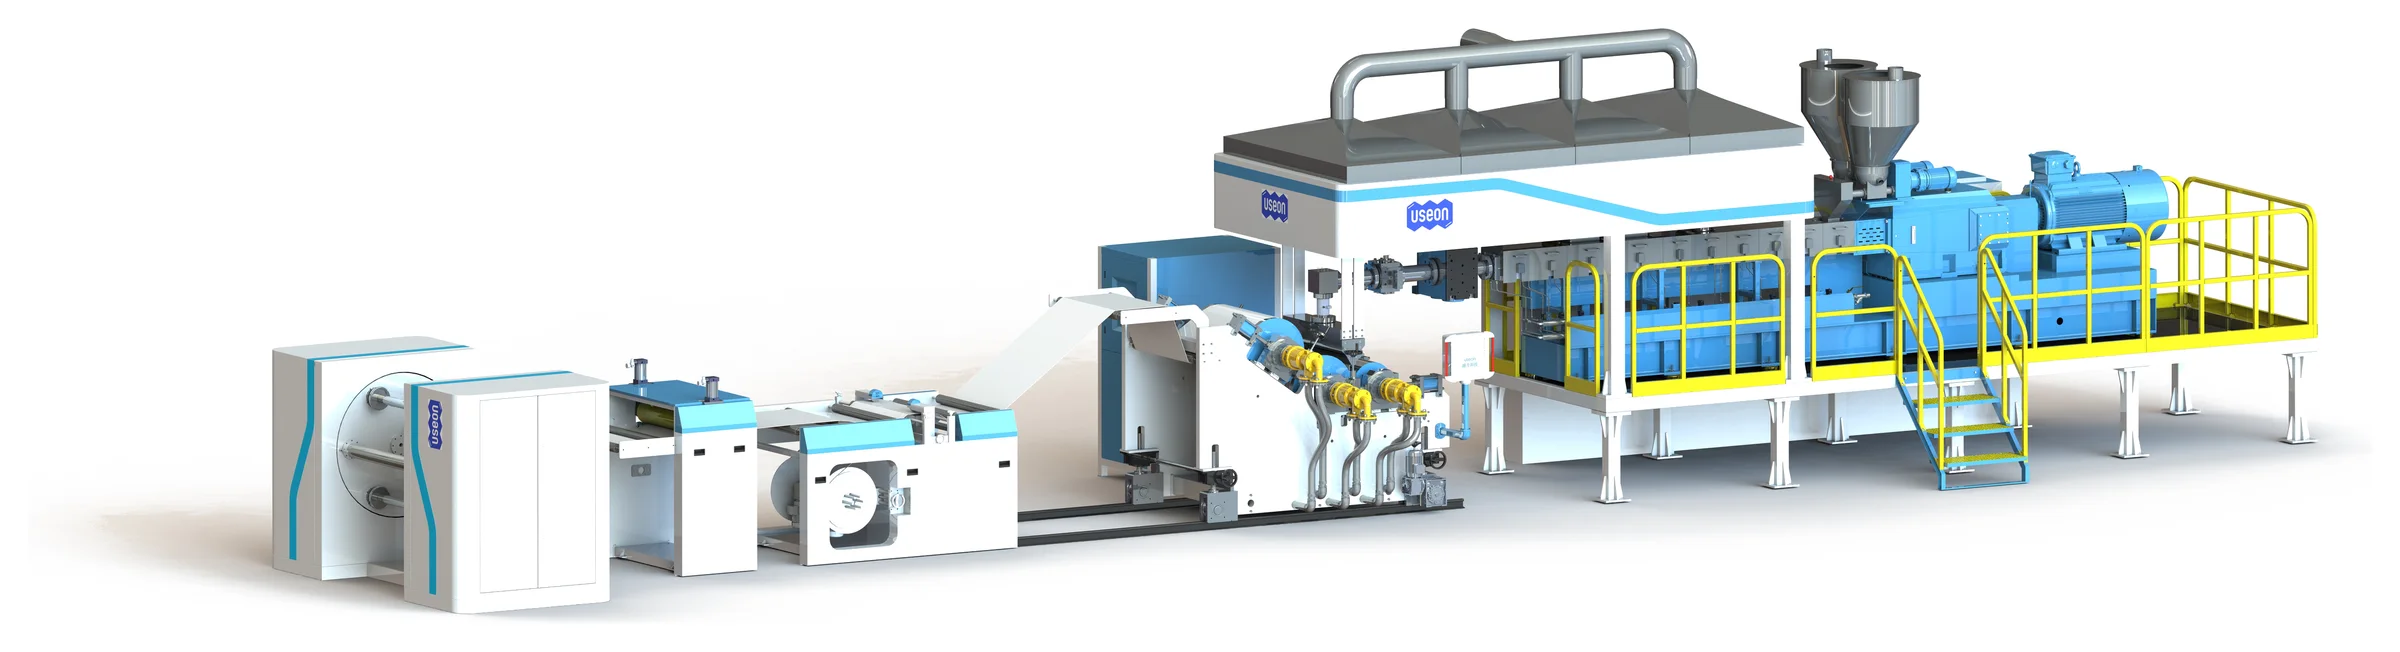
The processing equipment is very similar to the PP / PS line: the same extruder series, die, calender and winder.
High-torque extruder
Low temperature and low speed operation.
High-vacuum degassing system
Superior colour retention and minimal IV drop; a highly stable vacuum, consistently maintained at −0.1 MPa, minimises polymer degradation.
Highly optimised screw configuration
Optimal plasticising intensity and enhanced molecular weight distribution.
The compound before the sheet: PLA, PBAT and starch blends.
The line, station by station
An integrated melt-delivery system and a one-stop downstream, for low pulsation, maximum yield rates and extended continuous runtimes.
| Station | Equipment | What it does |
|---|---|---|
| Feeding | High-fill-ratio feeding system | Maximised throughput rates. |
| ExtrusionCo-extrusion: one more extruder for the skin layers | SAT twin screw or TDD single screw extruderHigh-vacuum degassing | Low temperature and low speed operation; venting and devolatilization by a redesigned barrel and screw geometry. |
| Melt delivery | Continuous screen changerMelt pumpFeedblockSheet die | Nonstop melt filtration; the melt pump balances flow rates and pressure differentials for surge-free extrusion. |
| Forming | L-type 3-roller calender | The first two rollers are horizontal, so the die extrudes vertically: effortless commissioning and rapid start-up. |
| DownstreamFully automatic winders and roll unloaders for hands-free production | Cooling conveyorEdge trimming unitEdge winderTake-offWinder | Trims the sheet to width and winds it into rolls. |
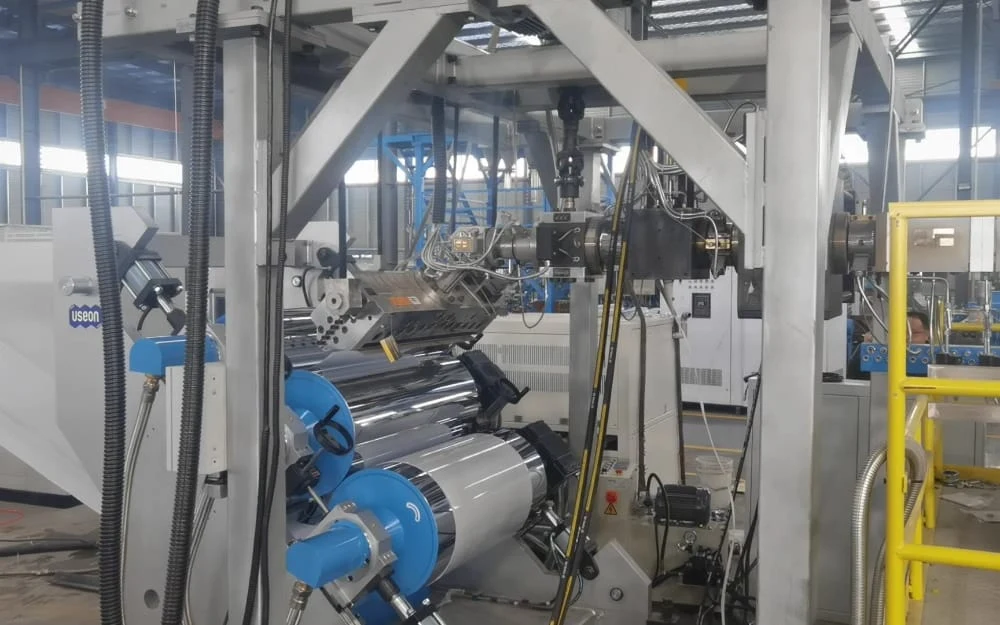
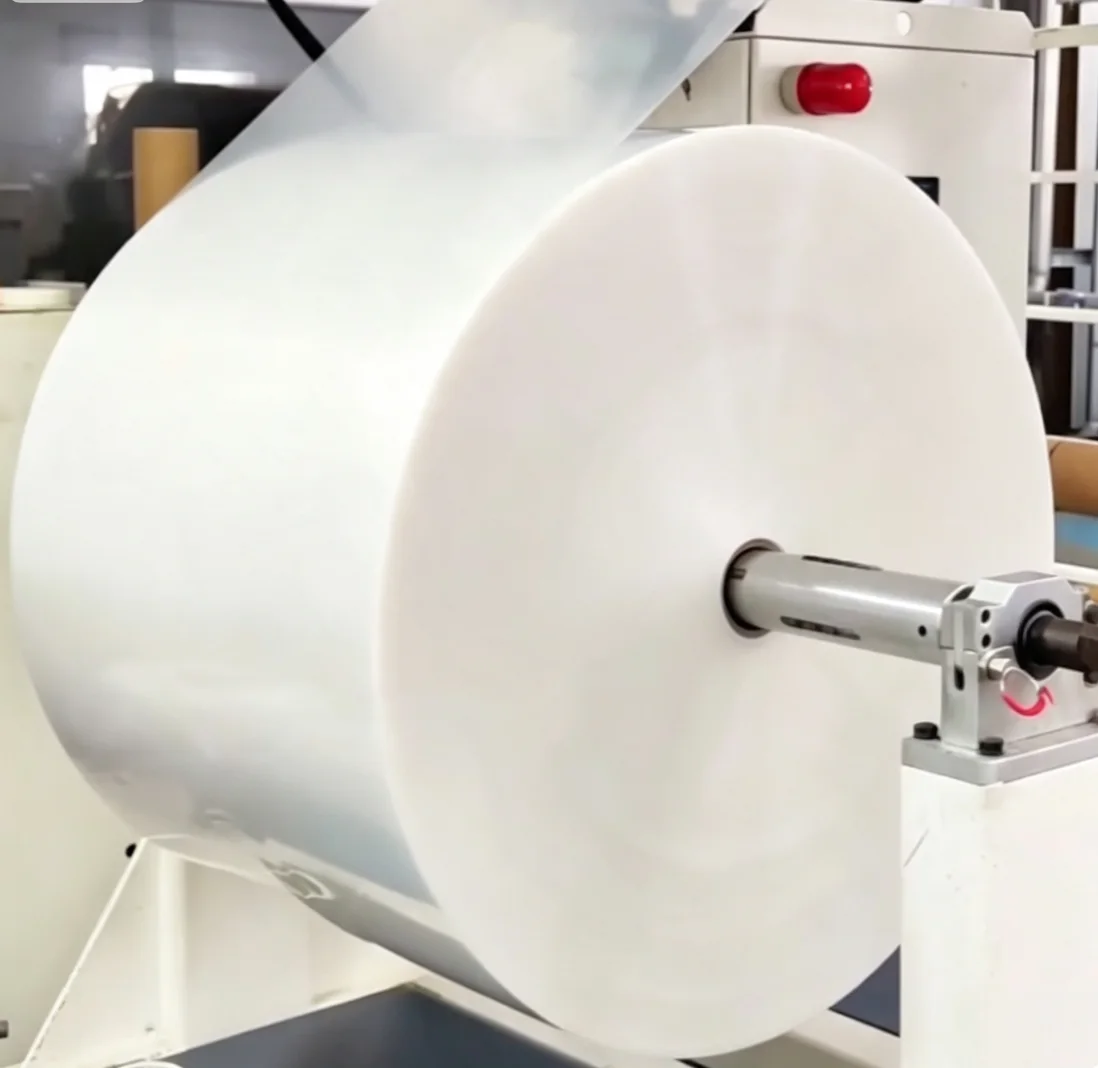
High-precision 3-roller calender
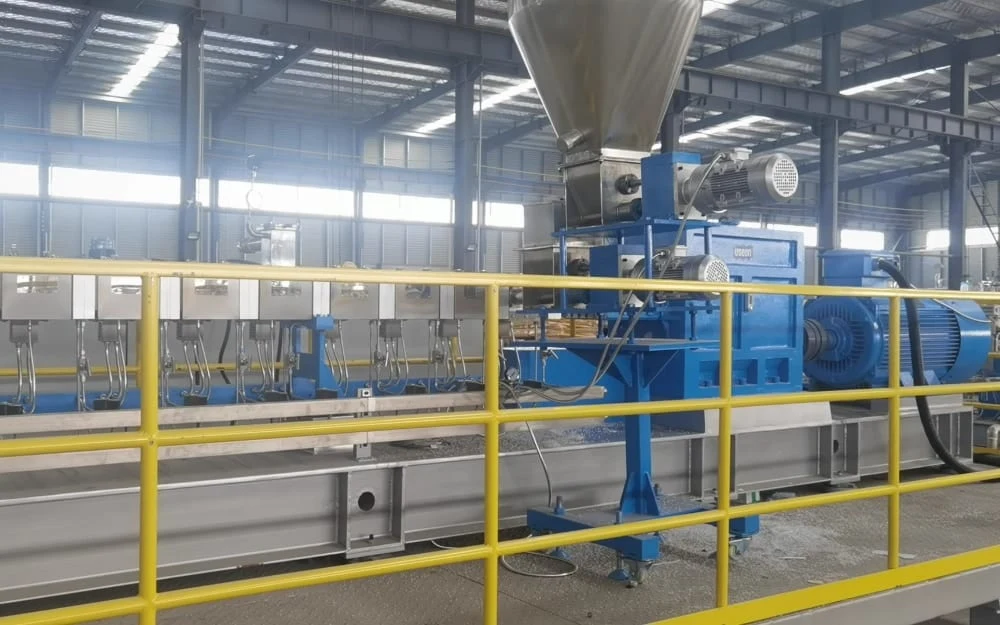
Where the surface and the thickness tolerance of the sheet are made.
< 0.005 mm
Roller runout in operation
Ra 0.015 μm
Roller surface, hard-chrome plated and polished
15 mm
Thin-wall roller shell
Up to 10 t
Clamping force per hydraulic cylinder
- Thin-wall rollers: cooling efficiency 15% to 30% higher than traditional thick-wall designs
- 42CrMo alloy steel shell: surface strength and hardness against scratching or denting by high-stiffness sheets
- Monoblock spiral-groove core, shrink-fitted into the shell: no internal gaps, no deflection under calendering pressure
- Premium bearings, shrink-fitted for a zero-clearance fit between bearing and shaft
- Servo motors on all three rollers, with zero-backlash gearboxes: no chatter marks or ripples
- Hydraulic clamping with zero pressure fluctuation during production, for flatness and consistency
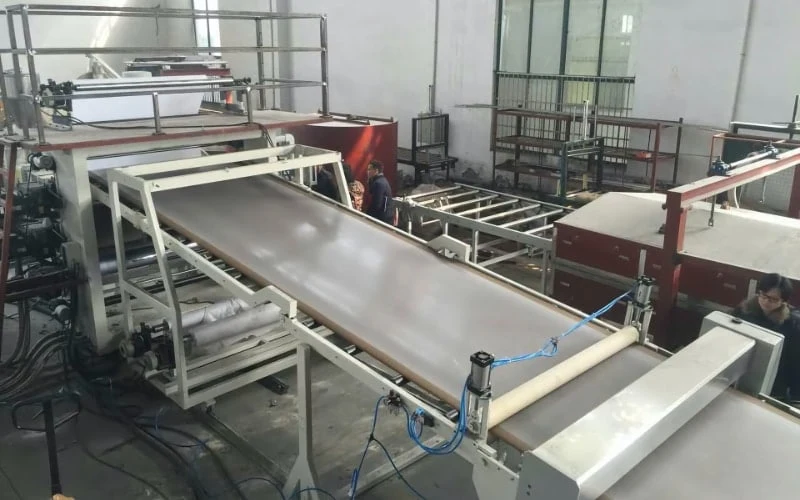
PP sheet lines delivered
All three compound the filler in the twin screw extruder and extrude the sheet directly.
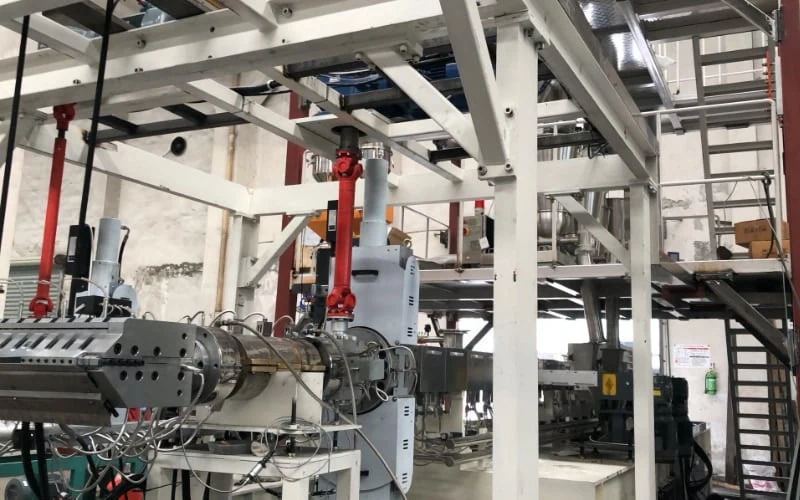 USA
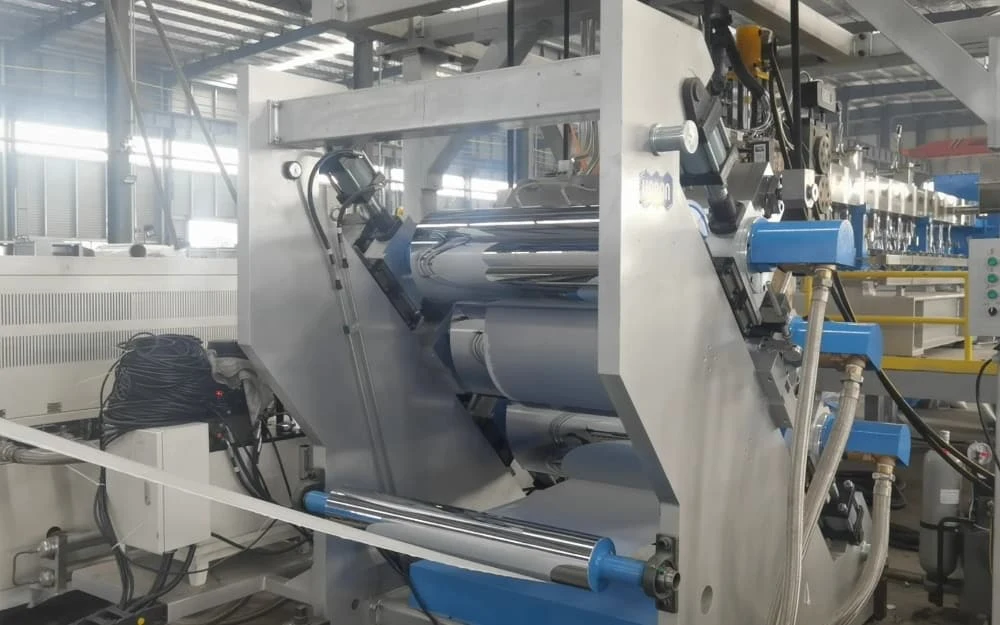 China
 Latvia
Related lines
 Sheet Extrusion
Why compounding and sheet extrusion run in one step.
 PET Recycling
PET Sheet Extrusion Line
The sister line for APET, RPET, CPET and PETG, without pre-drying.
 Sheet Extrusion
PP/PE/PS/EVA/EVOH Barrier Sheet Extrusion Line
Multi-layer sheet with a barrier layer.
 Foam Extrusion
PET/PS/PLA/PC Microfoam Sheet Lines
PLA sheet with a foamed core, for lighter trays.
Get a quote
Tell us the sheet you sell and the formula behind it. We propose twin or single screw, the number of layers and the line width.
- 01Material and formula: PP, PS, HIPS, PLA, PBAT or PHA; filler type and percentage
- 02Sheet: thickness range, width, layer structure, output per hour
- 03Extruder type, line configuration and quotation
Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.