Single Screw Extruder
The TDD series runs from 20 to 500 mm screw diameter, with smooth or grooved feeding barrels and an L/D from 8 to 32. It processes melt with venting or vacuum for recycling and product extrusion, and it is the second stage of our tandem lines.
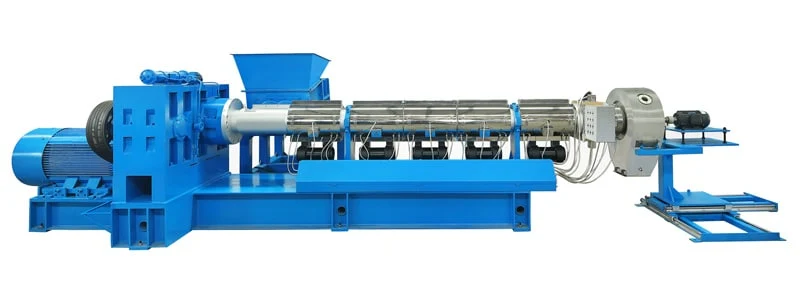
- Screw diameter, TDD20 to TDD500
- 20–500mm
- Length of screw
- 8–32L/D
- Output, by size and material
- 5–7,000kg/h
Four jobs for a single screw
Recycling and direct extrusion
Polyolefin and engineering plastic recycling; direct extrusion of films, sheet, plates, pipes and profiles in PET, PA, PBT, ABS and PC, with venting or vacuum.
Cooling and pressure in a tandem line
Behind a twin screw extruder, the lower-speed single screw provides cooling and pressure accumulation, for PVC, HFFR and wood plastic compounds.
Rubber and elastomer lumps
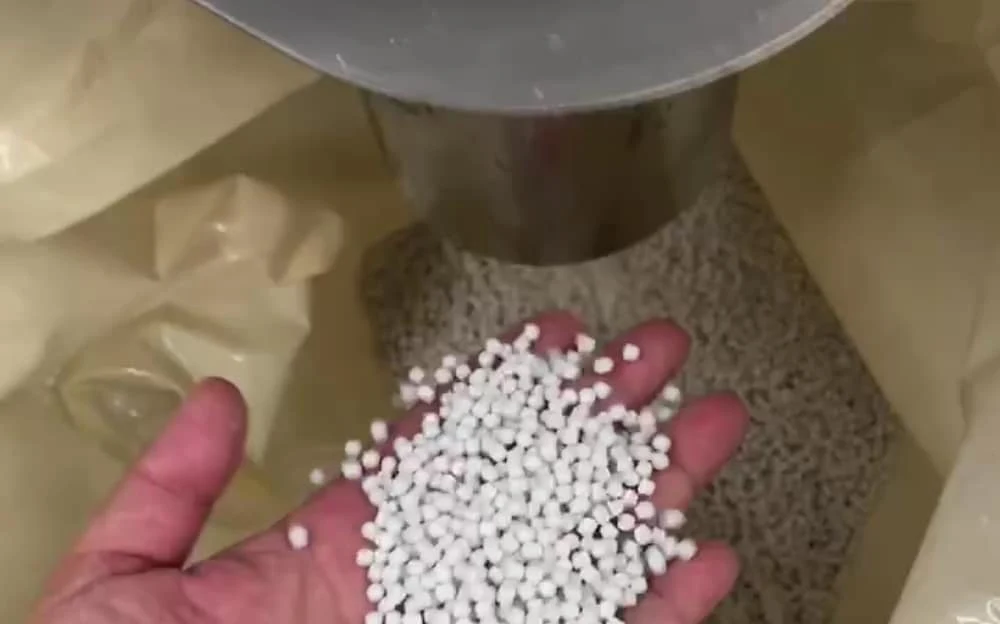
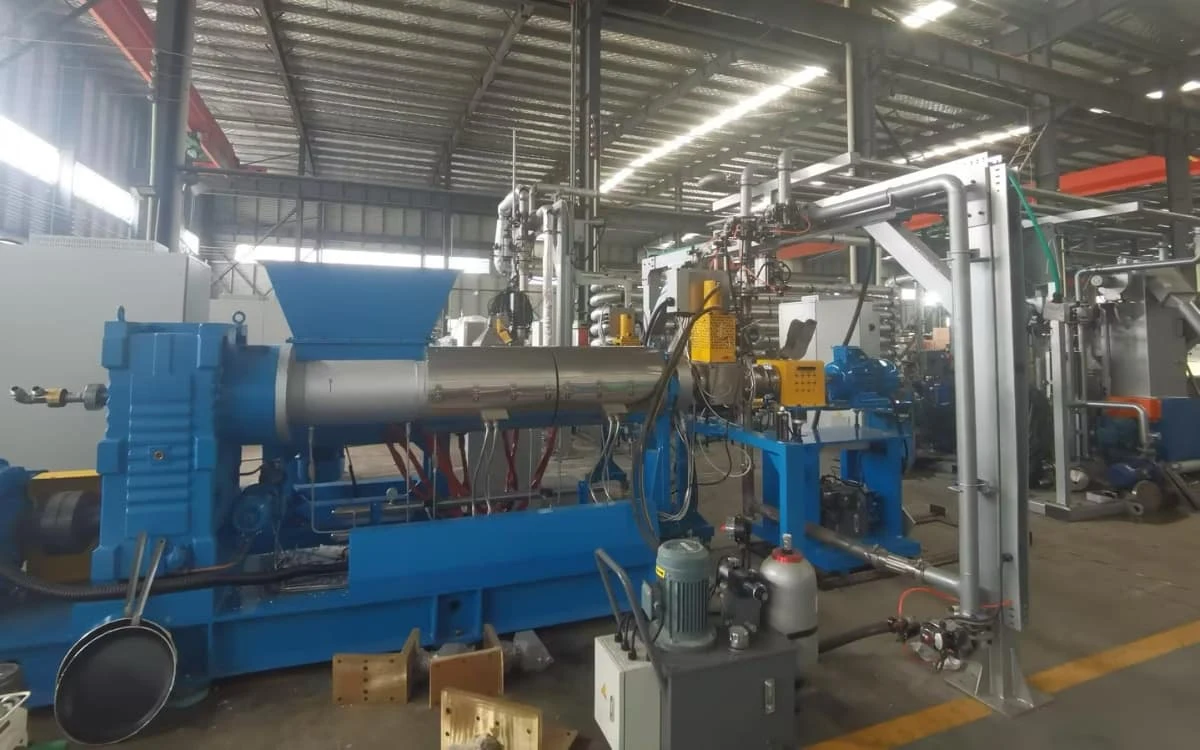
A conical force feeder takes EPDM, SR or TPU lumps into the TDD; the melt goes to an underwater pelletizer. TDD120 at 300 kg/h, TDD220 at 1,000 kg/h.
Rotational moulding compounds
A compounding line for rotational moulding, built on a TDD150 at 1,000 kg/h.
Where the TDD works with another extruder
MachineTandem Extrusion System SolutionCO₂ foam XPS line: the TDD as cooling extruder
Twin screw
The standard for compounding. Usually the more economical choice.
- Sizes
- SAT, U+, EC, TDY, Lab
Triple screw
When feeding volume limits the output: light powders, very high filler loading.
- Sizes
- SAT-T35 to SAT-T95
Tandem: twin + single
Mixing in the twin screw, cooling and pressure build-up in a slow single screw.
- Sizes
- SAT52-TDD150 to SAT95-TDD240
This page
Single screw
Melt extrusion with venting, force-fed lumps, or the second stage of a tandem.
- Sizes
- TDD20 to TDD500
Design of the TDD series
The newly designed high efficiency TDD series focuses on energy saving, more accurate process control and higher output.
- Smooth or grooved feeding barrels
- Screw length from L/D 8 to L/D 32
- Superior plastication
- Better mixing effect
- Precise and accurate process control
- Wider application, including recycling, compounding, pipe extrusion and sheet / film extrusion
TDD series specifications
Ten sizes. The last column shows lines we have delivered on each size.
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | Length of Screw (L/D) | Output (kg/h) | Delivered lines |
|---|---|---|---|---|---|---|
| TDD20 | 20 | 93 | 3 | 8–32 | 5–10 | — |
| TDD65 | 65 | 93 | 30 | 8–32 | 80–100 | — |
| TDD120 | 120 | 93 | 160 | 8–32 | 500–600 | EPDM / SR rubber compounding300 kg/h |
| TDD150 | 150 | 93 | 200 | 8–32 | 700–900 | Rotational moulding compounding, UK1,000 kg/h |
| TDD180 | 180 | 93 | 280 | 8–32 | 800–1300 | HFFR cable compound, behind SAT75700 kg/hRigid PVC, behind SAT65500 kg/h |
| TDD200 | 200 | 93 | 355 | 8–32 | 1200–1500 | Rigid PVC, behind SAT75, Serbia900 kg/hWood plastic compound, behind SAT75, Latvia700 kg/h |
| TDD240 | 240 | 93 | 455 | 8–32 | 1500–2000 | — |
| TDD300 | 300 | 70 | 600 | 8–32 | 2500–3000 | — |
| TDD400 | 400 | 70 | 1000 | 8–32 | 4000–5000 | — |
| TDD500 | 500 | 70 | 1300 | 8–32 | 5000–7000 | — |
Motor and output are for the single screw as a stand-alone extruder. As the second stage of a tandem line the same size runs at L/D 8 with a smaller motor.
 TDD120
 TDD220
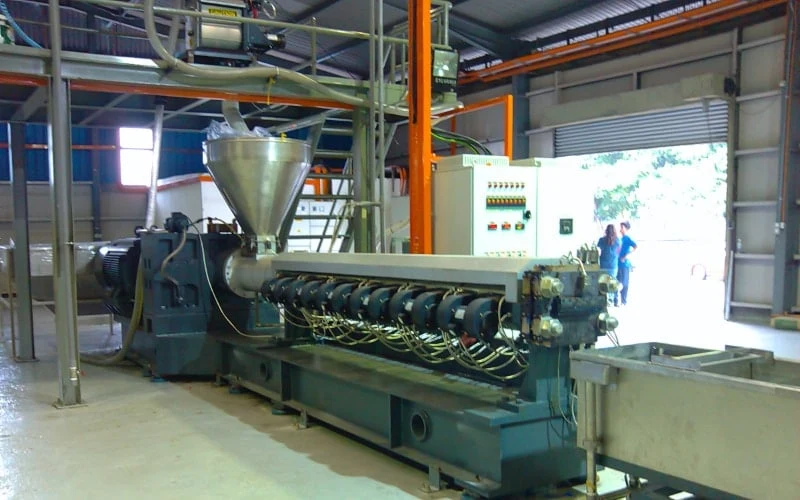 TDD150
Get a quote
Tell us the material, its form and the task: melt extrusion, a second stage behind a twin screw, or force-fed lumps. We size the TDD and its feeding.
- 01Material and form: pellets, flakes, melt or lumps
- 02Target output and what follows: die, pelletizer or sheet line
- 03TDD size, L/D, feeding and quotation
Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.