
3D Printer Filament Extrusion Line
Single screw lines that turn ABS, PLA, PET, HIPS or PVA, with colour masterbatch, into 1.75 mm or 3 mm filament: extrusion, water-bath forming and cooling, laser diameter gauging, haul-off and automatic winding.
- 1.75 mm or 3 mm
- Laser diameter gauge
- Automatic winding
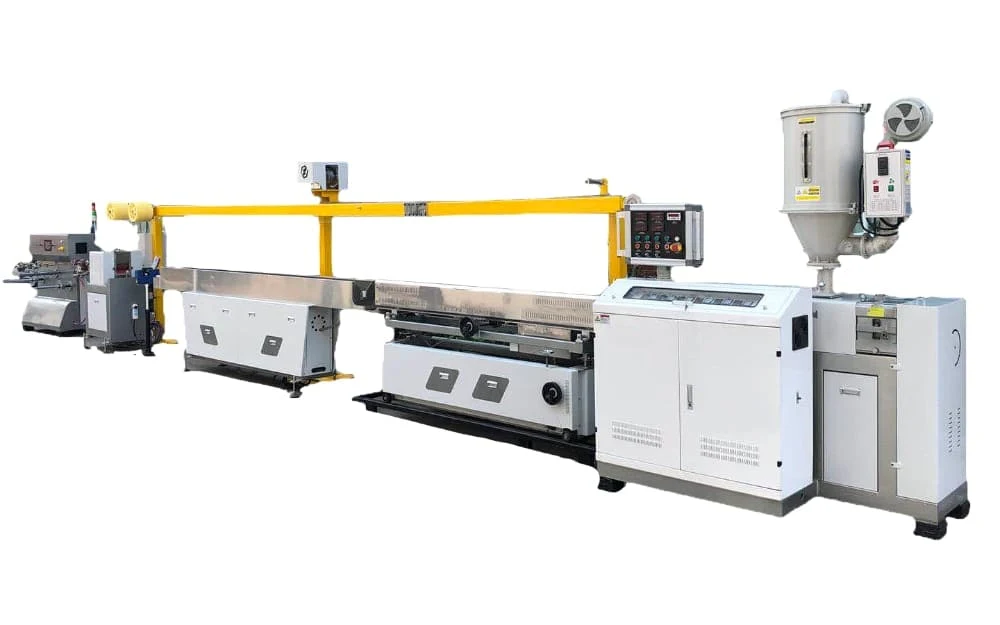
Ten stations, mixer to spool
The extruder makes the melt; everything after the die is about holding the diameter. The filament is formed in hot water, cooled, measured by laser and wound automatically.
Three line sizes
From a few kilograms an hour for trials to 30 kg/h for production. Each size makes either standard diameter.
| Model | Screw Dia. mm | Motor (kW) | Strand Dia. (mm) | Output (kg/h) |
|---|---|---|---|---|
| TDD-25 | 25 | 1.5 | 1.75 or 3 | 2–4 |
| TDD-30 | 30 | 7.5 | 1.75 or 3 | 5–10 |
| TDD-45 | 45 | 15 | 1.75 or 3 | 15–30 |
Five materials, five ways to handle them
The line runs ABS, PLA, PET, HIPS and PVA, compounded with colour masterbatch. What the printer needs from each filament decides how you dry, cool and wind it.
| Material | What the printer user needs | On your filament line |
|---|---|---|
| PLA | Hardly shrinks, so large parts print even on open printers. Brittle, and softens above about 60 °C. For models, prototypes, boxes and gifts. | Dry before extrusion: moisture breaks PLA down in the melt and shows as bubbles and diameter swings. Keep winding tension even, because the filament snaps rather than stretches. |
| ABS | Tough and heat resistant, for parts that take knocks or sit in a hot car. Shrinks on cooling, so it warps or delaminates without an enclosure; print in a ventilated room. | Dry before extrusion. Cool gradually — warm forming tank, then the cooling tank — so the filament stays round and free of internal stress. |
| PET / PETG | Tough, low shrinkage, good layer adhesion. | Dry thoroughly before extrusion; PET picks up moisture and loses viscosity in the melt. |
| HIPS | Similar to ABS; also used as a dissolvable support for ABS prints. | Runs much like ABS. |
| PVA | Water-soluble support material. | Dissolves in water: it cannot go through the water tanks and needs dry cooling and sealed, dry packing. |
Filament diameter tolerance is what printer users notice first; the laser gauge after the cooling tank measures it continuously.
Upstream · Compounding
Compounding the material first
Filament with carbon fibre, powder additives or a custom colour starts as a compound. For a materials maker serving 3D printing, USEON built an Ex tb IIIC rated SAT65 twin screw line that compounds PLA, PETG and ABS with carbon fibre and powders.
- Materials
- PLA · PETG · ABS
- Additives
- Carbon fibre, powders
- Output
- 500–700 kg/h
- Extruder
- SAT65 · L/D 44
Explosion-proof SAT65 twin screw extruder for PLA/PETG/ABS compounding
Get a quote
Tell us the materials you will run, whether you buy compound or make it yourself, the filament diameter and tolerance you need, and the output. We will size the extruder and the forming, gauging and winding downstream.
- 01Material & colour
- 02Diameter, tolerance & output
- 03Gauging & winding

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.