
Cable Compounding
Extrusion lines for every compound in a power or data cable: PE insulation and sheathing, crosslinkable XLPE for 10 kV and 35 kV, semiconductive screens, PVC and halogen-free flame retardant (HFFR) compounds.
- PE
- XLPE
- Semiconductive
- PVC
- HFFR
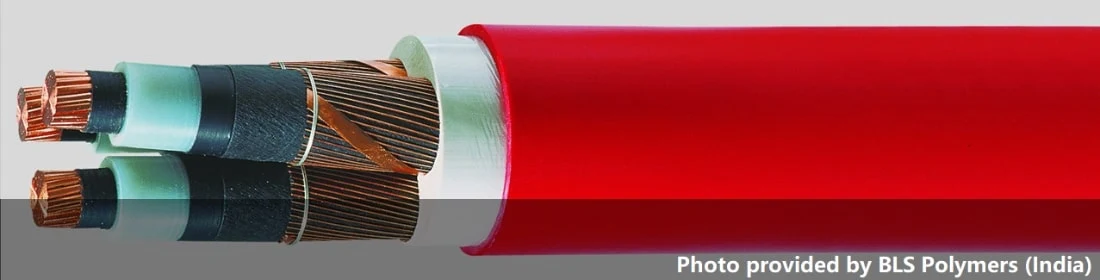
One cable, five compounds
Each layer of a cable is a different compound with a different process. Find your layer, then jump to its line.
1 · Conductor screen
Semiconductive compound: PE / EVA + carbon powder
2 · Insulation
PE, silane XLPE for 10 kV, peroxide XLPE for 35 kV, plasticised PVC, HFFR
3 · Insulation screen
Semiconductive compound, silane or peroxide type to match the insulation
4 · Metallic screen
Copper tape or wires, not a compound
5 · Sheath
PE sheathing compound, plasticised PVC, HFFR / LSZH
Six compounds, six routes
The formula decides the machine. Filled and heat-sensitive compounds go through a kneader or a second, single screw stage; clean polymer compounds go straight through a twin screw extruder.
| Compound | Basic formula | Process | Pelletizing | Output |
|---|---|---|---|---|
| PE insulation & sheathing | LDPE / LLDPE / MDPE / HDPE + 2–5% pigment or carbon black + additives | KneaderConical force feederSingle screwor mixer / loss-in-weight feeding → twin screw | Water ring | 250–1,100 kg/h |
| Silane XLPE · 10 kVA + B materials | A: PE + DCP + silane + anti-oxidant · B: PE + DBTL catalyst + anti-oxidant | Loss-in-weightTwin screw L/D 56B: low-torque twin screw, L/D 40 | On requestdryer, vacuum packing | 150–1,100 kg/h |
| Peroxide XLPE · 35 kV | LDPE + DCP + anti-oxidant | Loss-in-weightTwin screwSingle screwtwo stages to hold melt temperature | Ion-free cooling waterdryer, vacuum packing | 400–850 kg/h |
| Semiconductiveperoxide & silane | PE / EVA + carbon powder + DCP + anti-oxidant | KneaderConical force feederSingle screw | Air-cooling die face | 350–600 kg/h |
| PVC cable | PVC 60% + DOP 20% + calcined clay 10–20% + CaCO₃ 0–10% + heat stabiliser + additives | Twin screwSingle screwtandem | On request | 250–2,500 kg/h |
| HFFR / LSZH | PE 10% + EVA 30% + ATH 55% + additives 5% | KneaderForce feederTwin screwSingle screwor loss-in-weight → triple screw → single screw | Air-cooling die face | 250–1,000 kg/h |
Output ranges are the span of the model tables in each section below.
PE insulation and sheathing compound
Our PE compounds are based on polyethylene or its co-polymers, modified to the client's specification. Three types of process, all with water ring pelletizing.
- LDPE / LLDPE / MDPE / HDPE
- Pigment / carbon black2–5%
- Additives
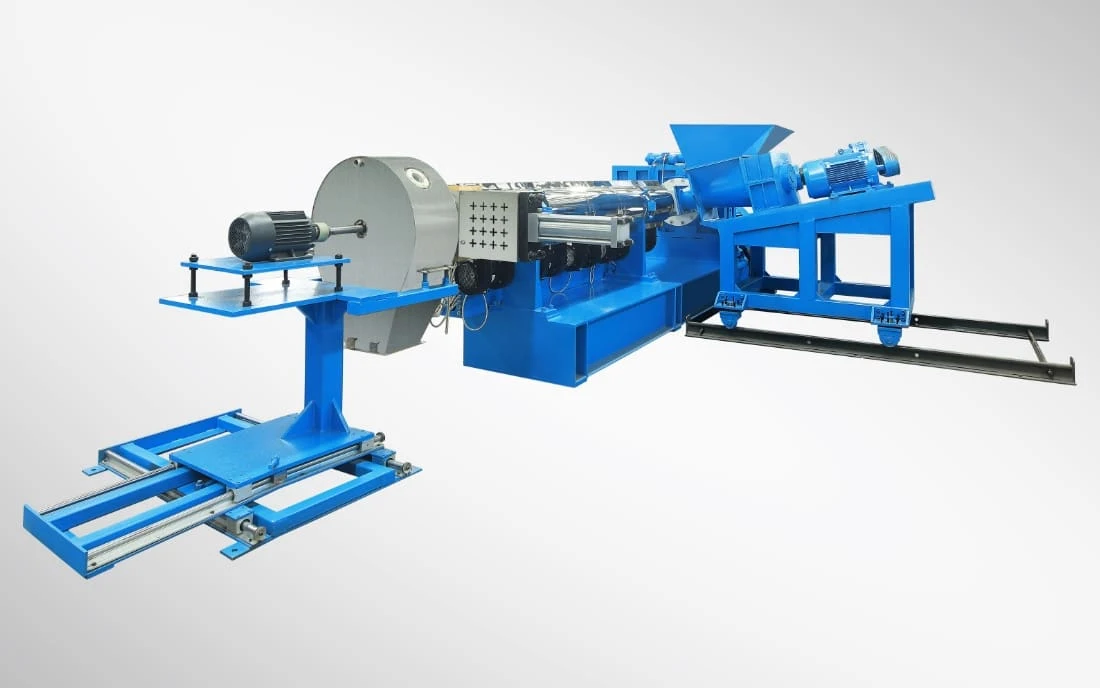
| Model | Kneader Volume (Liter) | Screw Diameter (mm) | Screw Speed (rpm) | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| K75-TDD180 | 75 | 180 | 75 | 110/90 | 600–700 |
| K110-TDD220 | 110 | 220 | 75 | 160/110 | 900–1100 |
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT52 | 51.4 | 800 | 110 | 40–44 | 250–350 |
| SAT65 | 62.4 | 800 | 160 | 40–44 | 450–600 |
| SAT75 | 71.4 | 800 | 250 | 40–44 | 700–900 |
Crosslinkable PE (XLPE) insulation
Crosslinking stops the PE molecules moving against each other under heat. An XLPE cable runs hotter, carries a higher current than its PVC equivalent, and has one of the best water resistances. Almost all XLPE cable compounds are based on LDPE.
90 °C
Maximum conductor temperature
140 °C
Depending on the standard
250 °C
Conductor short-circuit rating
10–380 kV
Medium voltage 10–50 kV AC, high voltage up to 380 kV AC, several hundred kV DC
Two materials, mixed 95 : 5 at the cable plant
Two compounds are made separately and mixed at the cable extruder.
Grafted PE
- LLDPE / LDPE 98% + DCP 0.1% + silane 1.5% + anti-oxidant
- Loss-in-weight feeding, high-torque extruder, long L/D
- Dryer and vacuum packing
Catalyst masterbatch
- LLDPE / LDPE 95.5% + DBTL 4% + anti-oxidant 0.5%
- Loss-in-weight feeding, low-torque extruder, L/D 40
95% A + 5% B go into the XLPE cable extruder.
One material, held below its reaction temperature
The melt temperature must be controlled very well so the DCP does not react with the polymer.
- LDPE
- DCP
- Anti-oxidant
- Loss-in-weight feeding.
- Two-stage extruders suit this compounding better, because they hold the melt temperature.
- Cooling water for pelletizing must be clean, without positive or negative ions.
- Dryer and vacuum packing system.
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT65 | 62.4 | 400 | 132 | 56 | 400–500 |
| SAT75 | 71.4 | 400 | 220 | 56 | 700–800 |
| SAT95 | 93 | 400 | 315 | 56 | 900–1100 |
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT40 | 41 | 600 | 45 | 40 | 150 |
| Model | Diameter (mm) | Max. Speed (rpm) | L/D | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| SAT75-TDD180R | 71/180 | 400/93 | 48/8 | 132/75 | 400–450 |
| SAT95-TDD200R | 93/200 | 330/93 | 48/8 | 220/90 | 700–850 |
Semiconductive compounds: one machine for every type
Peroxide and silane semiconductors are compatible with the two XLPE types. All kinds of semiconductive compound can be produced on the same machine.
Basic formula
- PE / EVA
- Carbon powder
- DCP
- Anti-oxidant
- Kneader
- Conical force feeding
- Single screw
- Air-cooling die face
| Model | Kneader Volume (Liter) | Screw Diameter (mm) | Screw Speed (rpm) | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| K75-TDD150 | 75 | 150 | 60 | 110/75 | 350–450 |
| K110-TDD180 | 110 | 180 | 60 | 160/110 | 550–600 |
PVC cable compounds
Plasticised PVC is commonly used as insulation and sheathing on electrical cables.
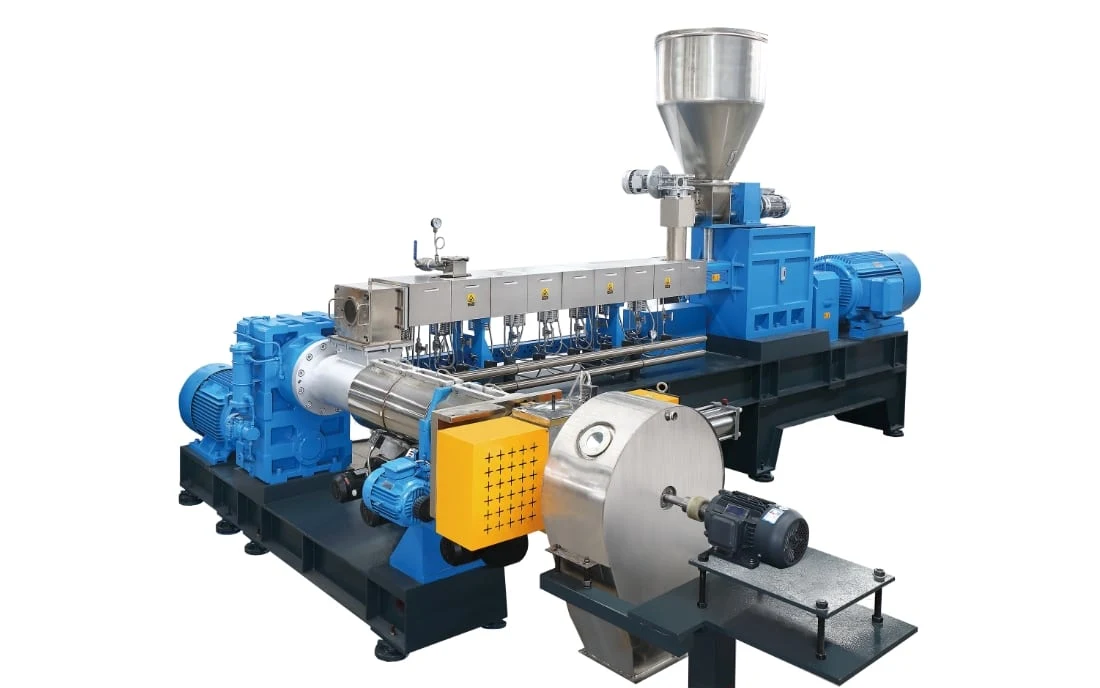
Tandem: twin screw to disperse, single screw to cool
The first stage is a co-rotating parallel twin screw extruder for dispersion and distribution; the second stage is a single screw extruder for cooling and pelletizing.
Basic formula
- PVC60%
- DOP20%
- Calcined clay10–20%
- CaCO₃0–10%
- Heat stabiliser
- Additives
| Model | Diameter (mm) | Max. Speed (rpm) | L/D | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| SAT52-TDD150R | 51.4/150 | 500/93 | 40/8 | 90/55 | 250–350 |
| SAT65-TDD180R | 62.4/180 | 500/93 | 40/8 | 132/75 | 500–600 |
| SAT75-TDD200R | 71/200 | 500/93 | 40/8 | 220/90 | 800–1200 |
| SAT95-TDD240R | 93/240 | 500/93 | 40/8 | 355/110 | 1700–2500 |
Halogen-free flame retardant (HFFR)
HFFR, low smoke zero halogen (LSZH) and low smoke and fume (LSF) are names for compounds used extensively in cable insulation. They are based on polyethylene or its co-polymers, with mineral fillers to make them flame retardant.
- PE10%
- EVA30%
- ATH powder55%
- Additives5%
| Model | Kneader Volume (Liter) | Screw Diameter (mm) | Screw Speed (rpm) | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| K75-SAT65-TDD180 | 75 | 62.4/180 | 500/75 | 110/110/75 | 400–500 |
| K110-SAT75-TDD200 | 110 | 71.4/200 | 500/75 | 160/200/90 | 700–800 |
| Model | Diameter (mm) | Max. Speed (rpm) | L/D | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| SAT-T52-TDD150R | 51.4/150 | 500/75 | 44/8 | 90/55 | 250–350 |
| SAT-T65-TDD180R | 62.4/180 | 500/75 | 44/8 | 132/75 | 500–600 |
| SAT-T75-TDD200R | 71.4/200 | 500/75 | 44/8 | 220/90 | 800–1000 |
Projects · XLPE
XLPE cable compounds on SAT95 with underwater pelletizing
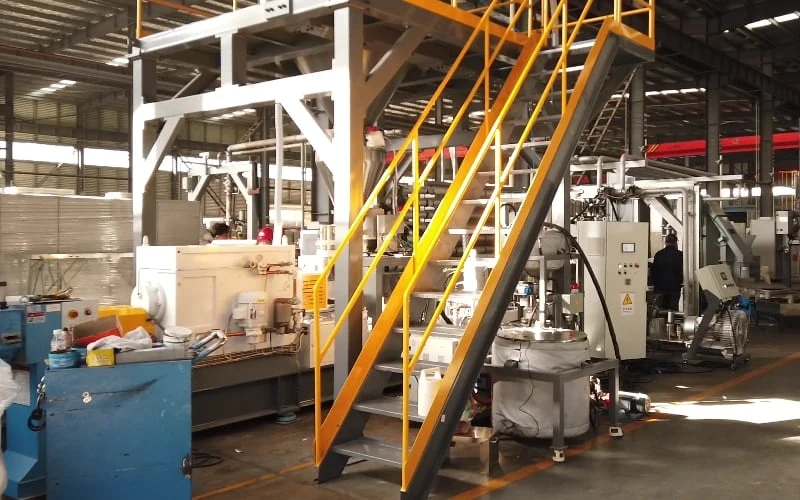
Two XLPE cable compound lines, one for 35 kV peroxide XLPE in China and one for a client in India. Both run a SAT95 twin screw extruder into an underwater pelletizing system.
- Extruder
- SAT95
- Output
- 800–1,500 kg/h
- Pelletizing
- Underwater
- Feeding
- Loss-in-weight
- Vacuum loader
- Buffer hopper
- Loss-in-weight
- Twin screw
- Filter
- Start-up valve
- Underwater pelletizing
- Dewater
- Classifier
- Fluidised bed
- Packing
Peroxide XLPE line for 35 kV cable 800 kg/h XLPE line, India
 India
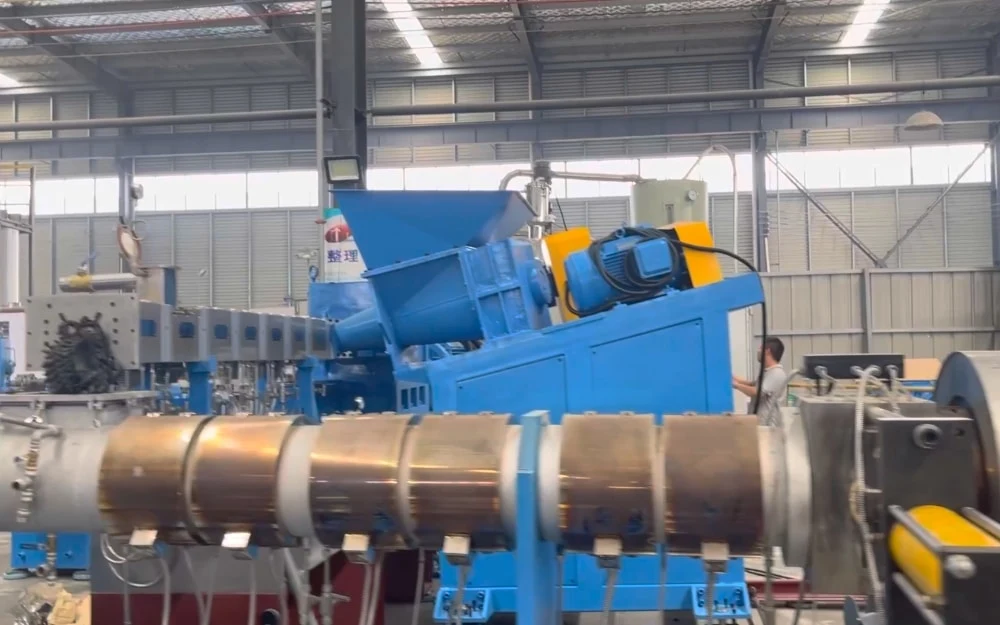 HFFR
 Solution
Get a quote
Tell us which cable compound you make — PE, silane or peroxide XLPE, semiconductive, PVC or HFFR — with its formula, filler loading and voltage class. We will propose the kneader or extruder stages, pelletizing and drying for that compound at your target output.
- 01Compound, formula & voltage class
- 02Machine stages & pelletizing
- 03Drying, packing & layout

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.