
Thermoplastic Elastomers (TPE)
TPEs, sometimes called thermoplastic rubbers (TPR), combine the properties of rubber with the processability of plastic. USEON builds compounding lines for TPV, TPR and SEBS compounds and TPU, with the long L/D, liquid injection and pelletizing these soft, oil-filled materials need.
- TPV
- TPS · TPR · SEBS
- TPU
- TPO · TPC · TPA
Six generic classes of commercial TPE
Most elastomers are thermosets. TPEs are copolymers or physical mixes of a plastic and a rubber, so they can be moulded like plastics.
TPSTPE-S
Styrenic block copolymers
Based on SBS or SEBS. Soft to the touch and easy to colour; the base of TPR shoe compounds and soft-touch overmoulding grades.
Typical usesShoe soles, tool grips, soft-touch overmoulding
TPOTPE-O
Thermoplastic polyolefin elastomers
Blends of PP with EPDM or POE rubber, without vulcanizing the rubber phase. Low density and good weathering resistance.
Typical usesBumpers, interior skins, roofing membranes
TPVTPE-V
Thermoplastic vulcanizates
PP and EPDM with the rubber phase dynamically vulcanized, for rubber-like resilience and heat resistance with thermoplastic processing.
Typical usesSeals, weatherstrips, hoses, metro pads
TPUTPU
Thermoplastic polyurethanes
Hard and soft polyurethane segments in one chain. High abrasion resistance and elasticity across a wide hardness range.
Typical usesCable jackets, films, footwear
80 kg/h TPU micro pellets, SAT40 1 t/h TPU / rubber lump pelletizing
TPCTPE-E
Thermoplastic copolyester
Hard polyester and soft polyether segments. Keeps its strength at high temperature and resists oil and flex fatigue.
Typical usesCVJ boots, hoses, cable jackets
TPATPE-A
Thermoplastic polyamides
Polyamide block copolymers (PEBA). Light, with high rebound and good flexibility at low temperature.
Typical usesSports shoe soles, medical tubing
Applications
Automotive
Wire & cable
Construction & transportation
Other industrial
TPV: one step or two?
TPV is made by vulcanizing rubber inside molten plastic. The rubber is sheared into micron-sized particles, a sea-island structure that gives the compound rubber's resilience and plastic's processability. Which route fits depends on the form of your EPDM and on your output.
EPDM in pellet form
Step 1: PP 20–30%, EPDM pellets 40–50%, CaCO₃ 10–20%, oil 0–15%, additives 2–10%
Step 1 · premix, blend, absorb oil
- Big twin screw
- Water ring
Step 2 · reacting compounding
- Premix
- Volumetric feeding
- Small twin screw · L/D 52
- Water ring or underwater
- One big extruder can supply several small extruders in step 2.
- Small extruder with less clearance is the key point of step 2.
- Special screw elements premix the liquid and polymer.
EPDM in block form
Step 1: EPDM block, CaCO₃ 10–20%, oil 0–30%, additives 2–10%
Step 1 · premix with CaCO₃, absorb all the oil
- Kneader
- Force feeding
- Single screw
- Pellets or crushed pieces
Step 2 · reacting compounding, with PP
- Loss-in-weight feeding
- Twin screw · L/D 52
- Water ring or underwater
- Long L/D and a high-torque gearbox give enough reaction time and dispersion.
- Loss-in-weight feeding is better for step 2.
Dynamic vulcanization in one pass
PP, EPDM, CaCO₃, oil and additives in one line; oil enters in stages along the barrel.
One line · react, disperse, pelletize
- Loss-in-weight main + side feeders
- Multi-port oil injection
- Twin screw · L/D 56
- Filter · diverter valve
- Underwater pelletizing
- Sectional injection prevents local over-lubrication and screw slippage.
- Sectional temperature control keeps the reaction window stable.
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT75 | 71.4 | 500 | 220 | 48 | 500–600 |
| SAT95 | 93 | 500 | 355 | 40 | 800–900 |
| Model | Kneader Volume (Liter) | Screw Diameter (mm) | Screw Speed (rpm) | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| K75-TDD180 | 75 | 180 | 75 | 110/90 | 300–400 |
| K110-TDD220 | 110 | 220 | 75 | 160/110 | 600–700 |
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT52 | 51.4 | 600 | 110 | 52 | 200–300 |
| SAT65 | 62.4 | 600 | 220 | 52 | 300–400 |
| SAT75 | 71.4 | 600 | 315 | 52 | 500–600 |
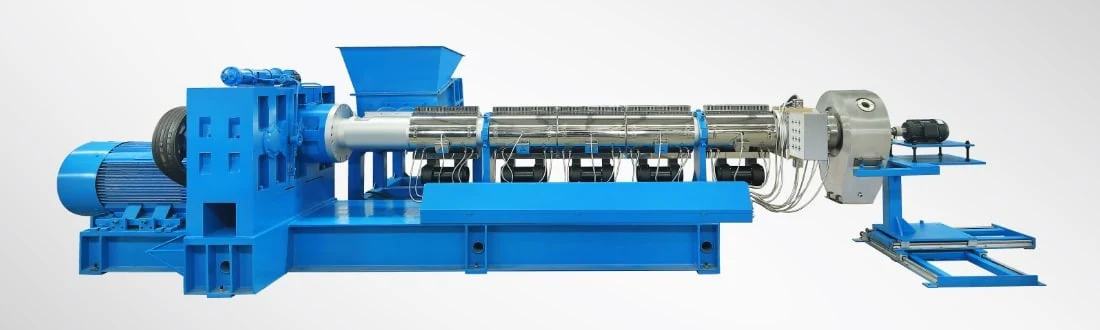
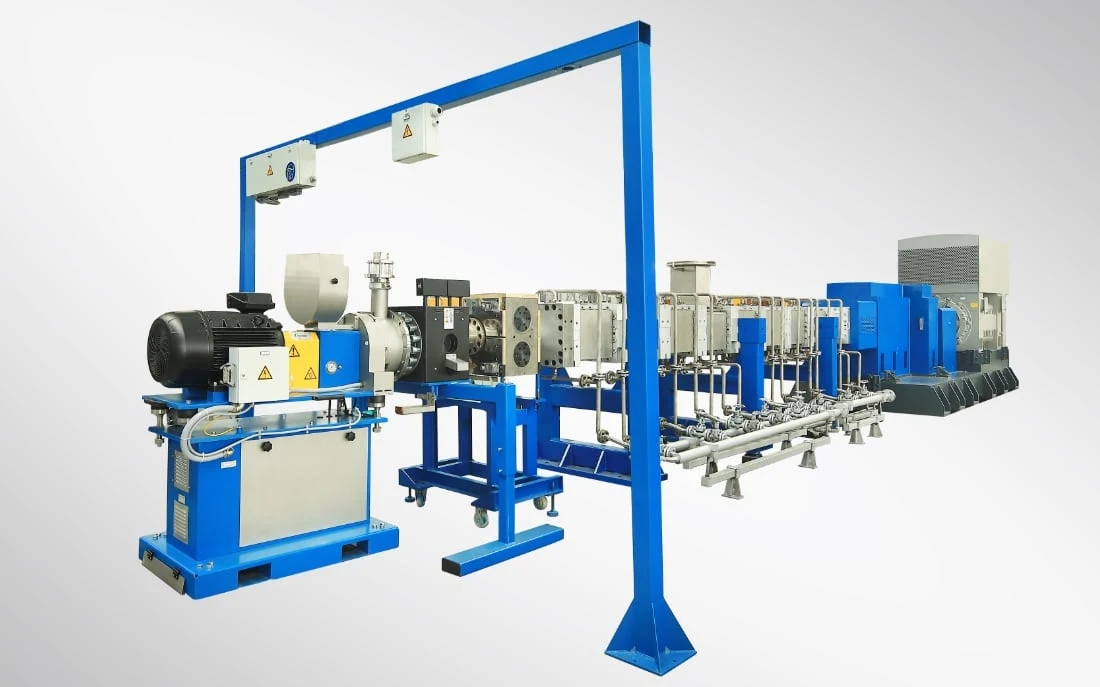
Inside a TPV reaction extruder
From our SAT75 TPV line: four engineering choices for the three hard parts of elastomer processing — the reaction, the feeding and the pelletizing.
Dynamic vulcanization control
Too little reaction time leaves vulcanization incomplete; too much shear lets the temperature run away.
L/D 56 + sectional temperature control
A residence-time window long enough for in-situ vulcanization and fine dispersion of the rubber phase.
High viscosity and torque load
Elastomer melt puts a high load on the main drive.
250 kW water-cooled PM motor + safety coupling
High torque at low speed, a cleaner motor without dust intake, and mechanical overload protection.
Oil injection and slippage
A large amount of liquid at one point makes the screws slip and the formula drift.
Multi-port injection at barrels 2, 3, 6, 7, 8
Oil is absorbed step by step; extrusion pressure stays stable.
Soft pellets stick
Strands of soft compound break, stick and leave tails.
UWP500 underwater pelletizing + uniform-temperature die plate
Cutting and cooling happen together; pellets come out rounder and do not agglomerate.
Water ring or underwater: set by hardness
The hardness of the final pellets decides the pelletizing. These are the choices made on our TPE lines.
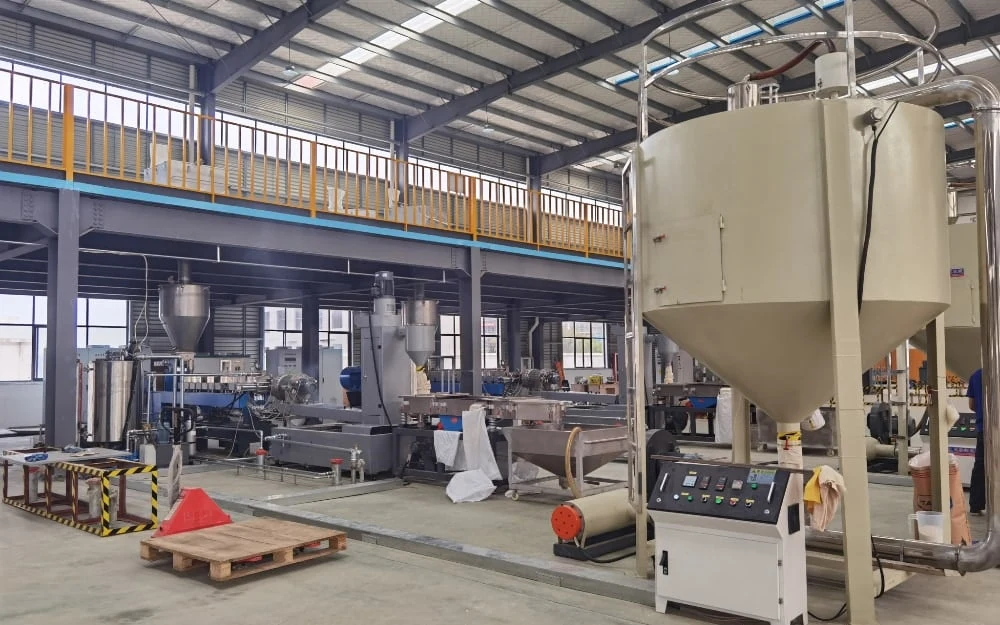
Harder compounds and step-1 pellets
A gentle cooling path for sticky elastomers that still hold their shape at the die face.
- TPV step 1, two step processSAT95 · 500–600 kg/h
- SEBS + EVA for shoe foams and soft-touch gripsSAT65 · L/D 48
- TPR shoe compoundsSAT65 / SAT75
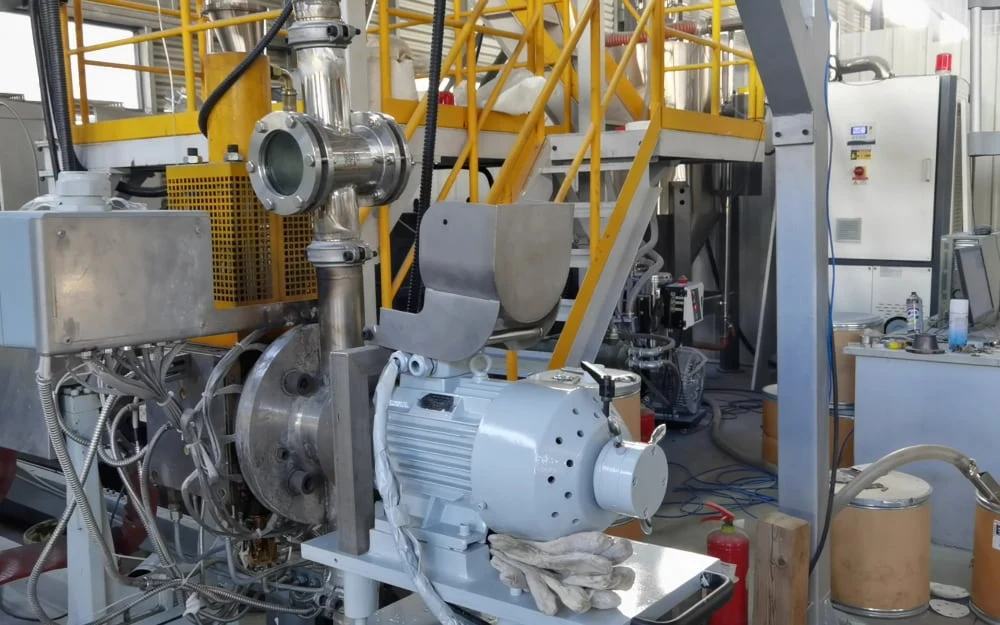
Soft, oil-filled and micro pellets
Cutting and cooling at the same moment, for low-hardness TPV and TPE that strand pelletizing cannot handle.
- TPV / TPE reaction extrusionSAT75 · UWP500
- TPE lines in Brazil, Poland, TurkeySAT65–SAT110
- TPU micro pellets, 0.8 mm holes × 1,200SAT40 · 80 kg/h
- TPU / rubber lump at 80 °CTDD220 · 1 t/h
PelletizingWater ring pelletizing system PelletizingUnderwater pelletizing system
TPR compounding for shoes
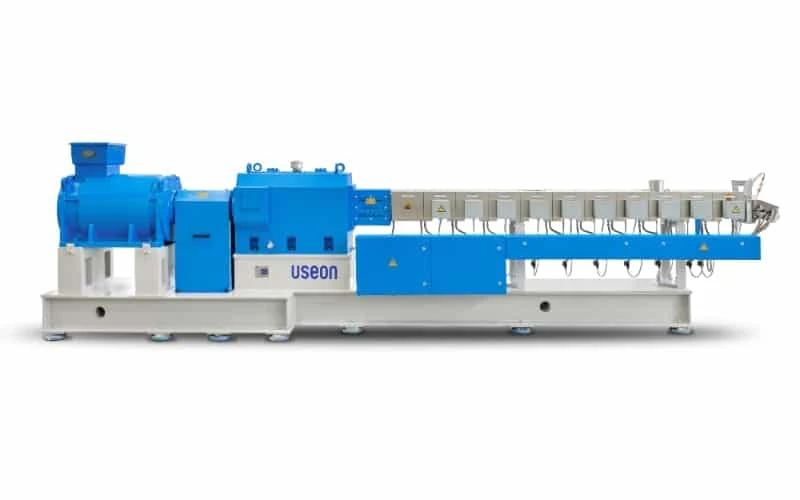
A twin screw instead of a kneader
Compared with the traditional kneader + single screw process, the twin screw extruder gives more output and better dispersion, and the colour is easy to change. Water ring pelletizing.
Basic formula
- HIPS / GPPS
- SBS
- Paraffin oil
- CaCO₃
- Silica
- EVA
- Stabiliser
- Additives
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT65 | 62.4 | 500 | 160 | 52 | 400–500 |
| SAT75 | 71.4 | 500 | 220 | 52 | 700–800 |
Project400 kg/h TPR compounding line, VietnamSAT65 Project1,500 kg/h TPE / TPR line, BrazilSAT110
Projects · TPV reaction extrusion
TPV and soft TPE on one SAT75 line
A thermoplastic elastomer maker needed one line for both conventional TPE compounding and TPV dynamic vulcanization, with very consistent physical properties. Its short-L/D equipment had given incomplete reaction and large fluctuations.
- Extruder
- SAT75 · L/D 56
- Output
- 250–500 kg/h
- Drive
- 250 kW PM
- Pelletizing
- UWP500
Main motor torque and die pressure stable across the target capacity range.
Rounder pellets; soft-material sticking effectively suppressed.
Interlock and one-key start / stop reduce manual steps and downtime from human error.
TPE lines delivered
Sorted by output.
| Line | Material | Output | Pelletizing |
|---|---|---|---|
| SAT110 · Brazil | TPE / TPR | 1,500 kg/h | Underwater |
| TDD220 single screwconical force feeder | TPU / rubber lump at 80 °C | 1,000 kg/h | Underwater |
| SAT95 · two step process | TPV | 500–600 kg/h | Water ring |
| SAT75 · Poland | TPE compounds | 500 kg/h | Underwater |
| SAT65 · Turkey | TPE | 500 kg/h | Underwater |
| SAT75 · L/D 56featured above | TPV dynamic vulcanization + TPE | 250–500 kg/h | Underwater UWP500 |
| SAT65 · Vietnam | TPR | 400 kg/h | — |
| SAT75 · China | TPV | 350 kg/h | Water ring |
| SAT65 | TPV | 250–300 kg/h | Underwater |
| SAT40filter · gear pump | TPU micro pellets | 80 kg/h | Underwater |
| SAT40 · one step process | TPV: PP, EPDM, CaCO₃, oil | 40–80 kg/h | Underwater |
| SAT65-48 · 160 kW · 600 rpm | SEBS + EVA | — | Water ring |
| U7 twin screwvideo in the hero | TPE | — | Underwater |
Get a quote
Tell us your TPE type, the form of your rubber (pellets or bales), the oil content and the hardness you need. We will advise one-step or two-step compounding, where the oil goes in along the barrel, and whether water ring or underwater pelletizing suits your pellets.
- 01Formula, rubber form & oil content
- 02One step or two & L/D
- 03Hardness & pelletizing

Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.