Additive Masterbatch
Any plastic product needs at least two types of additives to modify its physical or chemical properties, such as flame resistance, thermal stability or weather resistance. USEON provides pelletizing lines for all kinds of additive masterbatch, designed around your formulas and circumstances.
- Films & sheets
- Engineering plastics
- PET
- Rigid PVC
- Pipe coating
- SAT40 to SAT75 twin screw extruders
- 150–1,000kg/h
Which additive, in which polymer
Additive masterbatch is used in a wide variety of applications. Find your additive in the rows and your polymer family in the columns.
| Additive | Multilayer films & sheetsPO, PVC, PS, PA, PET, CPP, BOPP, BOPET, BOPA | Engineering plasticsSAN, ABS, PET, PBT, POM, PMMA, PA6, PA66, PC | PETAPET, PETG, CPET, RPET | Rigid PVCProfiles, sills, panels, sidings, gutters, pipes | 3-layer PE coatingSteel pipes |
|---|---|---|---|---|---|
| Stabilisers | |||||
| Anti-oxidant | Yes, Multilayer films & sheets | Yes, Engineering plastics | Yes, PET | Yes, Rigid PVC | Yes, 3-layer PE coating |
| UV stabilisers & absorbers | Yes, Multilayer films & sheets | Yes, Engineering plastics | Yes, PET | Yes, Rigid PVC | Yes, 3-layer PE coating |
| Chain extender | No | No | Yes, PET | No | No |
| Surface & handling | |||||
| Slip | Yes, Multilayer films & sheets | No | No | No | No |
| Anti-slip | Yes, Multilayer films & sheets | No | No | No | No |
| Anti-block | Yes, Multilayer films & sheets | No | Yes, PET | No | No |
| Anti-static | Yes, Multilayer films & sheets | Yes, Engineering plastics | No | No | No |
| Anti-fog | Yes, Multilayer films & sheets | No | No | No | No |
| Anti-scratch | No | No | Yes, PET | No | No |
| Mould release | No | Yes, Engineering plastics | Yes, PET | Yes, Rigid PVC | No |
| Processing | |||||
| Processing aid | Yes, Multilayer films & sheets | Yes, Engineering plastics | Yes, PET | No | No |
| PIB | Yes, Multilayer films & sheets | No | No | No | No |
| Barrier & absorbers | |||||
| Gas barriers | Yes, Multilayer films & sheets | No | Yes, PET | No | No |
| Gas absorbers | Yes, Multilayer films & sheets | No | No | No | No |
| IR absorbers | Yes, Multilayer films & sheets | No | Yes, PET | No | No |
| Function & appearance | |||||
| Flame retardant | No | Yes, Engineering plastics | No | No | No |
| Laser marking | No | Yes, Engineering plastics | No | No | No |
| Optical brightener | Yes, Multilayer films & sheets | No | Yes, PET | No | No |
| Anti-root | Yes, Multilayer films & sheets | No | No | No | No |
| Anti-rodent | Yes, Multilayer films & sheets | No | No | No | No |
| Biodegradable additives | Yes, Multilayer films & sheets | No | No | No | No |
| Adhesion | |||||
| Adhesive | No | No | No | No | Yes, 3-layer PE coating |
| Maleic anhydride (MAH) grafting | No | No | No | No | Yes, 3-layer PE coating |
| Functions listed | 16 | 7 | 10 | 3 | 4 |
Engineering plastics include all reinforced and modified polymers used in injection and extrusion. PET grades cover injection moulding, extrusion and thermoforming. MAH grafting is also a compounding process of its own: Grafting compounding →
Processing of additive masterbatch
Two facts shape an additive masterbatch line.
Output depends on feeding, not torque
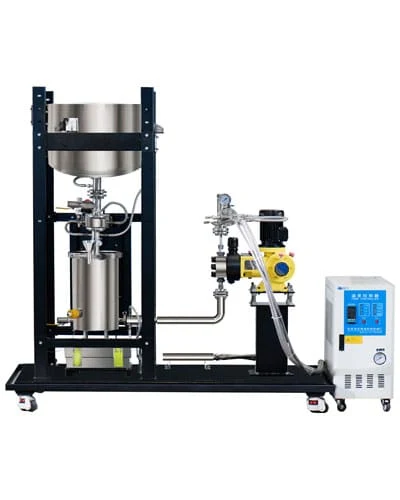
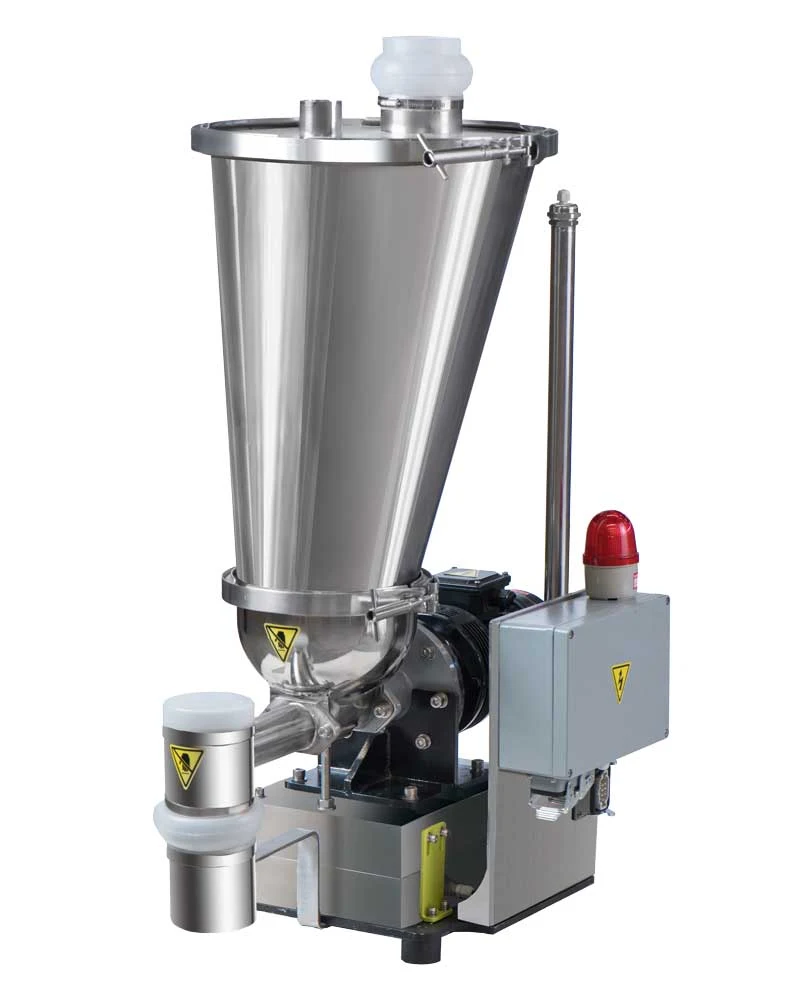
The bulk density of additives is relatively low, so the output depends mostly on the feeding capacity, not on the torque of the main motor.
One extruder, many formulas
One extruder should be able to make many types of additive masterbatch, so it needs a fast-cleaning strand die plate for formula changes.
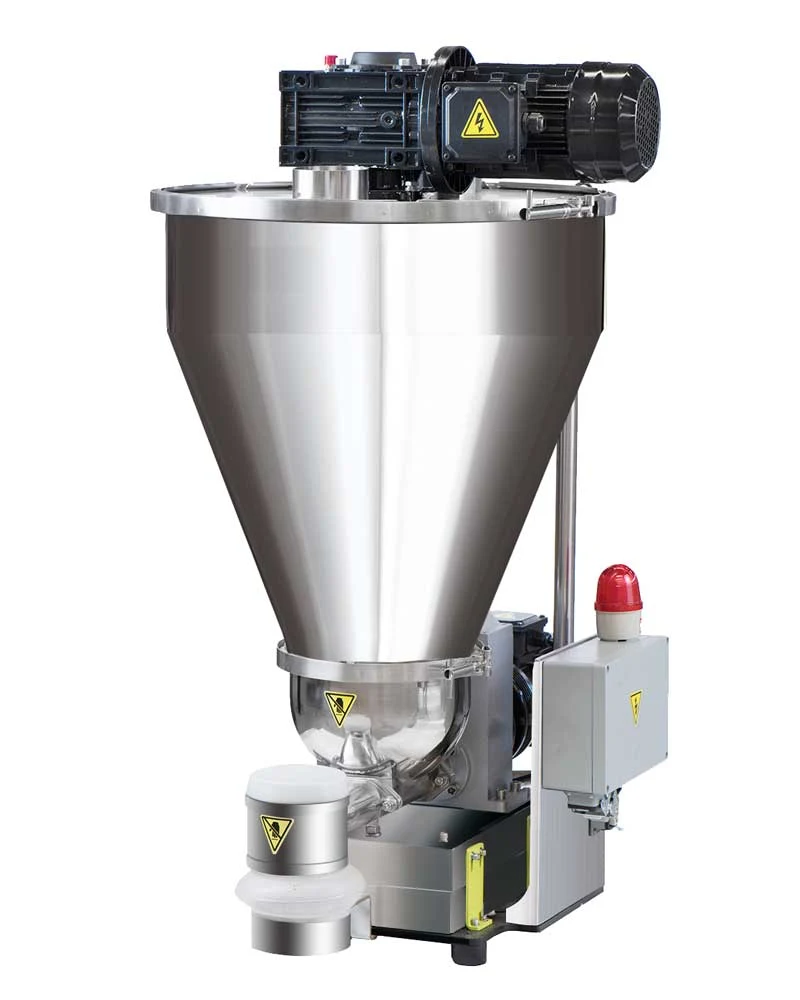
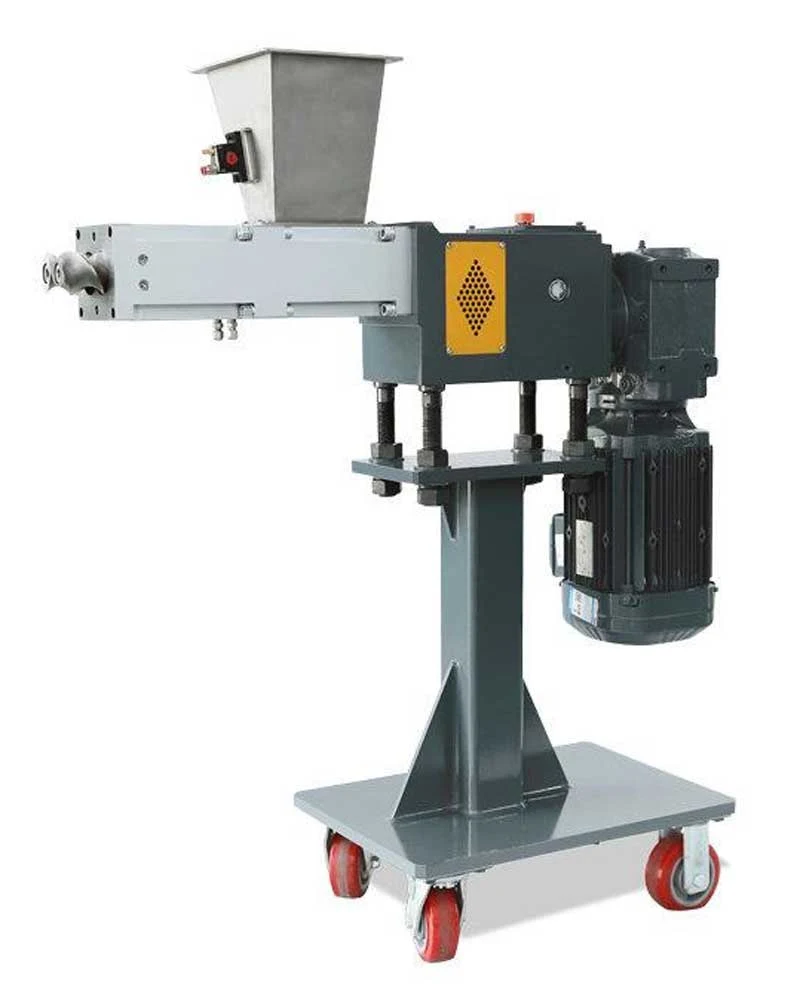
Technical specifications of the extruder
Because output follows feeding capacity, our SAT twin screw extruder suits this process.
| Model | Diameter (mm) | Max. Speed (rpm) | Motor (kW) | L/D | Output (kg/h) |
|---|---|---|---|---|---|
| SAT40 | 41 | 600 | 45 | 40 | 150–200 |
| SAT52 | 51.4 | 600 | 90 | 40 | 200–300 |
| SAT65 | 62.4 | 600 | 160 | 40 | 400–500 |
| SAT75 | 71.4 | 600 | 250 | 40 | 800–1000 |
Machine page: Co-rotating Twin Screw Extruder
Projects · additive masterbatch
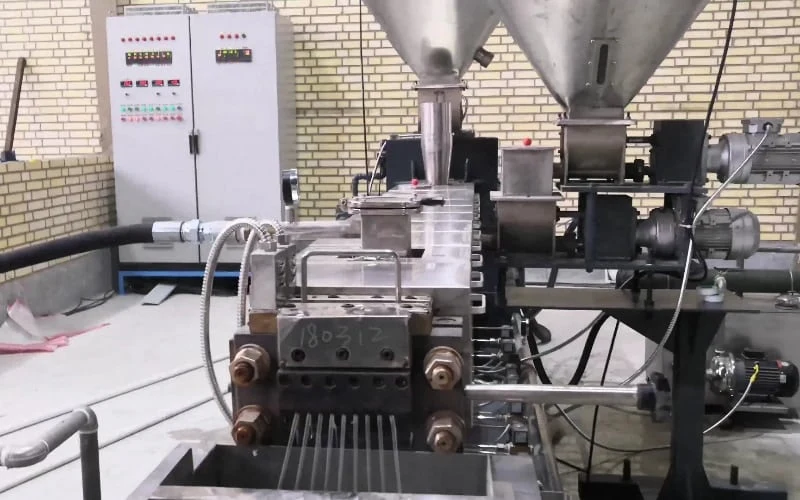
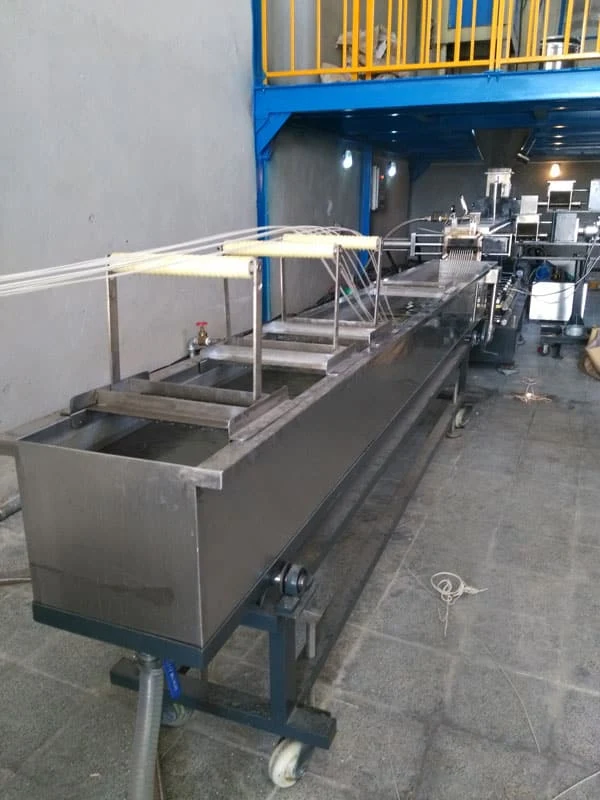
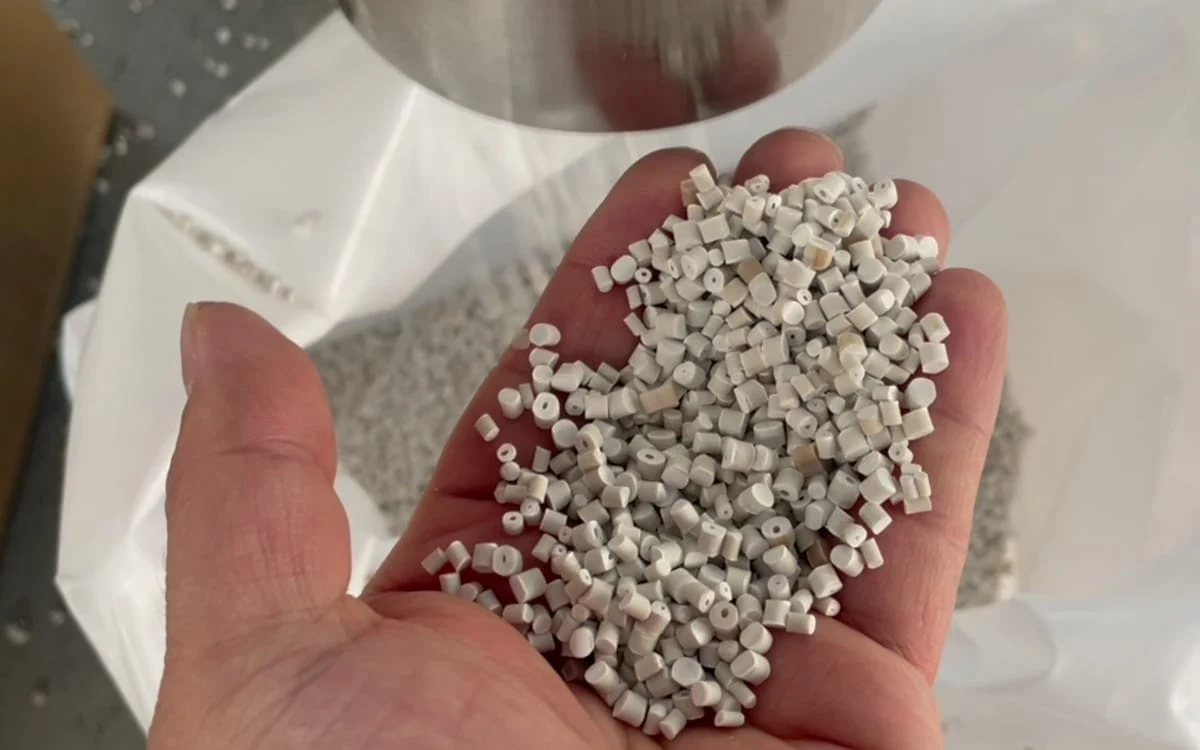
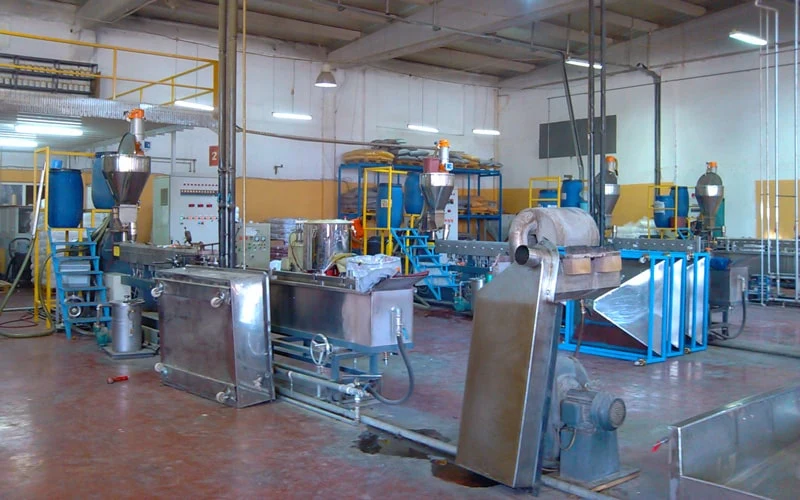
SAN anti-aging masterbatch on a SAT65
Anti-aging masterbatch for SAN, an engineering plastic, compounded on a SAT65 twin screw extruder with water-cooling strand pelletizing.
- Extruder
- SAT65
- Output
- 200–400 kg/h
- Pelletizing
- Water-cooling strand
- Base
- SAN
Read the SAN project 250 kg/h line in the Middle East, SAT52
 Middle East
 Compounding
 Compounding
Get a quote
Tell us the additives you compound, their form (liquid, pellet or powder), the carrier resin and how often your formula changes. We size the feeding first, because that is what sets the output.
- 01Additives, forms & carrier
- 02Feeding layout & extruder
- 03Formula changes & cleaning
Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.