PVC Compounding
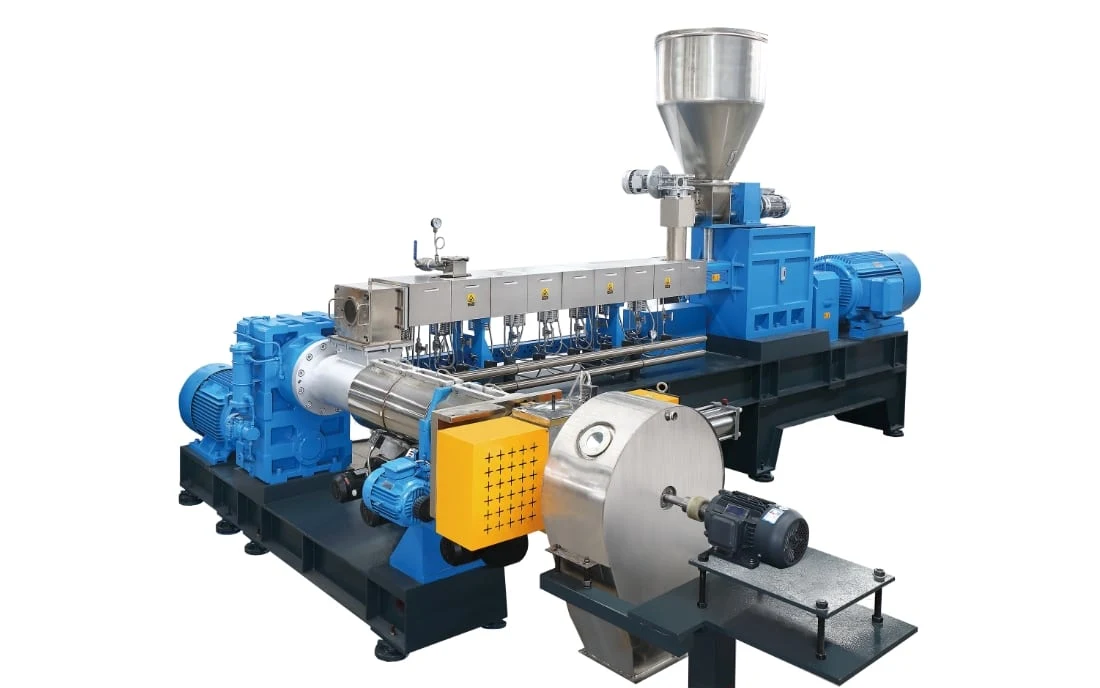
PVC is durable, cheap and easily worked, but before it becomes a product it must be compounded with additives — and it degrades easily at high temperature. Our tandem compounder, a twin screw followed by a cooling single screw, is designed for exactly that.
- Rigid · pipe fittings & profiles
- Soft · cable & medical
- Profile recycling
Disperse hot, then cool down
PVC degrades very easily above 170 °C. A twin screw alone gives the dispersion and output but holds a high melt temperature, so a second, slow single screw takes the melt down before pelletizing.
Twin screw: dispersion
Modular screws and barrels; change the screw sequence easily for different formulae. High screw speed gives better dispersion and more output.
- Speed
- 300–500 rpm
- L/D
- 40
Single screw: cooling
Cools the melt from the twin screw and extrudes it for pelletizing.
- Speed
- 93 rpm
- L/D
- 8
- Rigid PVC
Air-cooling die face, eccentric
No filter; strong cooling on the single screw. Pipe fittings and profiles.
- Soft PVC
Water ring
Filter before the die; dewatering and fluidised bed after. Medical compounds.
- Profile recycling
No pellets
Cool on a conveyor, then crush into powder.
What goes into a PVC compound
Before PVC can be made into finished products, it is converted into a compound with additives — not necessarily all of these.
Additives
Then formed by
GuidePolyvinyl chloride (PVC): properties, uses and processing
Four applications we know well
Experience from our PVC compounding lines.
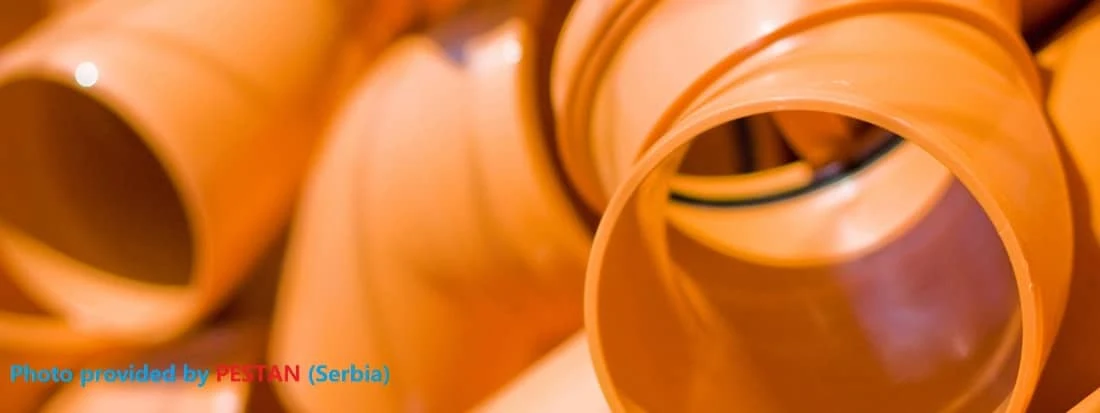
a · Rigid PVC
Pipe fittings and connections
- For injection-moulded fittings, compound pellets work better than premix powder: you can add more CaCO₃, and premix powder gives poorer dispersion and shape quality.
- No filter; an eccentric pelletizer.
- Strong cooling on the single screw extruder.
Basic formula
- PVC
- CaCO₃5–15%
- Heat stabiliser
- Impact modifier
- Lubricant wax
- Colour pigment
Project900 kg/h rigid PVC, SerbiaSAT75–TDD200 Project500 kg/h rigid PVC, ChinaSAT65–TDD180 ProjectRigid PVC two-stage lineSAT65–TDD180
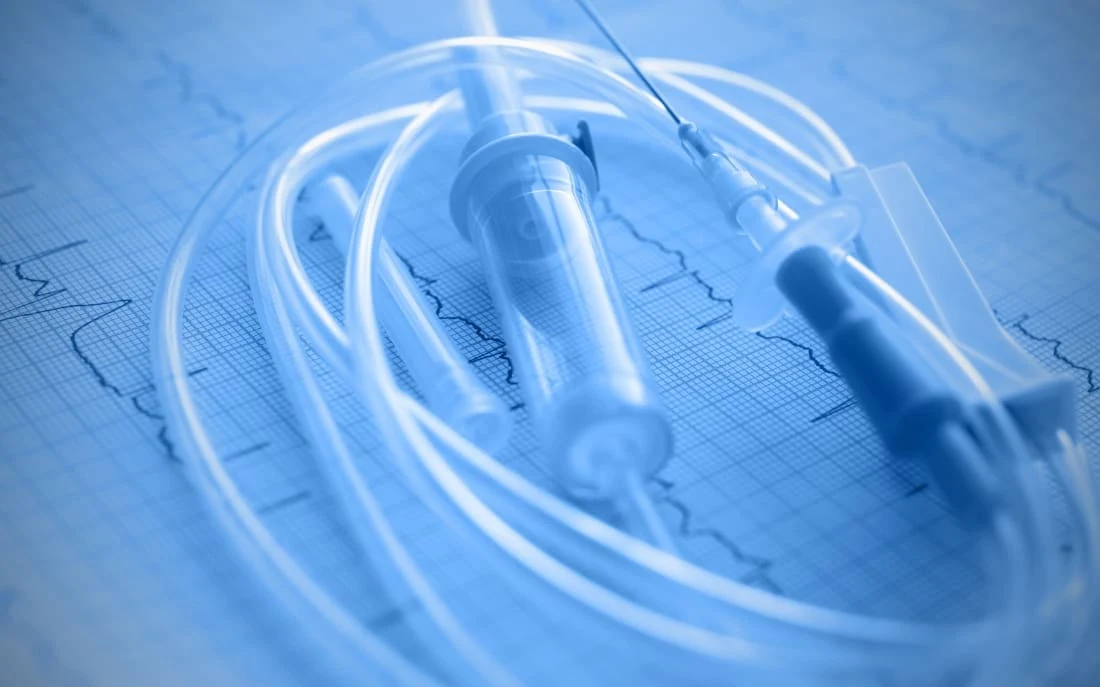
b · Soft PVC
Medical grade transparent compound
The medical industry demands only the best quality PVC: flanges for Copper-T, disposable tubes, IV tubes, oxygen masks, regulators, urine bags, blood bags and glucose bags.
Process on our 2,000 kg/h medical line
- Two-stage mixer
- Feeding
- Twin screw
- Single screw
- Filter
- Water ring
- Dewater
- Classifier
- Fluidised bed
- Storing
Project2,000 kg/h soft PVC for medical applicationSAT95–TDD220
c · Soft PVC
Cable insulation and sheathing
Plasticised PVC is commonly used as insulation and sheathing on electrical cables.
Basic formula
- PVC60%
- DOP20%
- Calcined clay10–20%
- CaCO₃0–10%
- Heat stabiliser
- Additives
d · Recycling
Window profile scrap back into profile
- Premix scrap + virgin powder + impact modifier + pigment + stabiliser
- First barrel
- Side feeder: wood fibre or CaCO₃
- Conveyor cooling
- Crush to powder
Basic formula
- PVC scrap40%
- Virgin PVC powder10%
- Wood fibre20%
- CaCO₃20%
- Additives
Tandem compounder models
Twin screw / single screw values are given as stage 1 / stage 2.
| Model | Diameter (mm) | Max. Speed (rpm) | L/D | Motor (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| SAT52-TDD150R | 51.4/150 | 500/93 | 40/8 | 90/55 | 250–350 |
| SAT65-TDD180R | 62.4/180 | 500/93 | 40/8 | 132/75 | 500–600 |
| SAT75-TDD200R | 71/200 | 500/93 | 40/8 | 220/90 | 800–1200 |
| SAT95-TDD240R | 93/240 | 500/93 | 40/8 | 355/110 | 1700–2500 |
Machine page: Tandem Extrusion System
Projects · rigid PVC
Rigid PVC for profiles, from jumbo bag to silo
A SAT95-TDD220 tandem compounding extruder for rigid PVC profile compound, with automatic loss-in-weight feeding and air-cooling pelletizing.
- Extruder
- SAT95-TDD220
- Output
- 1,200–1,500 kg/h
- Pelletizing
- Air cooling
- Feeding
- Loss-in-weight
- Jumbo bag unloading
- Vacuum loader
- Loss-in-weight
- Twin screw
- Single screw
- Air-cooling pelletizing
- Conveying & cooling
- Classifier
- Storing
PVC lines delivered
Sorted by output.
| Line | Compound | Output | Pelletizing |
|---|---|---|---|
| SAT95-TDD220two-stage mixer · filter | Soft PVC, medical | 2,000 kg/h | Water ring |
| SAT95-TDD220featured above | Rigid PVC for profile | 1,200–1,500 kg/h | Air cooling |
| SAT75–TDD200 · Serbia | Rigid PVC | 900 kg/h | — |
| SAT65-TDD180 · China | Rigid PVC | > 500 kg/h | — |
| SAT65-TDD180 | Rigid PVC | 300 kg/h | Air-cooling die face |
Tell us whether you compound rigid or soft PVC, your formula (plasticiser and filler content) and the end product — fittings, profiles, cable or medical. We will size both stages of the tandem line and the pelletizing for your target output.
- 01Rigid or soft, formula & end product
- 02Twin screw and cooling single screw
- 03Pelletizing, cooling & storing
Souder Chen
Head of Compounding Division
With USEON since 2008. Twin screw compounding, devolatilization and recycling lines.